Use a shaped soft support that restrains the part outside finished and load-critical areas; never hold a tiny workpiece in the fingertips beside a rotating accessory. Test the exact material and geometry on a representative sample before production. Control workholding, accessory fit, debris and heat, and stop at the first sign of damage.
clamp small 3D prints for rotary finishing
clamp small 3D prints for rotary finishing is the controlled selection of a rotary, hand or alternative finishing method for stabilizing a miniature, bracket, insert or thin printed component for local finishing, with the work material, protected geometry and pass/fail condition defined before removal begins.
Use a shaped soft support that restrains the part outside finished and load-critical areas; never hold a tiny workpiece in the fingertips beside a rotating accessory. Test the exact material and geometry on a representative sample before production. Control workholding, accessory fit, debris and heat, and stop at the first sign of damage. This guide treats stabilizing a miniature, bracket, insert or thin printed component for local finishing as a controlled process. It separates what can be verified on the current workpiece from what must be confirmed through the material supplier, a drawing, a mating part or a retained finish sample.
The working material is printed polymer that may crush, spring out or transmit vibration when clamped incorrectly. That description matters because a method that looks acceptable on one polymer, resin, coating or accessory combination can produce heat, tearing, dust, loss of geometry or contamination on another. Work from a disposable coupon whenever the material or finish is unfamiliar.
How should a small printed part be held while using a rotary tool?
Use a shaped soft support that restrains the part outside finished and load-critical areas; never hold a tiny workpiece in the fingertips beside a rotating accessory. Begin by protecting surfaces that should not be touched, then identify one visible stop condition. The operator should be able to explain why material is being removed, which direction the tool will move and how the result will be checked before the accessory contacts the part.
No universal speed follows from clamp small 3D prints for rotary finishing. For printed polymer that may crush, spring out or transmit vibration when clamped incorrectly, accessory diameter, pressure and dwell change surface speed, heat and the failure described by part movement, jaw marks, flexing, blocked visibility or a tool path aimed at the hand means the setup must be changed. Use the tool maker’s instructions, accessory rating and material information, then qualify clamping force, jaw material, part orientation, access path, tool reaction, no-touch zones and visibility on a coupon. A structural, safety-critical or poorly measurable feature requires an approved process or a replacement part.
Why does this job fail?
part movement, jaw marks, flexing, blocked visibility or a tool path aimed at the hand means the setup must be changed. These signs are useful because they appear before the operator can correct the result with more pressure. Stop, clean the area and decide whether the problem is accessory condition, workholding, tool alignment, material response or an incorrectly defined task.
A buyer considering clamp small 3D prints for rotary finishing should not describe the kit only by speed and accessory count. The useful brief names stabilizing a miniature, bracket, insert or thin printed component for local finishing, the exact defect, protected geometry and this pass condition: the part stays fixed through the trial pass and leaves the fixture without distortion or surface damage That evidence lets a distributor or manufacturer propose a configuration for the stated material without implying one accessory works on every printed or molded surface.
Which variables control the result?
Control clamping force, jaw material, part orientation, access path, tool reaction, no-touch zones and visibility. Change one variable at a time during the first-piece trial. Keep the accessory clean, seat the shank correctly, support the work and use direct light. If the result depends on a particular pad, compound, cutter or abrasive, record its identity and replacement condition instead of calling it a generic rotary bit.
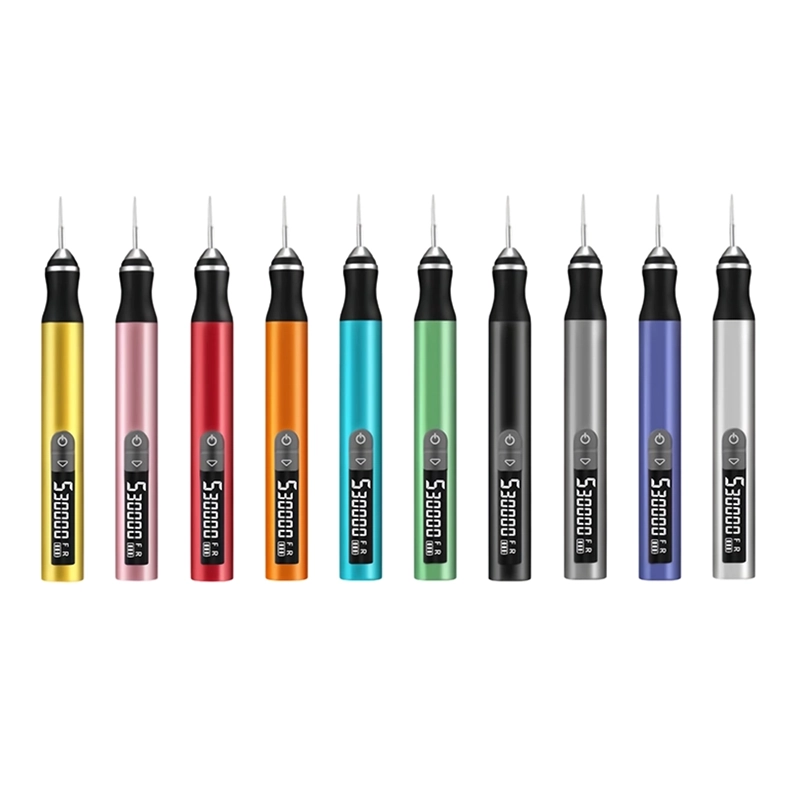
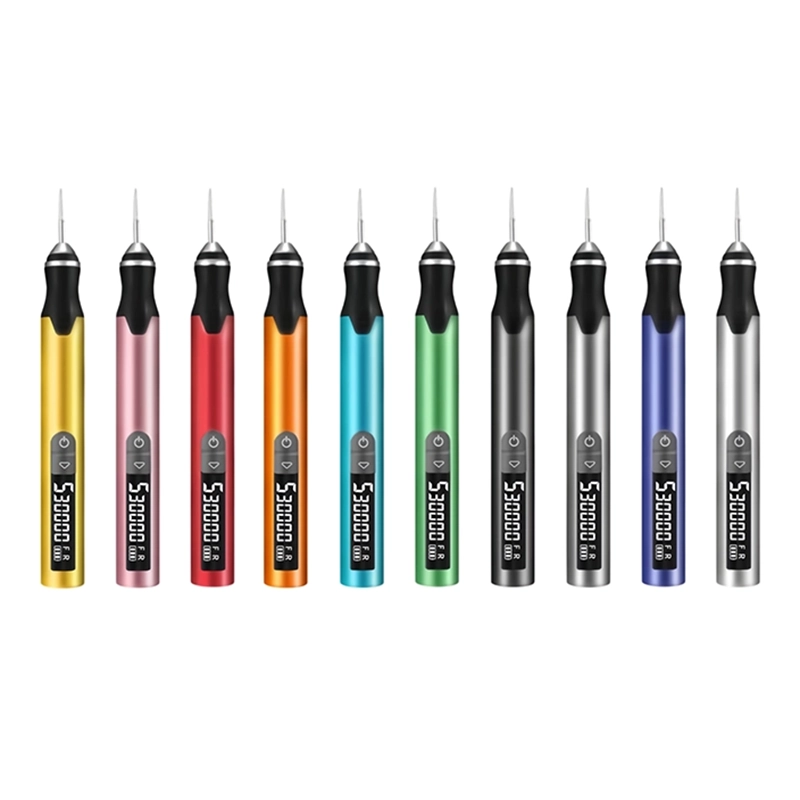
The current H101 five-speed cordless engraving pen is the real XOENAEN platform reference for clamp small 3D prints for rotary finishing, not a validated finishing recipe. Qualify the final accessory, setting and contact method on printed polymer that may crush, spring out or transmit vibration when clamped incorrectly, using the part stays fixed through the trial pass and leaves the fixture without distortion or surface damage as the acceptance evidence. Keeping the article-specific material and geometry beside the catalogue record prevents a platform specification from becoming an unsupported performance promise.
How should the work be prepared?
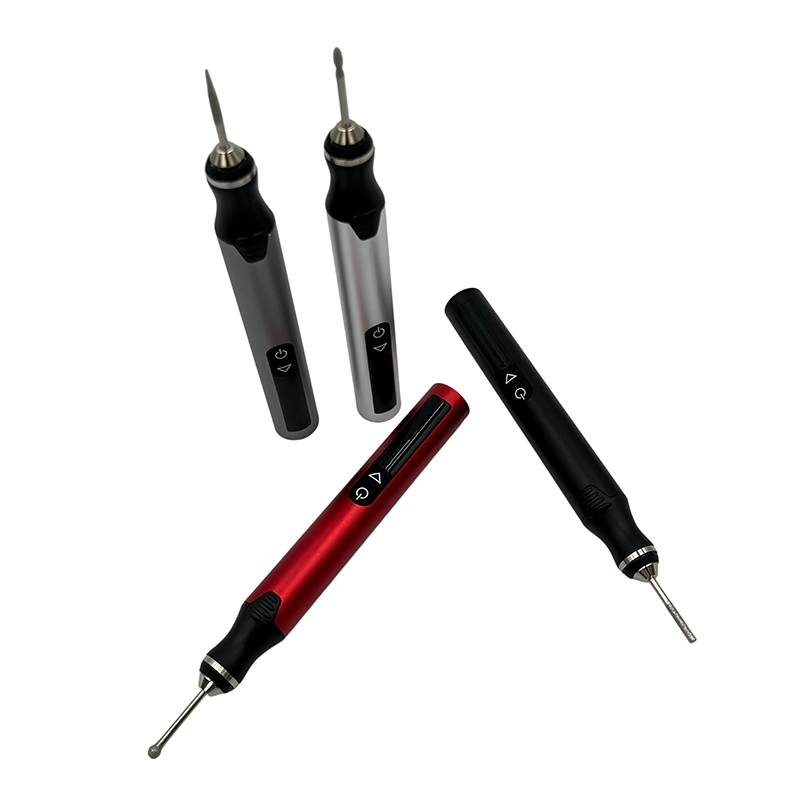
mark protected surfaces, add sacrificial supports, test clamp pressure on a rejected part, orient the tool away from the body and confirm a clear stop path. Photograph the starting condition and preserve one acceptable reference. Keep removed debris and used media away from clean parts. If several pieces are processed, approve the first piece and recheck after any accessory change, charging interruption or unexplained change in cut or sound.
The work record for clamp small 3D prints for rotary finishing should identify the part, printed polymer that may crush, spring out or transmit vibration when clamped incorrectly, accessory, workholding and this sequence: mark protected surfaces, add sacrificial supports, test clamp pressure on a rejected part, orient the tool away from the body and confirm a clear stop path It only needs enough detail for another trained person to reproduce the decision and verify the part stays fixed through the trial pass and leaves the fixture without distortion or surface damage, without guessing what broad terms such as “light pressure” or “smooth finish” meant on this geometry.
What should be compared before choosing a method?
Soft shaped jaws suits repeat small geometry, but its main limitation is fixture preparation. Sacrificial carrier is useful for very thin or delicate part, with extra print step as the risk to control. Hand-held part may be the right choice for avoid near rotating tool when the team accepts loss of control.
Compare the listed methods for clamp small 3D prints for rotary finishing on the same workpiece and against the part stays fixed through the trial pass and leaves the fixture without distortion or surface damage. Time is only one result; also record the changes most relevant to clamping force, jaw material, part orientation, access path, tool reaction, no-touch zones and visibility, including fit, edge condition, heat, debris, access, consumable wear and rework. A slower method can be the lower-cost choice when it preserves the protected feature in stabilizing a miniature, bracket, insert or thin printed component for local finishing.
How do you know when to stop?
the part stays fixed through the trial pass and leaves the fixture without distortion or surface damage. Inspect after cleaning and cooling, because dust, compound and temporary heat gloss can hide the actual surface. Use the mating part, gauge, fixed light or retained sample named in the work instruction. Do not accept the result only because the operator can no longer see the original mark.
For clamp small 3D prints for rotary finishing, stop and quarantine the part when part movement, jaw marks, flexing, blocked visibility or a tool path aimed at the hand means the setup must be changed. Do not use cosmetic finishing to hide a print, material or assembly defect that should be corrected upstream. The disposition should reference printed polymer that may crush, spring out or transmit vibration when clamped incorrectly and the affected feature so a reprint, alternate method or engineering review addresses the cause rather than only the visible mark.
What should a buyer put in the project brief?
include workholding assumptions and a sample fixture when qualifying a finishing workflow. Add target market, expected quantity, required accessory map, storage layout, manual language, packaging and sample timing. If the application creates dust, flying debris, heat or a battery-charging duty cycle, the intended workplace and user controls belong in the brief as well.
For an OEM or wholesale clamp small 3D prints for rotary finishing program, approve the complete pack-out against this buyer action: include workholding assumptions and a sample fixture when qualifying a finishing workflow Check accessory identity, collet compatibility, labels, replacement items and the limits linked to stabilizing a miniature, bracket, insert or thin printed component for local finishing. The product page can state platform facts, while the retained sample must show that the selected configuration answers this specific customer question.
Final recommendation
Use clamp small 3D prints for rotary finishing as a defined job, not a broad marketing claim. Start with a representative sample, control one variable at a time and keep a visible stopping rule. When the method passes, record the configuration and connect the tool, manufacturing review, OEM brief and inquiry path so the next buyer receives the same technical context.
Method comparison for stabilizing a miniature, bracket, insert or thin printed component for local finishing
| Method | Best fit | Main control |
|---|---|---|
| Soft shaped jaws | Repeat small geometry | Fixture preparation |
| Sacrificial carrier | Very thin or delicate part | Extra print step |
| Hand-held part | Avoid near rotating tool | Loss of control |
- Name the material and the exact application: stabilizing a miniature, bracket, insert or thin printed component for local finishing.
- Control clamping force, jaw material, part orientation, access path, tool reaction, no-touch zones and visibility.
- Use a representative coupon, fixture or mating part before approving the method.
- Stop when part movement appears.
- Accept only when the part stays fixed through the trial pass and leaves the fixture without distortion or surface damage.
- Confirm accessory identity, collet fit, labels, replacement media, manual language and packaging.
- View the H101 five-speed cordless engraving pen →
- Define an OEM / ODM tool configuration →
- Review manufacturing and quality controls →
- Read the related guide: organize-rotary-accessories-shared-maker-lab →
- Read the related post-process-carbon-fiber-filament-parts guide →
- Read the related clean-resin-print-drainage-holes guide →
- Continue with the clean-heat-set-insert-bores-3d-prints topic →
- XOENAEN editorial policy →
How should a small printed part be held while using a rotary tool?
Use a shaped soft support that restrains the part outside finished and load-critical areas; never hold a tiny workpiece in the fingertips beside a rotating accessory. Test the exact material and geometry first, then document the accessory, workholding and stop condition before treating the method as repeatable.
What technical factors matter for clamp small 3D prints for rotary finishing?
Control clamping force, jaw material, part orientation, access path, tool reaction, no-touch zones and visibility. These variables determine whether the process cuts cleanly, creates heat, changes geometry or leaves a finish that passes the real inspection.
Should the first clamp small 3D prints for rotary finishing trial use a final customer part?
No. Start with a representative sample of printed polymer that may crush, spring out or transmit vibration when clamped incorrectly and reproduce stabilizing a miniature, bracket, insert or thin printed component for local finishing. Move to a saleable part only after clamping force, jaw material, part orientation, access path, tool reaction, no-touch zones and visibility and the stopping rule are documented.
When should clamp small 3D prints for rotary finishing switch to a hand or guided method?
Switch when powered contact cannot control the failure described by part movement, jaw marks, flexing, blocked visibility or a tool path aimed at the hand means the setup must be changed. Sacrificial carrier is the comparison method for very thin or delicate part, subject to its limitation: extra print step.
What should an OEM buyer include for clamp small 3D prints for rotary finishing?
Include the target market, printed polymer that may crush, spring out or transmit vibration when clamped incorrectly, application, quantity, photographs or samples, accessory map, packaging and the acceptance evidence. include workholding assumptions and a sample fixture when qualifying a finishing workflow.
How should the result of clamp small 3D prints for rotary finishing be verified?
the part stays fixed through the trial pass and leaves the fixture without distortion or surface damage. Clean and cool the part first, then use the same light, gauge, mating component or retained reference used for the article-specific sample approval.