
Manufacturing / quality
Controlled from part to final shipment.
An integrated production chain, scalable assembly capacity and a full inspection system for stable global supply.
 QUALITY VERIFICATION / PRODUCT 67-IN-1
TORQUE / FIT / FINISH
* Company-supplied capability statement. Available capacity, production schedule and order-specific test scope are confirmed in the quotation.
Core processes under coordinated control.
In-house capability reduces outsourcing delays, supports flexible order scheduling and strengthens consistency from batch to batch.
What is screwdriver bit runout and why does it matter?
Runout is radial movement observed or measured at a defined point on the installed bit while the system rotates. It can come from bit straightness, debris, seating, holder geometry, shaft or bearings. A useful check fixes the bit, seating method, speed and observation distance, then uses reference-bit substitution to isolate the source. There is no universal public limit for every bit length and application.
Buyer takeaway: approve runout as an installed-system result under one written method. See the electric screwdriver runout test guide for the complete isolation sequence.
Evidence type: Technical method; no numeric XOENAEN runout result is claimed here.Full-process quality control
What quality checks should an electric screwdriver pass?
An electric screwdriver quality control plan should begin with the exact model, revision, approved sample and order specification. Depending on the agreed scope, checks can cover component identity, assembly parameters, direction, speed, torque, charging, battery behavior, noise, installed-bit runout, bit fit, appearance, accessories, labels and packaging. The written method, sampling plan and acceptance limits—not the name of a process stage—define pass or fail.
Buyer takeaways: request the checkpoint owner, sample rule, instrument or fixture, recorded result, deviation route and change trigger. Compare the production unit with the approved sample method and read the public evidence boundary before treating a capability statement as a completed test record.
Evidence type: Technical quality-planning guidance; order-specific records require project confirmation.- IQC
Incoming quality control
The order plan can identify motors, batteries, PCBs, bits, plastic and metal parts whose identity, dimensions or condition must be checked before assembly.
- IPQC
In-process quality control
Defined assembly parameters, configuration identity and recorded process checks should remain tied to the approved product revision.
- FQC
Final quality control
Applicable function, appearance, pack-out, labels and quantity checks should follow the agreed method and sampling plan before release.
How does a factory test electric screwdriver torque?
An electric screwdriver torque testing method should identify the exact model and revision, operating mode, battery condition, installed bit, fixture or reference joint, suitable measurement instrument, calibration or verification status, cycle count, sampling rule and acceptance limits. Retain individual readings and exceptions with the conditions that produced them. A selected setting or maximum-torque specification is not, by itself, a measured accuracy or repeatability result.
Buyer takeaway: agree the method before samples are tested, separate accuracy from repeatability and keep changed fixtures or reference joints in a separate dataset. Continue with the precision screwdriver torque guide and the torque accuracy and repeatability method.
Evidence type: Technical measurement method; public model pages do not establish unpublished tolerances or pass rates.01MODEL / METHOD / SAMPLE PLAN
Torque test scope
The order-specific plan should name the model, mode, fixture, instrument, cycles, sampling and limits. This public page does not claim that every unit receives one universal torque test.
02FUNCTION / APPEARANCE / PACK-OUT
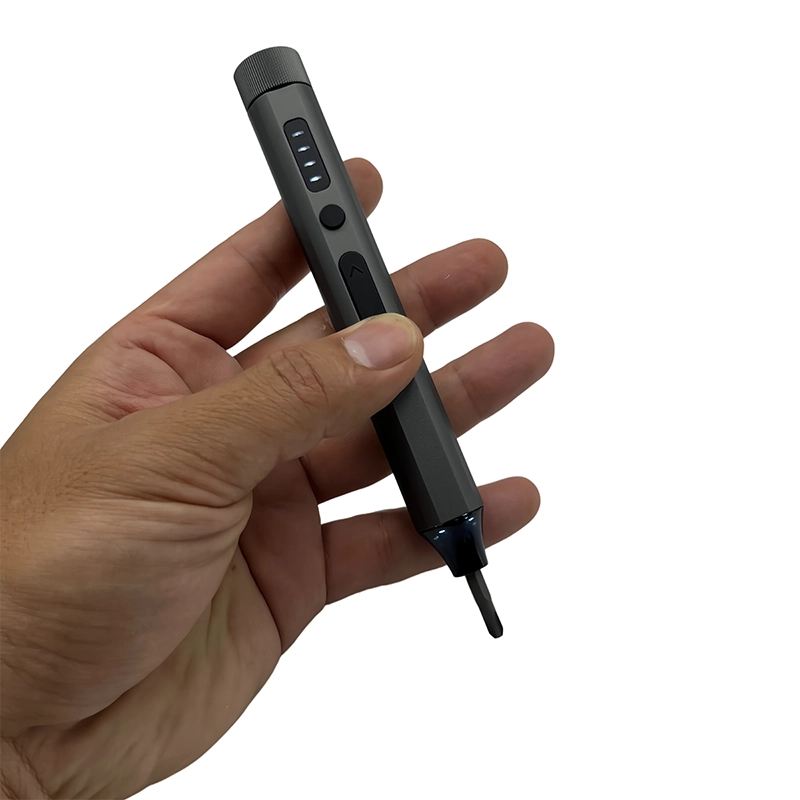
Function & finish scope
Direction, speed, charging, noise, appearance and accessory fit can be assigned to incoming, in-process or final checks according to the approved product and order plan.
03AGREED SCOPE / IDENTIFIED SAMPLE
Reliability sampling plan
Aging, cycle or temperature work should identify the exact model, condition, sample, endpoint and record. Availability and scope are confirmed for the project rather than inferred from this overview.
04IDENTITY / LABEL / PROTECTION
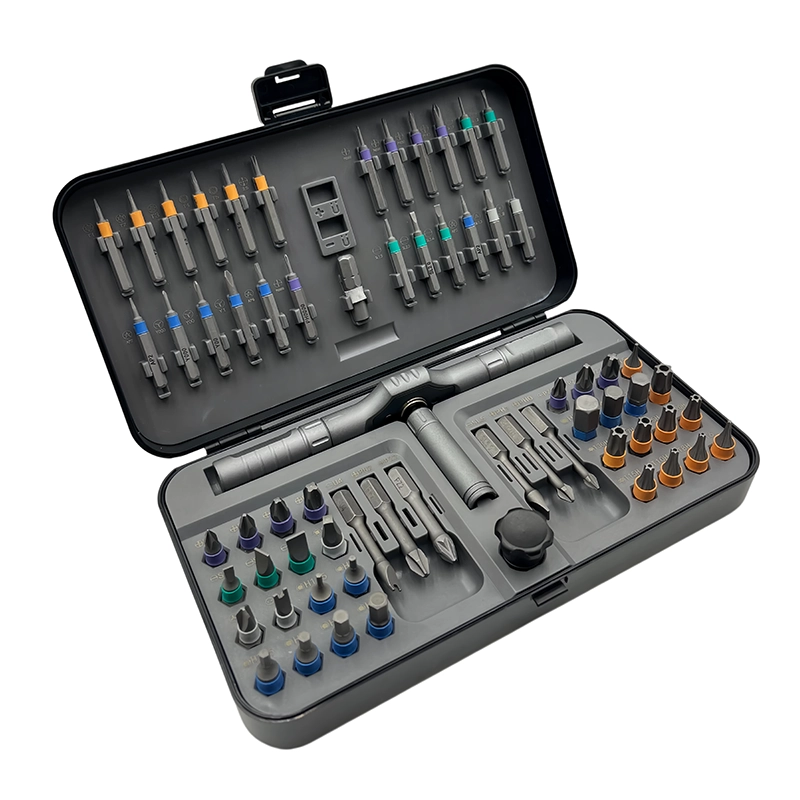
Pack-out release
The release plan should cover the approved product, bit map, accessories, labels, quantity and transport protection, with deviations recorded before shipment.
DELIVERY CAPABILITY
Flexible production. Planned global delivery.
Company materials state 3–5 days for standard samples and 10–15 days for a typical 1,000-unit standard production order. Customized schedules are confirmed after configuration review.
FOBEXWCIFDDPAIRSEAEXPRESS
REQUEST A PRODUCTION PLAN →Project inquiry
Bring us the brief.
Share your product, market, quantity and customization requirements. Our project team will reply with the right next step.