Limit finishing to noncritical flash and preserve designed radii and protective surface sections. For this job, control load path, UV-exposed surface, temperature, edge geometry and coating plan. Stop if a structural corner becomes sharp, a wall thins or heat gloss masks a smear. Accept the work only when the part retains its drawing features and the approved coating or weathering preparation.
finish ASA outdoor 3D printed part
finish ASA outdoor 3D printed part is the controlled process of deburring an outdoor sensor enclosure or functional bracket, using an approved method while protecting ASA exposed to weather where wall thickness, edge radius and coating adhesion may matter and verifying that the part retains its drawing features and the approved coating or weathering preparation.
Limit finishing to noncritical flash and preserve designed radii and protective surface sections. For this job, control load path, UV-exposed surface, temperature, edge geometry and coating plan. Stop if a structural corner becomes sharp, a wall thins or heat gloss masks a smear. Accept the work only when the part retains its drawing features and the approved coating or weathering preparation. This article treats finish ASA outdoor 3D printed part as one controlled customer question, not as a claim that every accessory or speed suits every material. The working example is deburring an outdoor sensor enclosure or functional bracket; final suitability still depends on the customer’s sample, instructions and acceptance method.
Finishing an ASA Outdoor 3D Printed Part Without Weak Edges concerns ASA exposed to weather where wall thickness, edge radius and coating adhesion may matter. That physical context changes the decision because geometry, heat, debris, tool access and inspection are connected. Before finish ASA outdoor 3D printed part, identify the area that may be touched, the areas that must remain unchanged and the exact evidence that will close the job.
What should be protected when an ASA bracket or enclosure is mechanically finished?
Limit finishing to noncritical flash and preserve designed radii and protective surface sections. For finish ASA outdoor 3D printed part, begin with a clean representative workpiece and photograph the starting condition. Mark the defect, orient the part so the tool moves away from hands and protected edges, and make one short trial. Clean the area before judging it; loose dust and temporary heat gloss can hide a changed contour.
Why does finish ASA outdoor 3D printed part need a task-specific plan?
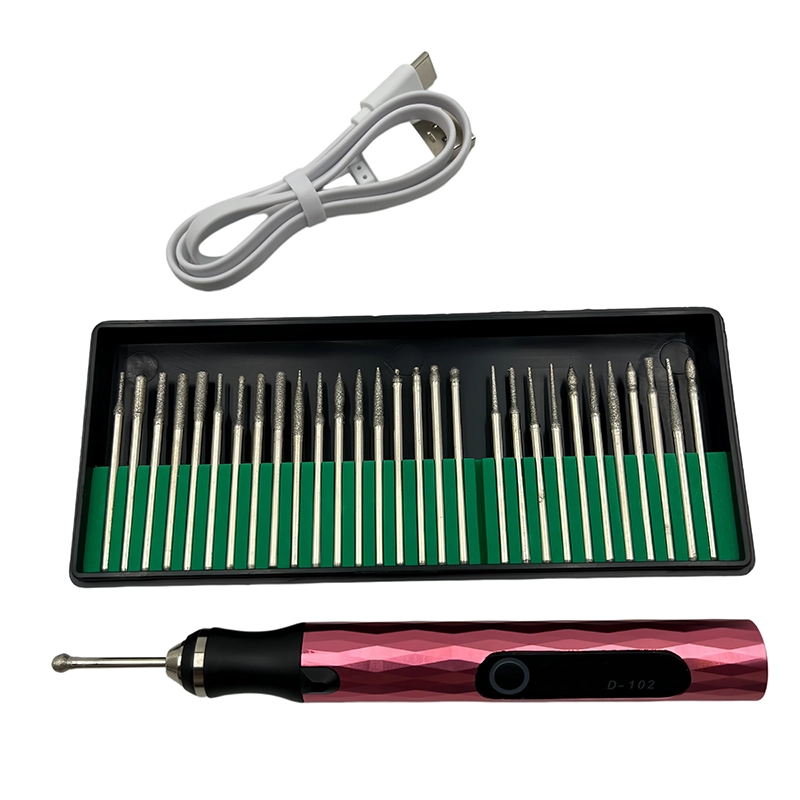
The real application is deburring an outdoor sensor enclosure or functional bracket, while the material condition is ASA exposed to weather where wall thickness, edge radius and coating adhesion may matter. A generic accessory count does not define a process. The plan for finish ASA outdoor 3D printed part must state why material is being removed, how much change is allowed, which direction the operation proceeds and who decides whether a damaged feature should be reworked, replaced or left untouched.
Which variables control finish ASA outdoor 3D printed part?
Control load path, UV-exposed surface, temperature, edge geometry and coating plan. Change one variable at a time and retain a known sample for comparison. Accessory diameter changes surface speed; pressure and dwell change heat; support changes vibration; and debris changes what the operator can see. During finish ASA outdoor 3D printed part, the lowest useful intervention is preferable to repeated aggressive correction that gradually erases the intended geometry.
How should the first-piece test for finish ASA outdoor 3D printed part be prepared?
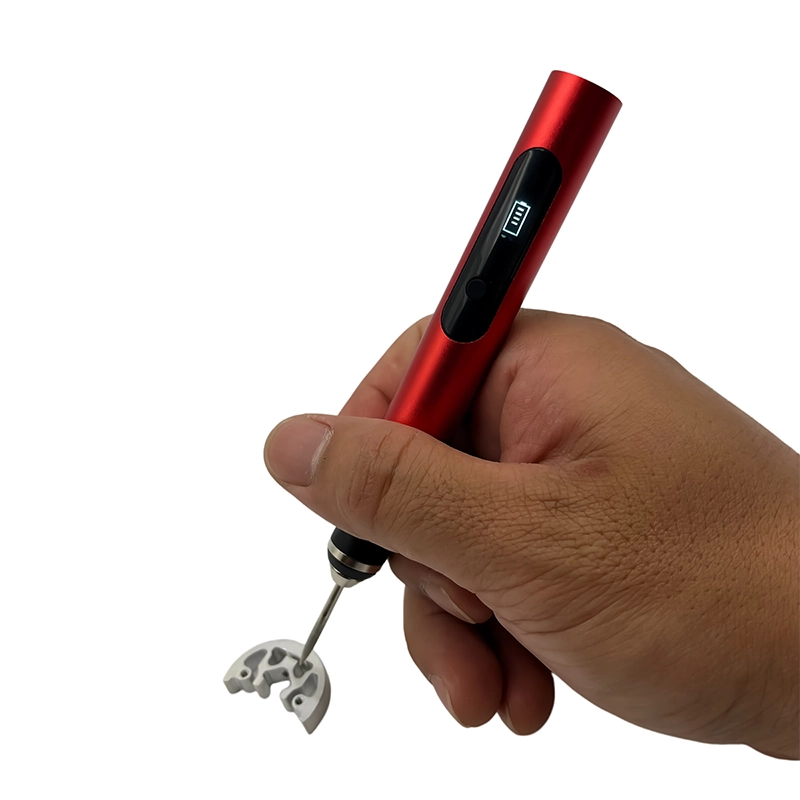
Use the same ASA exposed to weather where wall thickness, edge radius and coating adhesion may matter and a feature that represents the customer’s geometry. Record the D-102 cordless electric engraving pen reference, installed accessory, workholding, contact sequence and inspection tool. For finish ASA outdoor 3D printed part, approve the first piece only after it has been cleaned and returned to a stable temperature, then repeat the method on another sample to reveal operator-dependent variation.
When should powered work stop during finish ASA outdoor 3D printed part?
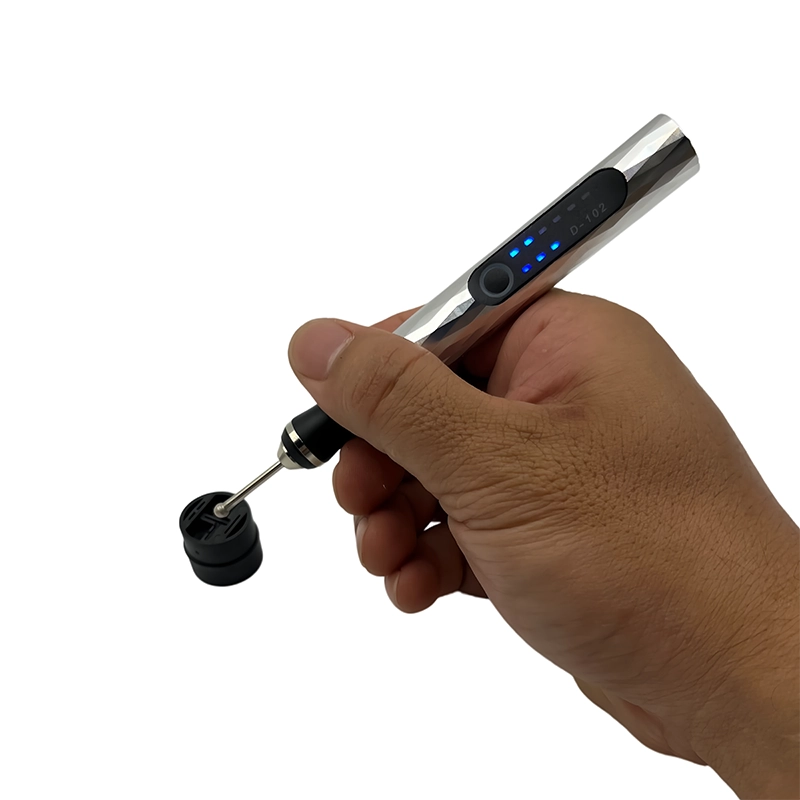
The practical stop signal is that a structural corner becomes sharp, a wall thins or heat gloss masks a smear. Stop power, isolate the accessory and inspect the work before deciding what changed. More speed or force rarely repairs a process that has lost support or alignment. A professional finish ASA outdoor 3D printed part instruction should make this signal visible so a technician does not continue merely because the original defect is still present.
How do sharp manual deburring and controlled rotary spot finishing compare for finish ASA outdoor 3D printed part?
sharp manual deburring gives a different balance of reach, reference control and cycle time than controlled rotary spot finishing. Test both against the same starting defect and measure more than speed. For finish ASA outdoor 3D printed part, compare edge condition, fit, debris, temperature, consumable wear and operator access. The better method is the one that repeatedly protects the acceptance requirement, even when it takes longer.
What proves finish ASA outdoor 3D printed part is acceptable?
The acceptance condition is that the part retains its drawing features and the approved coating or weathering preparation. Use the stated gauge, mating component, movement check, fixed lighting or retained finish reference. The result of finish ASA outdoor 3D printed part should be inspected after cleaning because residue can disguise scratches or missing material. If a critical feature cannot be verified, quarantine it rather than using cosmetic finishing to hide uncertainty.
Which product details matter when buying for finish ASA outdoor 3D printed part?
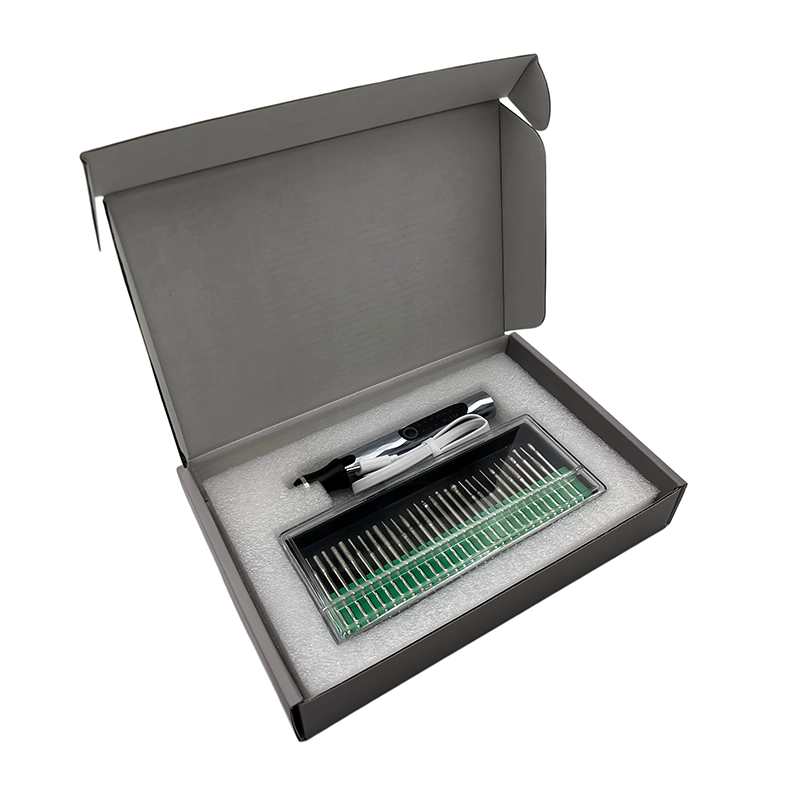
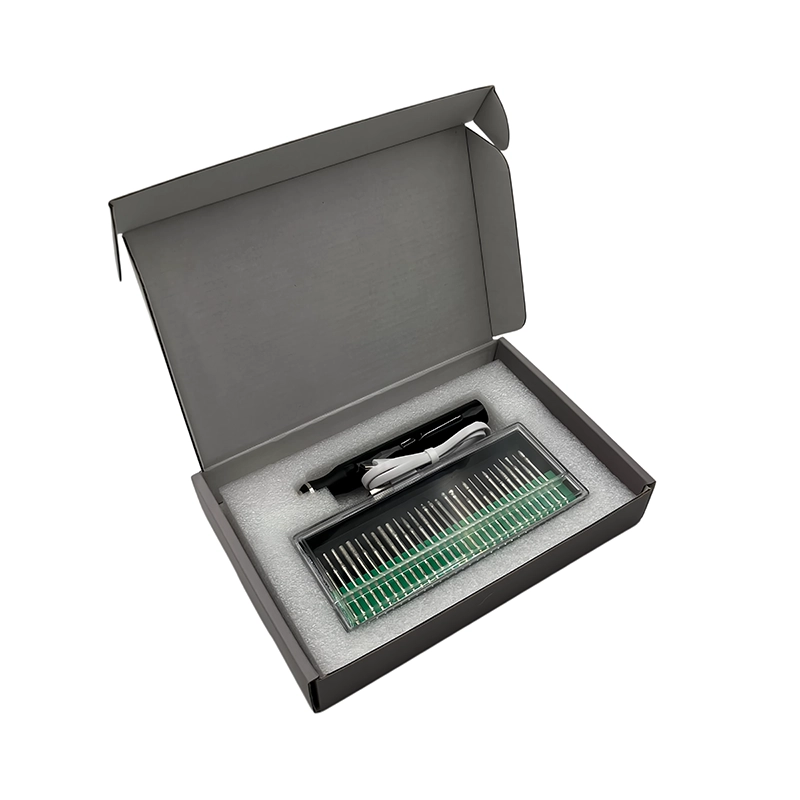
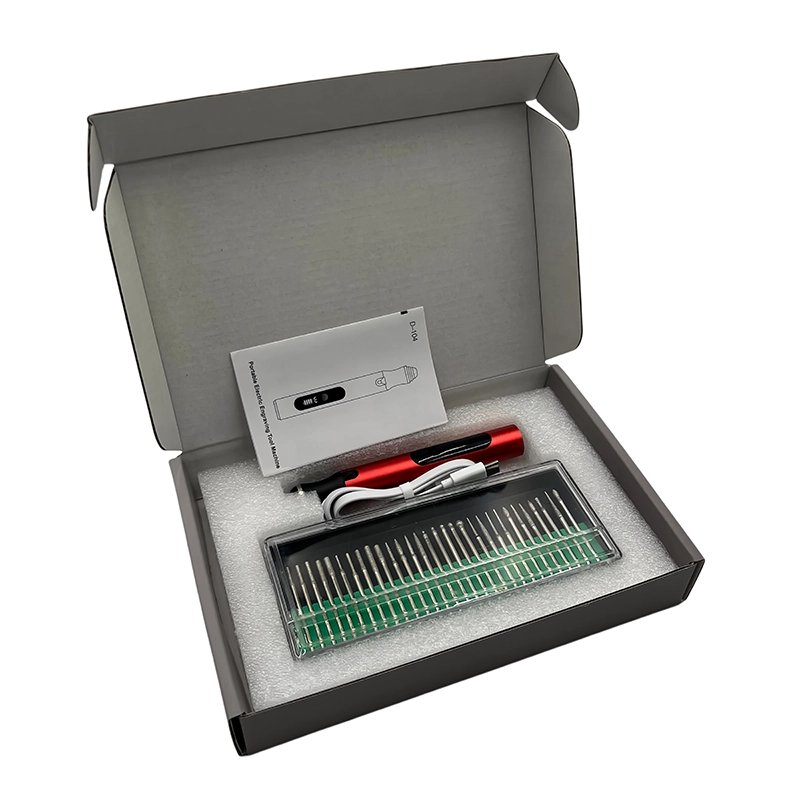
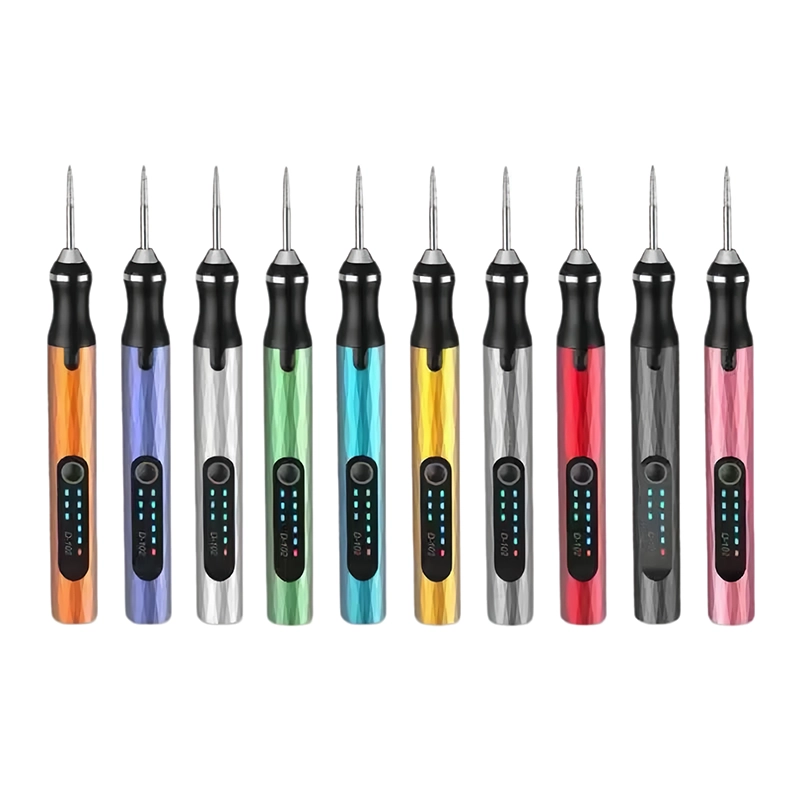
The current D-102 cordless electric engraving pen provides a real XOENAEN product reference, but it does not make finish ASA outdoor 3D printed part a validated universal application. Buyers should examine control layout, compatible shanks, accessory identity, charging pack-out, storage and replacement items. The target workpiece and acceptance method remain the sample approval basis, and all application claims should stay within that evidence.
What should an OEM brief record for finish ASA outdoor 3D printed part?
identify outdoor exposure and protected load features in the sample plan. Add target market, monthly volume, material mix, accessory map, case layout, label language, manual requirements and sample timing. For finish ASA outdoor 3D printed part, the brief should also identify workplace controls for dust, flying debris, heat or charging where relevant, so the proposed configuration can be assessed without inventing missing operating conditions.
How should finish ASA outdoor 3D printed part become a repeatable work instruction?
Write the approved sequence in plain observable terms: starting condition, protected zone, workholding, accessory, direction, short-pass rule, stop signal and final check. Keep rejected media separate and reapprove after a component change. This approach makes finish ASA outdoor 3D printed part transferable between trained operators while preserving the central rule that the actual part and customer requirement control the decision.
For the retained finish ASA outdoor 3D printed part record, identify ASA exposed to weather where wall thickness, edge radius and coating adhesion may matter, photograph the accepted setup and link the instruction to its product, accessory and inspection revision. Recheck the method whenever the workpiece, media, charging configuration or operator access changes. The release note should repeat the acceptance rule—the part retains its drawing features and the approved coating or weathering preparation—so later production cannot replace evidence with a subjective statement that the surface simply looks better.
sharp manual deburring compared with controlled rotary spot finishing for finish ASA outdoor 3D printed part
| Method | Useful when | Main control |
|---|---|---|
| sharp manual deburring | Reference control is important during deburring an outdoor sensor enclosure or functional bracket | load path, UV-exposed surface, temperature, edge geometry and coating plan |
| controlled rotary spot finishing | Localized access is needed for deburring an outdoor sensor enclosure or functional bracket | a structural corner becomes sharp, a wall thins or heat gloss masks a smear |
- Define the customer question: What should be protected when an ASA bracket or enclosure is mechanically finished?
- Identify the working material: ASA exposed to weather where wall thickness, edge radius and coating adhesion may matter
- Control load path, UV-exposed surface, temperature, edge geometry and coating plan
- Use this stop signal: a structural corner becomes sharp, a wall thins or heat gloss masks a smear
- Approve only when the part retains its drawing features and the approved coating or weathering preparation
- Complete the buyer action: identify outdoor exposure and protected load features in the sample plan
- D-102 cordless electric engraving pen →
- OEM and ODM development →
- Manufacturing and quality control →
- Related guide: Finishing Polycarbonate 3D Prints Without Heat Gloss or Cracks →
- Read the related remove-epoxy-resin-casting-flash guide →
- Read the related write-private-label-rotary-tool-limitations guide →
- Continue with the finish-multi-material-3d-print-seam topic →
- How XOENAEN presents quality evidence →
What should be inspected before finish ASA outdoor 3D printed part begins?
Inspect the actual ASA exposed to weather where wall thickness, edge radius and coating adhesion may matter, mark protected geometry and confirm the acceptance reference. For finish ASA outdoor 3D printed part, the operator also needs stable workholding and a clear stop rule before the tool or abrasive touches the part.
Which stop signal matters most during finish ASA outdoor 3D printed part?
Stop when a structural corner becomes sharp, a wall thins or heat gloss masks a smear. That observation means the chosen contact, accessory, support or method is no longer controlling the task, so cleaning and reassessment are safer than adding pressure or dwell.
Is sharp manual deburring better than controlled rotary spot finishing for finish ASA outdoor 3D printed part?
sharp manual deburring is usually stronger where broad reference control matters, while controlled rotary spot finishing can reach a localized feature. Compare both on the same deburring an outdoor sensor enclosure or functional bracket sample and judge them against the part retains its drawing features and the approved coating or weathering preparation.
How should a first-piece test document finish ASA outdoor 3D printed part?
Record the material, starting defect, workholding, accessory, sequence, stop observation and final inspection. A useful finish ASA outdoor 3D printed part record lets another trained person repeat the decision without relying on vague phrases such as light pressure.
What should a buyer specify for finish ASA outdoor 3D printed part?
identify outdoor exposure and protected load features in the sample plan. The brief should also state expected quantity, market, accessory pack, packaging, documentation and the sample that will prove the configuration is suitable for this exact customer question.
Which evidence proves finish ASA outdoor 3D printed part is complete?
Completion requires the cleaned and cooled workpiece to satisfy this defined condition: the part retains its drawing features and the approved coating or weathering preparation. Appearance alone is insufficient when a gauge, mating part, motion check or retained finish reference is available.