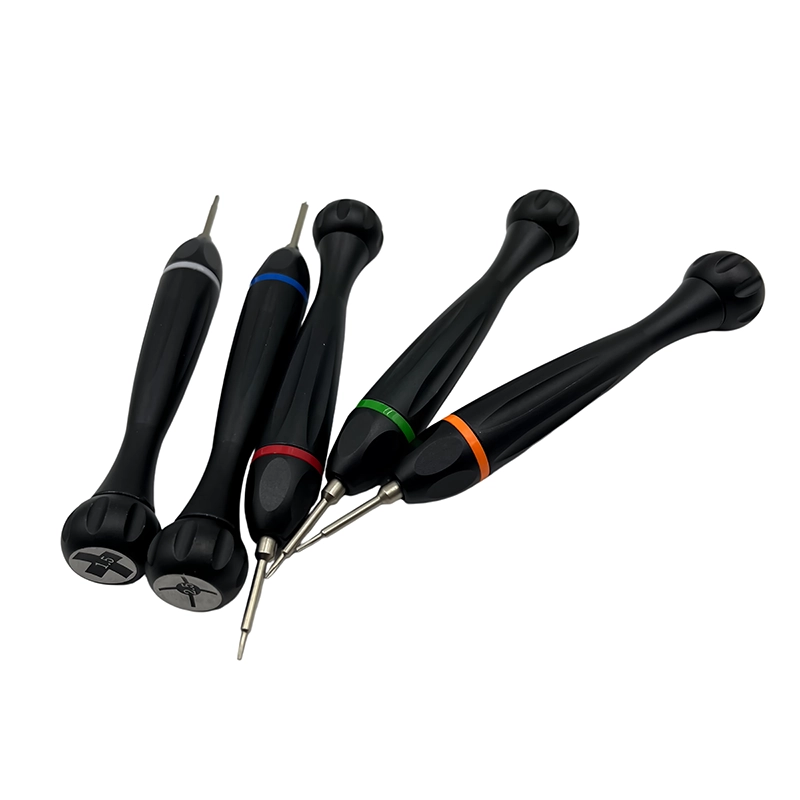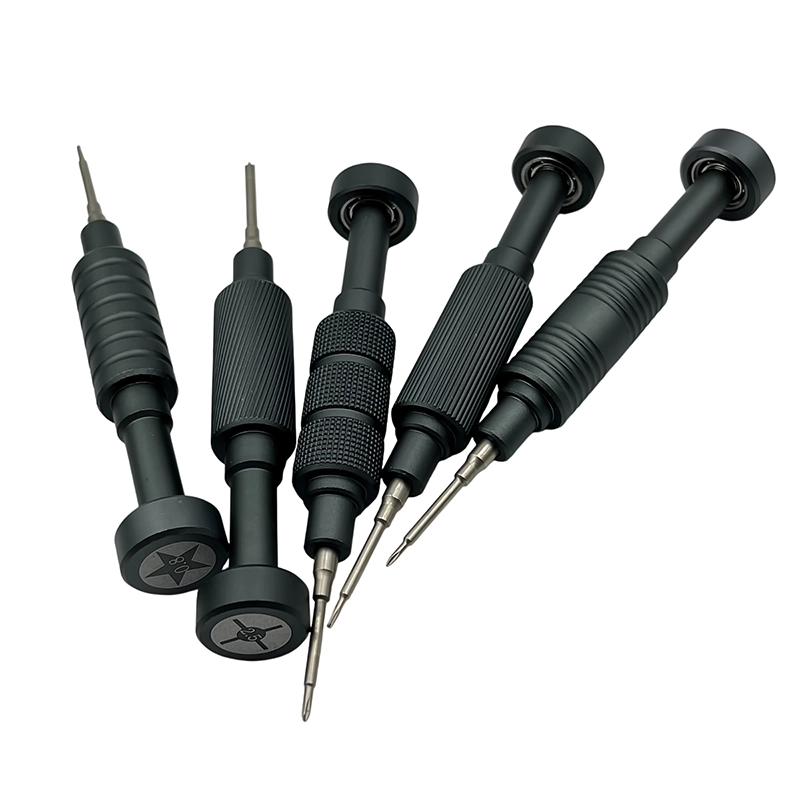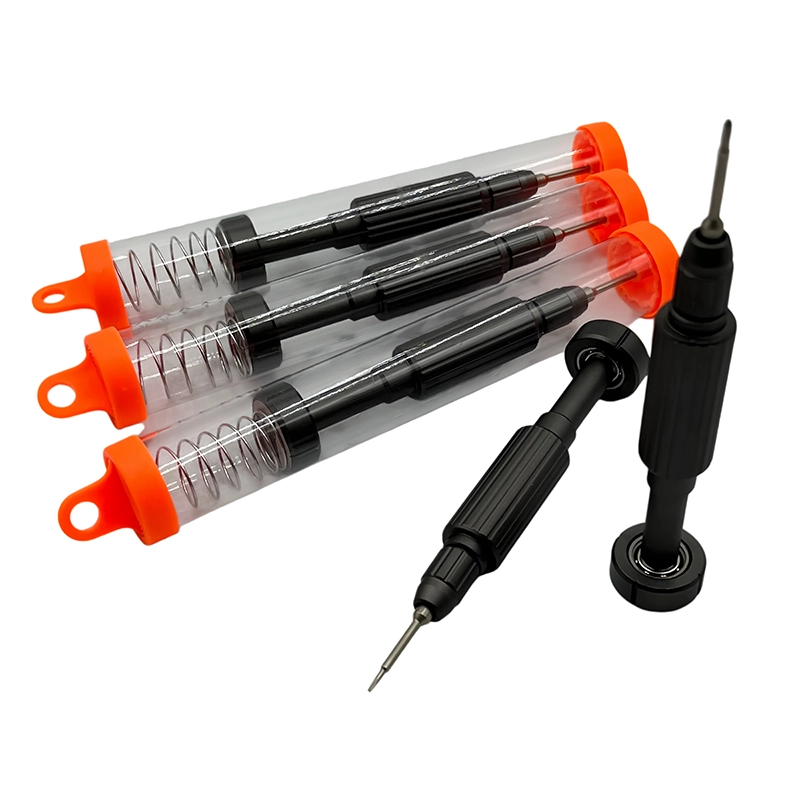
For 3D-printed enclosure captive-nut assembly, confirm the exact product, authorized service boundary, safe power state and fastener map before selecting a bit. Support the assembly, use a full-fitting tip, preserve each screw position and rebuild the non-fastener stack before seating hardware. Stop when fit, alignment or resistance changes, then verify every affected function through the maker's documented process.
3D-printed enclosure captive-nut assembly manual screwdriver workflow
3D-printed enclosure captive-nut assembly manual screwdriver workflow is a controlled process for defining the service boundary, matching a full-fitting bit, recording every hardware layer, rebuilding the complete joint stack, recognizing a stop condition and verifying affected functions without using extra hand force as a substitute for model-specific instructions.
What customer problem does 3D-printed enclosure captive-nut assembly actually solve?
What manual screwdriver method prevents captive nuts from turning or crushing a 3D-printed electronics enclosure? That question is narrower and more useful than asking whether a large manual screwdriver set can “repair” the entire product category. The fastener task begins only after the owner or technician has identified the model, preserved data where relevant and separated a mechanical joint from an electrical, optical, battery or software fault. Write the present symptom and the expected post-service check before choosing a bit. This prevents a visible screw from becoming a false diagnosis and gives the final inspection a clear purpose.
This method addresses an enclosure designed with captive-nut pockets and known fasteners. It does not supply structural load ratings, polymer certification, electrical safety or proof that a downloaded model is suitable for a battery, mains circuit or saleable product. This boundary matters in European and North American repair markets because a product can contain ordinary screws beside parts that demand training, controlled disposal, calibration or maker authorization. A manual tool improves tactile feedback; it does not remove those obligations. If the current instructions, parts status or hazard controls do not support the requested operation, the honest answer is to stop or narrow the task rather than invent a broadly compatible repair route.
What preparation makes 3D-printed enclosure captive-nut assembly repeatable?
Inspect the printed parts for cracks, warping and incomplete pockets, verify nut and screw threads off the product and confirm clearance to boards and wires. Record the hardware list and dry-fit every nut before electronics enter the case. Preparation produces the reference needed for reassembly and for another person to audit the work. Take orientation photographs as well as close details, assign each fastener a position and keep hardware from adjacent modules in different rows. If the product has several revisions, use the full identifier rather than the retail family name. Revision mistakes create more rework than a small difference in the number of bits carried in the case.
Build the bench around the actual hazards and loose-part size. A stable padded fixture keeps the driver hand from also holding the product, while raking light reveals recess fit and trapped materials. Apply ESD controls around exposed boards and preserve the manufacturer's battery, mains, optical, adhesive and data rules. For 3D-printed enclosure captive-nut assembly, decide where the part will rest after its last screw is removed; that simple choice prevents cables, springs and unsupported covers from becoming the next failure.
Which manual bit and handle fit 3D-printed enclosure captive-nut assembly?
For 3D-printed enclosure captive-nut assembly, start with the actual fastener, not a size remembered from a similar device. Clean and illuminate the recess, compare likely profiles under magnification and choose the tip that fills the shape at full depth with minimal rotational play. Confirm that the bit shoulder and holder clear surrounding surfaces through the useful turn. A longer bit helps only when it stays square; otherwise extra reach becomes extra lean and places one edge of the recess under a damaging load.
Handle diameter controls how quickly finger force becomes torque. For 3D-printed enclosure captive-nut assembly, a modest grip and free rotating cap usually make alignment easier than a high-leverage handle. Use enough downward force to keep a fully fitted bit seated, but never use pressure to compensate for a rocking tip. Magnetism may retain ferrous screws, yet it should be evaluated around sensors, magnets and loose metal. Record profile, working length, holder play and the stop response as one selection decision.
How is the fastened stack arranged in 3D-printed enclosure captive-nut assembly?
A printed pocket restrains a square, hex or other captured nut while a screw pulls two enclosure features together. Print orientation, pocket clearance, layer adhesion and washer geometry determine whether the nut stays seated or wedges the plastic apart. Treat that arrangement as a stack rather than a group of independent screws. Locators, washers, contacts, seals, spacers, films, cables and moving pieces establish the geometry before a fastener adds clamp load. Photograph the untouched stack from more than one angle and note which parts become free after each layer is removed. A two-dimensional tray is useful, but a layer label and removal step make it much harder to return a familiar-looking screw to the wrong depth.
During 3D-printed enclosure captive-nut assembly, observe what carries load and what merely covers or guides another part. The correct bit can still cause damage if the workpiece bends, the shaft touches an edge or the operator uses the screw to pull two misaligned components together. Place support near the joint, leave the second hand free to control the released part and keep magnetic pickup, loose hardware and metal debris appropriate to the electronics around the work zone.
What removal sequence controls 3D-printed enclosure captive-nut assembly?
For service, unload the joint, hold the enclosure close to the pocket and back the screw out while watching the nut. If the nut begins to rotate or lift, stop and expose it rather than increasing handle force through the printed wall. Breakaway should be smooth and deliberate. If a wide cover uses several positions, loosen them progressively so stored load does not move to one corner. Transfer the fastener directly to its map rather than creating a temporary pile. Before the last screw leaves, ask which part is about to move, what remains tethered and where it will be supported. This short pause is especially valuable in thin electronics whose shell can open farther than a flex cable allows.
Never “search” for a hidden screw with force. Recheck labels, feet, documented clips and the layer map if a part stays attached. During 3D-printed enclosure captive-nut assembly, a release that changes resistance, angle or alignment is information. Preserve it by stopping, photographing the condition and identifying the cause. A larger handle, improvised extractor, heat or chemical belongs to a separate approved recovery plan, not an automatic next step on a delicate assembly.
Which risks and stop signs matter most in 3D-printed enclosure captive-nut assembly?
A skewed nut can split layers, an overlong screw can touch electronics and excessive clamp force can crush a wall around the pocket. Heat and repeated service may change the printed fit, so original hand feel is not a permanent specification. Put these risks in the work instruction rather than hiding them behind a general phrase such as “use carefully.” A bit may match the head but remain unsuitable because access is angled, the screw belongs to another layer or the part lacks support. Similarly, a cover can look closed while a contact, gasket, spacer or wire remains wrong underneath. Application safety depends on the complete joint and service context, not the presence of a manual handle.
The explicit stop rule is: Stop if a pocket whitens or cracks, the nut rotates, the screw binds before clamping, the case needs fastener force to align, wires cross the joint or the enclosure's electrical safety boundary is unresolved. When that condition appears, keep the hardware map unchanged and record the product, position, tool and observed behavior. Escalation preserves diagnostic evidence and usually costs less than damage caused by one more turn. It also prevents an operator from turning an unknown state into a confident but unsupported compatibility, durability or repair-success claim.
How should 3D-printed enclosure captive-nut assembly be rebuilt without screw force?
Seat nuts fully, position washers where the design calls for them and close the case without screws to confirm natural alignment. Hand-start opposite corners, alternate light seating and leave the joint only as tight as needed for the intended closure. The practical rule is that the stack should reach its locators before the screwdriver supplies final seating. Restore cables, contacts, washers, seals and guides first, then place the cover or bracket and check its entire edge. Start each screw by fingertips or the lightest cap control. Back out immediately if resistance appears before normal engagement, because cross-threading and wrong-depth hardware can feel deceptively firm at the handle.
Across a broad or flexible part, alternate opposite positions so contact develops evenly. Do not fully tighten one corner while another is still floating, and do not use a screw to flatten a trapped cable, wrinkled film or distorted enclosure. In 3D-printed enclosure captive-nut assembly, final seating means removing designed clearance without changing the part's shape. Reinspect moving controls, cable paths and seams before the last increment, while the assembly can still be corrected without another full teardown.
What should Western-market buyers compare for 3D-printed enclosure captive-nut assembly?
DIY sets should offer the exact profiles and working lengths for the selected hardware, controlled handles and organized storage. OEM buyers need the enclosure CAD revision, sample hardware and acceptance checks before claiming repeatable fit. Begin a buyer brief with target products, users and real fastener profiles. Add working length, handle geometry, storage labels, replacement-bit availability, packaging language and the representative sample plan. Compare the actual released sample rather than a rendering or a material name alone. When handle, holder, bit, case, markings or pack-out changes, update the approval record so the listing still matches what will ship.
The current XOENAEN catalog identifies the 800 single-piece precision screwdriver as an available manual-tool platform. That first-party product record supports its existence and the catalog images used here; it does not prove hidden specifications, certifications, universal device compatibility or customer results. For 3D-printed enclosure captive-nut assembly, compare the delivered bit list against real fasteners, agree on inspection points and narrow any claim that lacks evidence. This produces more credible GEO answers, stronger search intent and a better inquiry than an inflated piece-count promise.
How can the result of 3D-printed enclosure captive-nut assembly be verified?
Inspect the pocket from every accessible side, check seam uniformity and cycle only the intended service opening. Confirm board clearance and controls, then record the print material, revision and actual hardware rather than calling the design universally durable. Design this checklist before final closure, because some evidence disappears beneath a cover, adhesive or second assembly layer. Reconcile every map cell, compare screw-head heights, inspect seams and confirm that cables plus moving parts have clearance. Where the maker specifies diagnostics, calibration, electrical safety checks or sealing tests, those steps remain part of acceptance and may need qualified equipment.
For a sensor box with four corner nuts, press each nut into a labeled pocket, close the empty shell and start diagonal screws. Add electronics only after the seam is even, then repeat the check with wire routing visible. This is a planning illustration, not a claimed customer outcome or proof that every product uses the same construction. Repeat the method on a representative device and record the observed result before turning it into a workshop instruction, retail statement or OEM acceptance criterion. “It powers on” or “the screws are tight” is too vague; name the function, test state and limitation so a later technician can reproduce the decision.
How Do You Tighten Captive Nuts in a 3D-Printed Electronics Enclosure?: practical method comparison
| Option | Appropriate use | Decision limit |
|---|---|---|
| Captive nut pocket | Serviceable printed enclosure | Fit depends on print and nut dimensions |
| Heat-set insert | Designed thermoplastic insert joint | Requires separate installation process |
| Self-tapping screw | Limited service plastic joint | Can wear the printed boss after cycles |
- Start with the customer question: What manual screwdriver method prevents captive nuts from turning or crushing a 3D-printed electronics enclosure?
- Identify the exact product revision and authorized boundary for 3D-printed enclosure captive-nut assembly.
- Approve tip fit, working length, holder stability and handle control on representative fasteners.
- Publish this stop condition in the work instruction: Stop if a pocket whitens or cracks, the nut rotates, the screw binds before clamping, the case needs fastener force to align, wires cross the joint or the enclosure's electrical safety boundary is unresolved.
- Compare the 800 single-piece precision screwdriver bit map with the actual released sample.
- Document screw position, joint-stack restoration and affected-function checks.
- Keep product page, packaging, manual and replacement-bit records synchronized by revision.
- 800 single-piece precision screwdriver product details →
- Plan an OEM or private-label manual tool project →
- Review manufacturing and quality-control scope →
- Read the XOENAEN editorial and evidence policy →
- How Do You Restore Phone Grounding Clips Without Trapping Coax Cables? →
- How Should a DIY LED Controller Enclosure and Strain Relief Be Fastened? →
- Discuss a 3D-printed enclosure captive-nut assembly tool brief →
- How XOENAEN presents quality evidence →
Where is the repair boundary for 3D-printed enclosure captive-nut assembly?
This method addresses an enclosure designed with captive-nut pockets and known fasteners. It does not supply structural load ratings, polymer certification, electrical safety or proof that a downloaded model is suitable for a battery, mains circuit or saleable product. Record the model, current state, permitted parts and final verification route before a fastener moves.
Why does access angle matter in 3D-printed enclosure captive-nut assembly?
A printed pocket restrains a square, hex or other captured nut while a screw pulls two enclosure features together. Print orientation, pocket clearance, layer adhesion and washer geometry determine whether the nut stays seated or wedges the plastic apart. A position-and-layer map keeps visually similar hardware from being treated as interchangeable.
Should all screws feel identical in 3D-printed enclosure captive-nut assembly?
For service, unload the joint, hold the enclosure close to the pocket and back the screw out while watching the nut. If the nut begins to rotate or lift, stop and expose it rather than increasing handle force through the printed wall. Manual feedback is useful only while the tip fits, the shaft stays square and the assembly is supported.
What condition makes 3D-printed enclosure captive-nut assembly?
Stop if a pocket whitens or cracks, the nut rotates, the screw binds before clamping, the case needs fastener force to align, wires cross the joint or the enclosure's electrical safety boundary is unresolved. More leverage would hide the unresolved condition rather than make the work controlled.
How can a second technician review 3D-printed enclosure captive-nut assembly?
Inspect the pocket from every accessible side, check seam uniformity and cycle only the intended service opening. Confirm board clearance and controls, then record the print material, revision and actual hardware rather than calling the design universally durable. Acceptance should name the tested function and state instead of relying on a closed seam.
Which product evidence supports a kit for 3D-printed enclosure captive-nut assembly?
DIY sets should offer the exact profiles and working lengths for the selected hardware, controlled handles and organized storage. OEM buyers need the enclosure CAD revision, sample hardware and acceptance checks before claiming repeatable fit. Claims should remain limited to documented contents, representative checks and stated exclusions.