Quick Answer: Test the saleable pack through the agreed distribution sequence, then open it in a controlled orientation and record movement, damage and label readability. Accept the job only when all items remain identifiable and undamaged with the case, labels and carton meeting the written approval rule.
ratchet screwdriver case transit test
ratchet screwdriver case transit test is the controlled selection and use of a hand ratchet, compatible bit and documented workflow for ratchet-case transit and pack-out verification, including access, support, stop rules and final inspection.
The practical setting for ratchet-case transit and pack-out verification is approving a retail case, inner pack and export carton before ratchet-set production. This article treats the ratchet screwdriver as one controlled element inside a larger installation, repair or approval process. It favors useful hand feedback, an explicit stop rule and documented acceptance over maximum leverage or accessory count. The distinctions matter because the same handle can behave very differently when the screw profile, receiving material, working depth or surrounding clearance changes.
How should a buyer test whether bits stay organized during shipping?
Test the saleable pack through the agreed distribution sequence, then open it in a controlled orientation and record movement, damage and label readability. That is the working answer for ratchet-case transit and pack-out verification, where the actual task is approving a retail case, inner pack and export carton before ratchet-set production. A ratchet screwdriver reduces repeated wrist repositioning, but its advantage exists only when the installed bit stays square, the work is supported and the operator can see or otherwise verify the fastener. The mechanism does not correct an incorrect profile, a damaged recess, a blocked thread, an unsafe service state or a component that was assembled under a different controlled procedure.
For ratchet-case transit and pack-out verification, separate the job into access, identification, movement and acceptance. Access establishes whether the handle and bit can follow the screw axis. Identification confirms the exact recess and receiving joint. Movement uses the ratchet only while feedback remains predictable. Acceptance means all items remain identifiable and undamaged with the case, labels and carton meeting the written approval rule. Keeping those four decisions separate gives a repair team or product buyer observable evidence instead of a vague claim that one set works everywhere.
Which field detail makes ratchet-case transit and pack-out verification a distinct customer question?
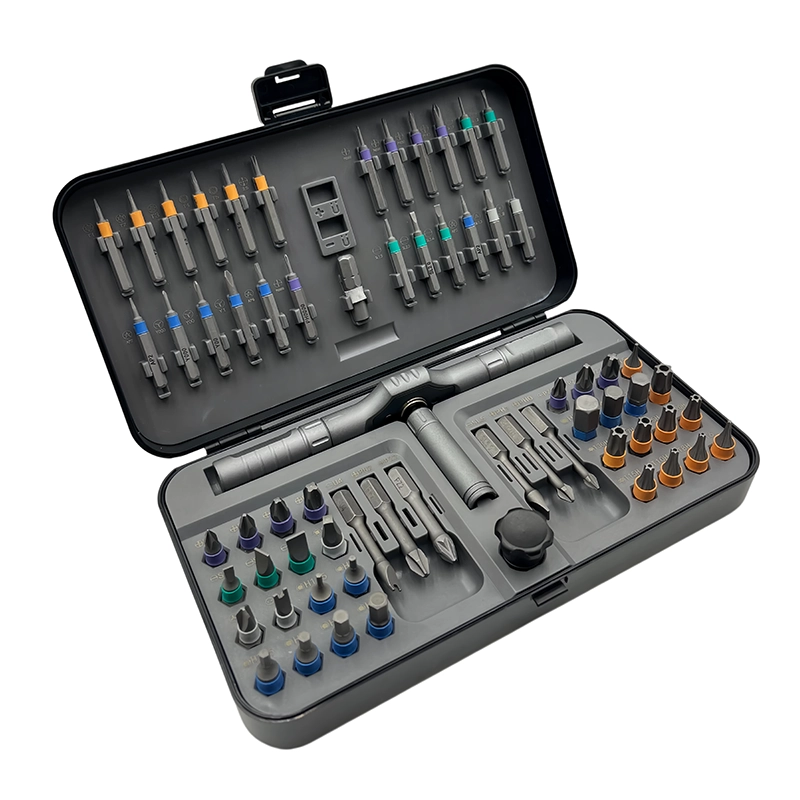
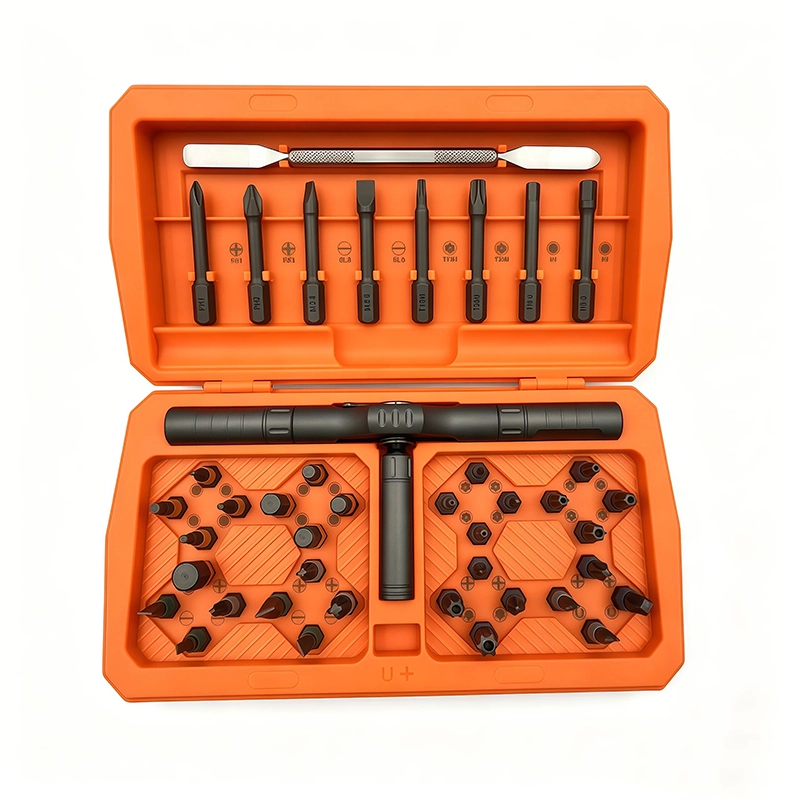
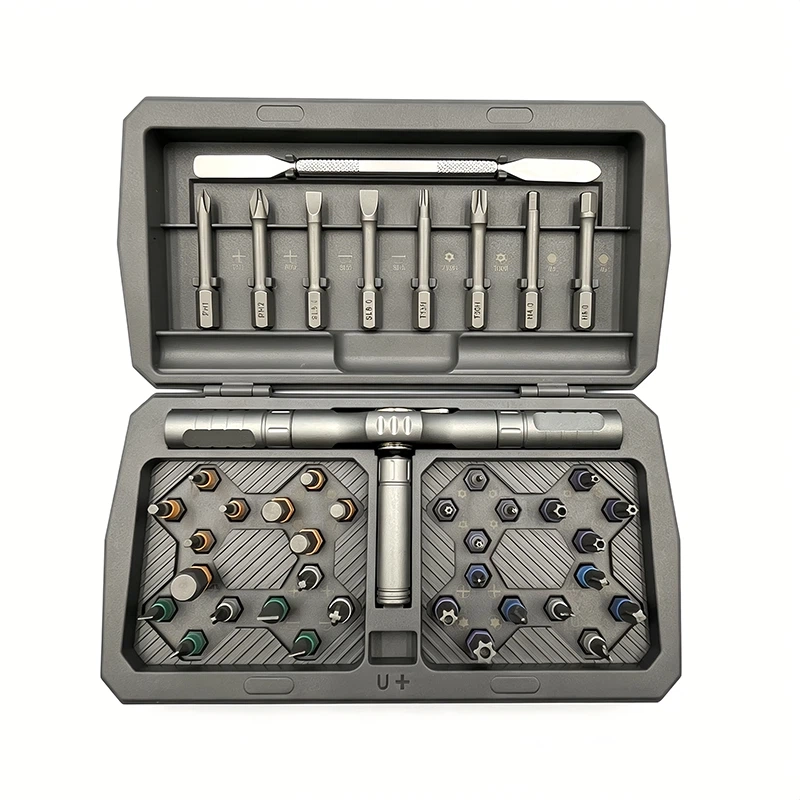
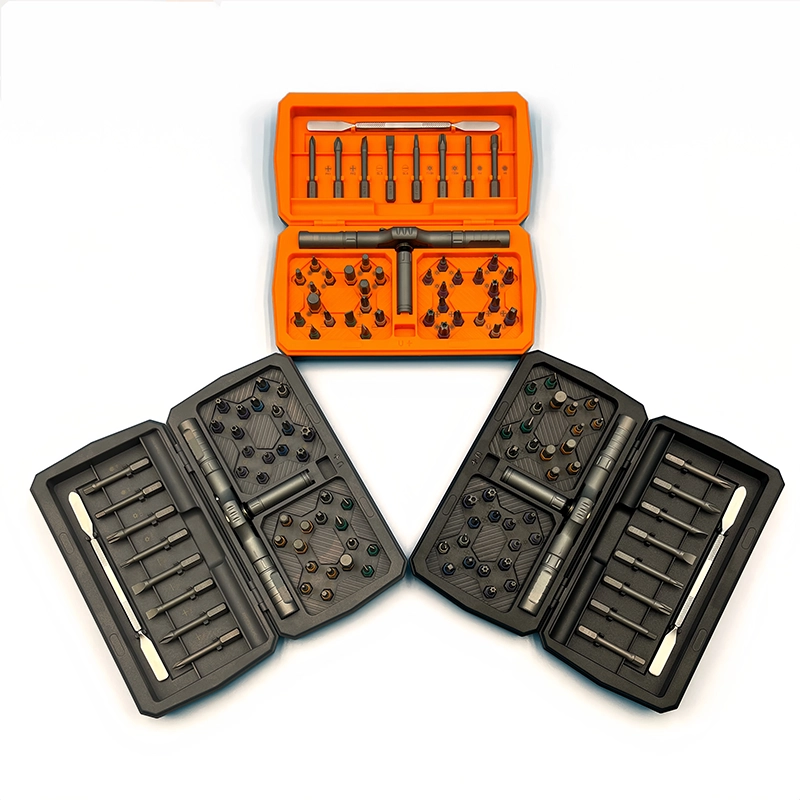
A transit check evaluates the saleable case inside its real pack-out, not an empty plastic shell on a bench. Define orientation, inner pack, carton, route simulation, sample count and failure criteria before testing. Open the pack in a controlled position and record migrated bits, latch release, scuffing and unreadable labels. The result belongs only to that case insert, accessory mass and packaging revision; a later insert change needs risk review.
What does “ratchet screwdriver case transit test” mean in this application?
In this guide, ratchet screwdriver case transit test means a hand-operated ratcheting setup selected specifically for ratchet-case transit and pack-out verification. The definition includes the handle mode, bit interface, working length, fastener condition, support method, access envelope and stop rule. It excludes electrical diagnosis, structural engineering, drilling, extraction, calibration and final torque work unless the accountable maker's instructions expressly place those actions within the same controlled method.
The physical reference is the complete tool pack whose small bits, handle and accessories must remain in assigned positions. A bit merely entering that recess is not enough. It should seat to the intended depth, resist rocking, clear nearby finishes and remain retained when the operator changes direction. If a screw standard, thread treatment, anchor, gasket, insert or service state is unknown, identification comes before leverage. This definition prevents ratchet-case transit and pack-out verification from being reduced to handle size or kit piece count.
Which fastener details control ratchet-case transit and pack-out verification?
The controlling variables for ratchet-case transit and pack-out verification are case latch, insert retention, accessory mass, retail orientation, inner pack, carton and test method. Inspect them as a linked system. A correct tip can still fail when its holder touches a wall before seating; an extended bit can reach the recess but magnify visible wobble; a compact handle can clear an obstacle but invite side load when the operator cannot support the joint. Record the actual screw, not a visually similar spare from a drawer.
Receiving material changes the decision. Sheet metal, molded plastic, wood, threaded inserts and machine threads provide different feedback and different consequences when engagement begins incorrectly. Surface coatings, corrosion, threadlocker, debris and repeated service history can further change resistance. During ratchet-case transit and pack-out verification, use early movement only as information. Unexpected resistance is a reason to stop and investigate, never an instruction to add hand force.
How should the work area be prepared for ratchet-case transit and pack-out verification?
Preparation begins by following the accountable product or installation procedure and establishing the safe work state for approving a retail case, inner pack and export carton before ratchet-set production. Support the assembly close to the joint, protect adjacent finishes and place a tray where a dropped bit or screw can be recovered without entering equipment. Photograph locations, lengths, washers, spacers and cable routes before removal. Clean the recess only with a method suitable for the material and preserve evidence of damage rather than covering it with a new scratch.
Next, inspect the ratchet selector, handle, holder and candidate bit away from the workpiece. Insert the bit fully, confirm retention and rotate the unloaded mechanism through the intended direction. For ratchet-case transit and pack-out verification, position the hand so the first swing cannot strike a finished surface, live area, sharp edge or fragile component. If the safe state, work support or sight line cannot be established, postpone ratcheting and choose the approved alternative.
What operating sequence keeps ratchet-case transit and pack-out verification controlled?
Start ratchet-case transit and pack-out verification by placing the verified bit into the recess without turning. Apply only enough axial hand pressure to maintain full contact, then take a short first stroke while watching both the screw and surrounding joint. After the initial response is known, use a repeatable swing that does not pull the bit sideways at either end. Reposition the work rather than turning the bit into a lever when clearance changes.
During reassembly, present every screw by hand and confirm natural thread engagement before using the ratchet. Bring multi-fastener panels or brackets down gradually instead of fully seating the first screw against a visible gap. Complete any specified torque, alignment, leak, electrical, structural or functional check with the method named by the maker. For ratchet-case transit and pack-out verification, the sequence ends only when all items remain identifiable and undamaged with the case, labels and carton meeting the written approval rule.
What can go wrong during ratchet-case transit and pack-out verification?
The primary failure path is that bits migrate into the mechanism, the latch opens or hidden case scuffing is accepted without a criterion. That outcome usually develops through a visible chain: incomplete bit seating creates local contact, local contact damages the recess, damage reduces feedback and the operator responds with extra pressure. Interrupt the chain at the first sign of rocking, climbing, scraping, joint movement or unexplained resistance. A ratchet's short return stroke should improve access, not justify continuing after control is lost.
A second failure path is configuration drift. A replacement bit, adapter, extension, case insert, translated instruction or fastener may look equivalent while changing reach or fit. For ratchet-case transit and pack-out verification, keep the approved sample and screw map connected to the current revision. Quarantine mixed, worn or unlabeled bits. When a change affects the interface or work method, repeat the relevant representative check instead of transferring an old result by assumption.
Which method should a buyer compare for ratchet-case transit and pack-out verification?
Compare case-only shake screening with documented complete-pack transit simulation. The first method should be evaluated for directness, visibility, installed length, retention and operator feedback. The second should be evaluated for the condition that justifies it, the added steps and the new failure modes it introduces. Neither description proves superiority by itself; the representative joint, documented boundary and acceptance rule decide which method is appropriate for ratchet-case transit and pack-out verification.
A useful comparison records the same evidence for both methods: time to prepare, profile fit, clearance at the tightest point, number of hand repositionings, observable stop signals, fastener condition after removal and final assembly condition. Do not compare an unloaded ratchet demonstration with a fully controlled alternative procedure. For ratchet-case transit and pack-out verification, equivalent test conditions matter more than an impressive feature list or unsupported speed claim.
How does XOENAEN 43-in-1 ratchet screwdriver set relate to ratchet-case transit and pack-out verification?
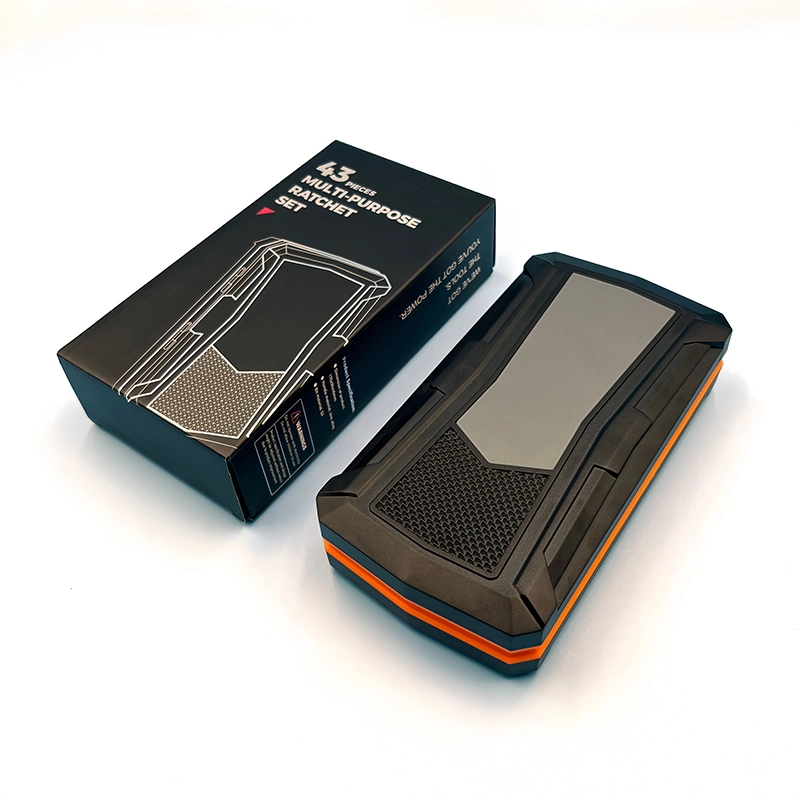
The current XOENAEN catalogue records forward, reverse and lock positions, 32 short 25 mm bits, eight extended 45 mm bits, a magnetizer and a metal pry bar for the 43-in-1 platform. This is catalogue evidence about the platform, not proof that every included bit fits the complete tool pack whose small bits, handle and accessories must remain in assigned positions. For ratchet-case transit and pack-out verification, the useful next step is to match the documented interfaces, short and extended bit formats, handle modes and case organization to a buyer-supplied fastener map and access envelope.
The catalogue record provides a stable first-party reference for sample planning. It does not create a certification, universal compatibility statement, test result or customer outcome. The buyer should identify the actual profiles used most often, decide whether long bits or mixed interfaces are necessary, and confirm that the chosen case makes those items easy to identify. XOENAEN can then evaluate ratchet-case transit and pack-out verification against a defined configuration rather than a generic “complete set” request.
What should a buyer include in an inquiry about ratchet-case transit and pack-out verification?
The inquiry should describe approving a retail case, inner pack and export carton before ratchet-set production, attach photographs or drawings of the access area and list every representative screw profile, size and working depth. Include expected order quantity, target market, case and marking preferences, manual languages, packaging route and the required sample date. For ratchet-case transit and pack-out verification, define route, orientation, sample quantity, inspection photographs and failure rules before the test. Commercial comparisons become meaningful only when every supplier answers the same joint and acceptance question.
For ratchet-case transit and pack-out verification, ask the sample report to distinguish observations from specifications. Observations include whether the bit seats squarely on the complete tool pack whose small bits, handle and accessories must remain in assigned positions, how the selector feels, whether accessories remain retained and what condition appears after representative use. Specifications include the approved BOM, bit map, materials, dimensions, packaging revision and the acceptance rule “all items remain identifiable and undamaged with the case, labels and carton meeting the written approval rule.” Keeping those categories separate prevents one demonstration from becoming an unsupported lifetime or compatibility promise for ratchet screwdriver case transit test.
How should QC verify ratchet-case transit and pack-out verification?
QC for ratchet-case transit and pack-out verification starts with identity: lot, model, bit profile, interface, working length, case position and document revision. It then checks function using an agreed fixture or representative screw, with a method that states sample quantity, sequence, observation point and failure definition. Measurement equipment used for a numerical claim needs an appropriate calibration and traceability plan; visual fit still needs a named reference and acceptance photograph.
The release record should show whether all items remain identifiable and undamaged with the case, labels and carton meeting the written approval rule. It should also record scratches, recess damage, selector anomalies, loose holders, missing accessories, incorrect labels and packaging movement as separate defect types. A count of parts alone cannot verify identity or function. If a component, source, finish or instruction changes, review the risk to ratchet-case transit and pack-out verification and repeat affected checks before the revised lot is released.
What evidence and limits support this ratchet-case transit and pack-out verification guide?
This guide combines the distinct customer question, the current XOENAEN 43-in-1 ratchet screwdriver set catalogue record, a task-level failure analysis and the linked official guidance. It does not claim a third-party certification, customer result, universal repair permission, guaranteed fastener removal or unlisted torque rating. The product or equipment maker remains responsible for its service instructions, and representative hardware remains the approval basis for ratchet-case transit and pack-out verification.
The methodology traces each recommendation to an observable point: safe state, recess identification, installed-bit fit, work support, alignment, ratchet response, stop signal and post-work acceptance. Photographs, sample identifiers, drawings, test conditions, revision history and deviations should stay with the decision. That evidence lets another technician, engineer or buyer review ratchet-case transit and pack-out verification without depending on anonymous experience or marketing superlatives.
Method comparison for ratchet-case transit and pack-out verification
| Method | Useful condition | Control question |
|---|---|---|
| case-only shake screening | Direct option for approving a retail case, inner pack and export carton before ratchet-set production | Does it remain square on the complete tool pack whose small bits, handle and accessories must remain in assigned positions? |
| documented complete-pack transit simulation | Alternative when the direct option falls outside its boundary | Which additional risk and approval step does it introduce? |
| Stop and escalate | Unknown, damaged or unsafe joint condition | Who owns the approved next procedure for ratchet-case transit and pack-out verification? |
- Define the exact customer question: How should a buyer test whether bits stay organized during shipping?
- Photograph and identify the representative fastener: the complete tool pack whose small bits, handle and accessories must remain in assigned positions
- Record the access, interface and material controls: case latch, insert retention, accessory mass, retail orientation, inner pack, carton and test method
- Approve a stop rule that prevents: bits migrate into the mechanism, the latch opens or hidden case scuffing is accepted without a criterion
- Verify the platform against XOENAEN 43-in-1 ratchet screwdriver set rather than accessory count alone
- Retain a dated sample, bit map, packaging revision and acceptance record for ratchet-case transit and pack-out verification
- XOENAEN 43-in-1 ratchet screwdriver set →
- Related ratchet guide: service-data-led ratchet assortment planning →
- Next ratchet guide: ratchet-mechanism endurance test planning →
- Application planning resources →
- XOENAEN OEM and ODM process →
- Manufacturing and quality control →
- Read the related ratchet-driver-coffee-machine-service-panels guide →
- How XOENAEN presents quality evidence →
How should a buyer test whether bits stay organized during shipping?
The direct answer is to use the ratchet only after the fastener, access and work boundary for ratchet-case transit and pack-out verification have been verified. Test the saleable pack through the agreed distribution sequence, then open it in a controlled orientation and record movement, damage and label readability. The tool does not replace the equipment maker's procedure, an isolation step, a specified torque tool or specialist remediation when the joint falls outside that boundary.
Which bit and handle setup fits ratchet-case transit and pack-out verification?
Use the setup that reaches the complete tool pack whose small bits, handle and accessories must remain in assigned positions with full recess engagement and a square hand path. For ratchet-case transit and pack-out verification, compare the exact profile, H4 or H6.35 interface where relevant, working length, holder clearance and swing arc on representative hardware; accessory count alone does not prove fit.
What stop signal matters most during ratchet-case transit and pack-out verification?
Stop as soon as the bit climbs, the joint shifts, resistance changes unexpectedly or any part of bits migrate into the mechanism, the latch opens or hidden case scuffing is accepted without a criterion becomes visible. Preserve the condition, remove hand load and determine whether the bit, screw, thread, fixture or documented procedure must change before ratchet-case transit and pack-out verification continues.
How should a buyer test ratchet-case transit and pack-out verification before purchase?
Test representative fasteners through the complete preparation, removal, reinstallation and acceptance sequence for ratchet-case transit and pack-out verification. Record profile fit, reach, selector behavior, retention, clearance, operator visibility and all items remain identifiable and undamaged with the case, labels and carton meeting the written approval rule; an unloaded clicking demonstration cannot answer the customer's application question.
Which XOENAEN catalogue platform supports evaluation of ratchet-case transit and pack-out verification?
XOENAEN 43-in-1 ratchet screwdriver set is the current catalogue reference selected for this ratchet-case transit and pack-out verification guide. It is a starting platform, not a universal compatibility claim; the buyer should compare its documented bit map and handle format with actual hardware and approve a representative sample before release.
What must an OEM brief state for ratchet-case transit and pack-out verification?
State the target joint, screw profiles and sizes, access envelope, required interfaces, long-bit needs, case layout, manual markets, expected volume, sample plan and acceptance rule for ratchet-case transit and pack-out verification. define route, orientation, sample quantity, inspection photographs and failure rules before the test. This makes the quotation and approval record specific rather than promotional.