Use a ratchet screwdriver for stick-vacuum floor-head soleplate screws only within this boundary: removing a maker-approved brush guard or soleplate after the cordless vacuum is switched off and its battery is handled exactly as the product instructions require; motor, battery-cell and live charging work are excluded. Match the exact recess, support the work and stop at packed debris prevents full seating, a boss rotates, a tab remains captured.
ratchet driver for stick vacuum floor head screws
ratchet driver for stick vacuum floor head screws describes selecting and using a compatible manual ratchet configuration for stick-vacuum floor-head soleplate screws after the fastener, access, work boundary and final inspection have been documented. It is not a universal compatibility, torque, certification or repair claim.
Use a ratchet screwdriver for stick-vacuum floor-head soleplate screws only within this boundary: removing a maker-approved brush guard or soleplate after the cordless vacuum is switched off and its battery is handled exactly as the product instructions require; motor, battery-cell and live charging work are excluded. Match the exact recess, support the work and stop at packed debris prevents full seating, a boss rotates, a tab remains captured. This guide answers one narrow customer question and does not turn a matching bit into permission for unrelated repair work.
The useful buying decision begins with the actual several similar-looking screws positioned near wheels, brush bearings, belt covers, sensors and flexible plastic tabs. A ratchet saves repeated wrist rotation where access is constrained, but it does not choose a fastener, repair damaged receiving material or establish a safe service state. For stick-vacuum floor-head soleplate screws, the application boundary, screw map and final observable condition should be written before a handle is compared. That approach gives a US or European buyer something more reliable than a broad “universal repair kit” claim and makes an OEM sample easier to evaluate on representative work.
Is a ratchet screwdriver the right tool for stick-vacuum floor-head soleplate screws?
It is the right tool only when the screw is compatible, the work can be supported and the return stroke stays square. Here the permitted scope is removing a maker-approved brush guard or soleplate after the cordless vacuum is switched off and its battery is handled exactly as the product instructions require; motor, battery-cell and live charging work are excluded. That wording matters because the surrounding product or structure may contain hazards and functions that have nothing to do with turning a screw. A compact ratchet can improve access, yet the smallest workable movement should begin only after the maker's procedure, work condition and receiving material are understood. If any one of those facts is missing, the sensible decision is to pause and obtain it rather than treating the handle as a troubleshooting device.
Which bit geometry and working length fit this particular fastener?
Start with several similar-looking screws positioned near wheels, brush bearings, belt covers, sensors and flexible plastic tabs. Clean the head by a material-compatible method, inspect the profile under direct light and compare a fresh bit without load. The key access detail is that deep wells beside wheels often need a long working tip, but the holder must not scrape the well or push the head sideways. Measure recess depth, holder diameter and the usable return arc as one system. A long bit that reaches but rubs the access wall is not a controlled fit; neither is a short bit extended by several loose adapters. Record the selected profile, interface and working length beside a photograph so replacement bits and later production samples can be checked against the same evidence instead of memory.
How should the work be prepared before the first loaded stroke?
For this job, clear hair and dust with the approved method, map screw length by location, secure the brush roll, and keep loose metal bits away from exposed electrical contacts. Put removed hardware into a divided tray in the order it leaves the assembly, and note whether each item is captive, shouldered or paired with a washer. Good lighting and a stable support are more valuable than additional leverage. Preparation should also identify the stop boundary: a safe state, an intact receiver and a clear path for the bit. When those conditions are visible before disassembly, the operator can notice a real change instead of discovering at reassembly that a cable, gasket, edge or panel was already out of position.
Why does a screw-location map matter even when the heads look alike?
Small differences in length, shoulder diameter, finish or washer order can serve different purposes. A longer screw returned to a shallow location can damage a hidden surface, while a short screw in a deeper receiver may appear seated without providing the intended engagement. Build a simple location map for stick-vacuum floor-head soleplate screws: one photograph, numbered positions and matching tray compartments are enough for many jobs. Add notes for any screw that releases a foot, clip, spacer or moving part. The map is also useful commercial evidence because it tells an OEM buyer which profiles and working lengths are actually needed, rather than rewarding a case merely for its printed piece count.
What sequence keeps the assembly aligned while ratcheting?
The controlled sequence is to release the soleplate in its documented order, keep bushings and end caps with the correct side, and hand-start every mapped screw before using short ratchet strokes. Separate free-running travel from final seating. Ratchet mode is useful while the screw moves smoothly; lock or straight-driver mode can give clearer feedback as parts make contact. Do not use one screw to drag distant holes, flatten a caught panel or overcome a loaded mechanism. Work across paired fasteners in small stages so alignment remains observable. If a manufacturer specifies an order, measured torque or special tool, that instruction replaces handle feel. The operator should be able to explain why each next screw is being moved and what condition will stop the motion.
What warning signs mean the ratchet should stop immediately?
Stop when you see or feel packed debris prevents full seating, a boss rotates, a tab remains captured, a wire enters the seam or a long screw approaches a shallow location. A ratchet is efficient at repeating a motion, which means it can repeat damage just as efficiently as useful free travel. Remove the load, preserve the remaining recess geometry and identify whether the problem is profile fit, debris, alignment, receiver damage or an excluded part of the job. Increasing hand force is not an inspection method. Photograph the condition before repair or replacement so a supplier, service team or customer can distinguish an application mismatch from a worn bit, damaged material or incorrect previous assembly.
When would a fixed driver or specialist method be better?
a fixed precision driver is preferable for the final plastic-thread feel; belt, motor, sensor or battery faults follow the model-specific service route. Compare options at the same representative access point using the same fresh bit and stopping rule. The best method is the one that remains axial, protects the surrounding surface and leaves the final condition visible. A fixed driver often wins at the last fraction of a turn; a ratchet often wins during smooth repeated travel in limited swing space. A powered driver is not automatically faster when screw mapping, fragile receivers or finish protection dominate the job. Specialist work remains specialist work even when a general-purpose bit physically enters the fastener.
How should reassembly be checked before the item returns to use?
The acceptance condition for this article is specific: the soleplate sits flush, wheels and brush parts move as specified, no cable is trapped, and the manufacturer-directed post-cleaning check is completed. Check every mapped location, visible seam, moving part and protected surface before cleanup. This is not proof of electrical safety, structural capacity or compliance beyond the stated boundary. It is a documented fastener and reassembly check. If the item maker requires a functional, stability or return-to-service procedure, complete that procedure after the enclosure or furniture is fully restored. Clean the chosen bit and holder before storage, and quarantine any worn tip so the next user does not inherit an unidentified fit problem.
Which XOENAEN ratchet platform should a buyer shortlist?
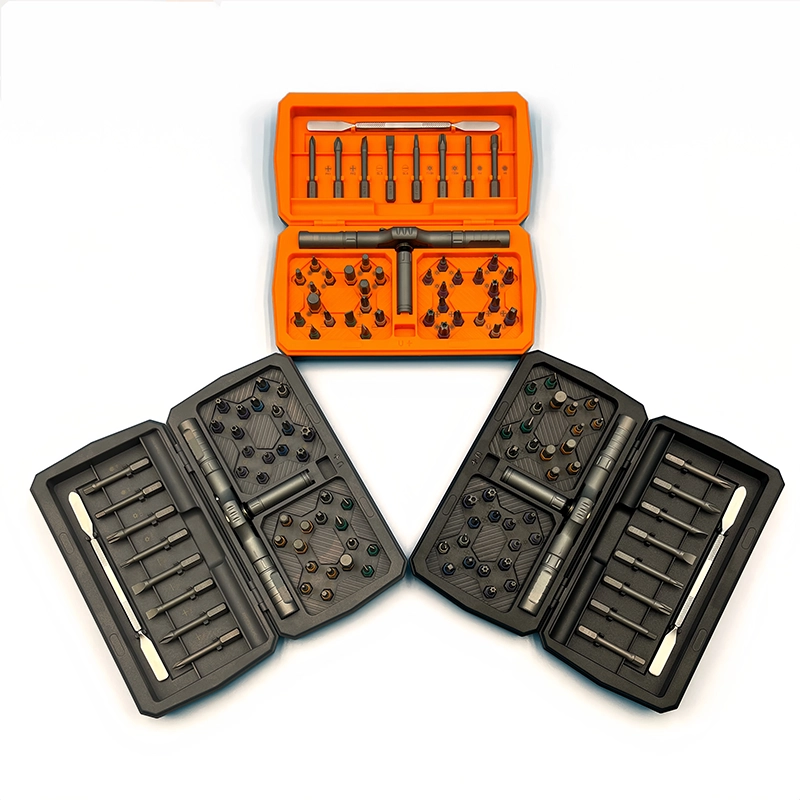
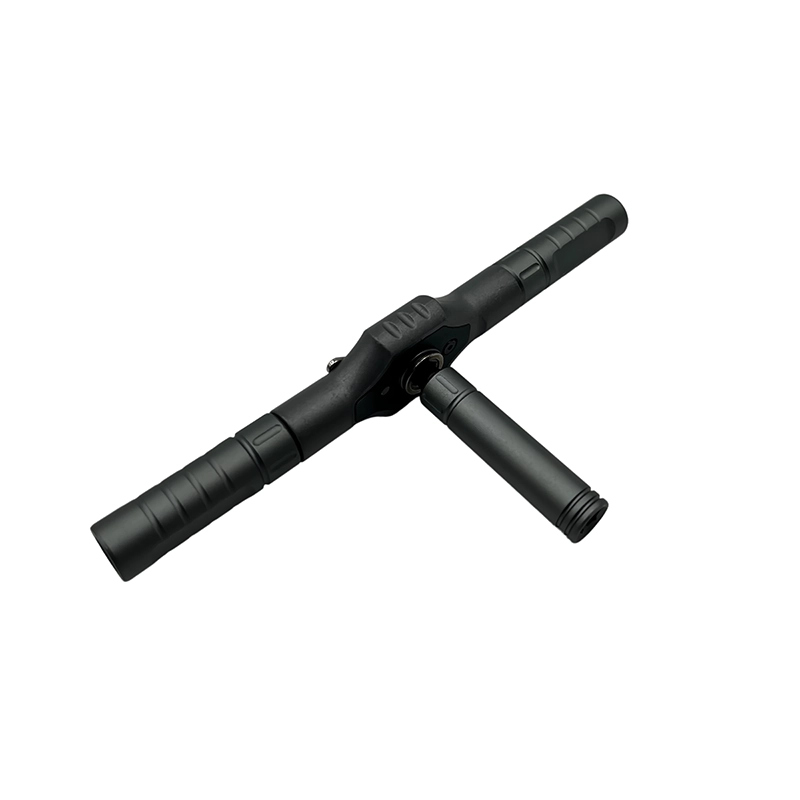
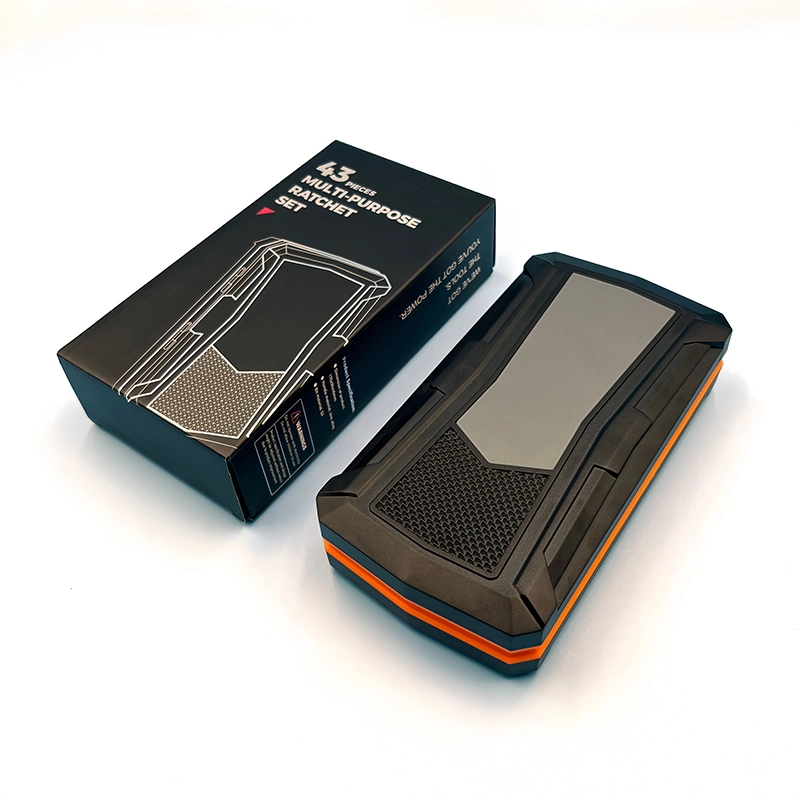
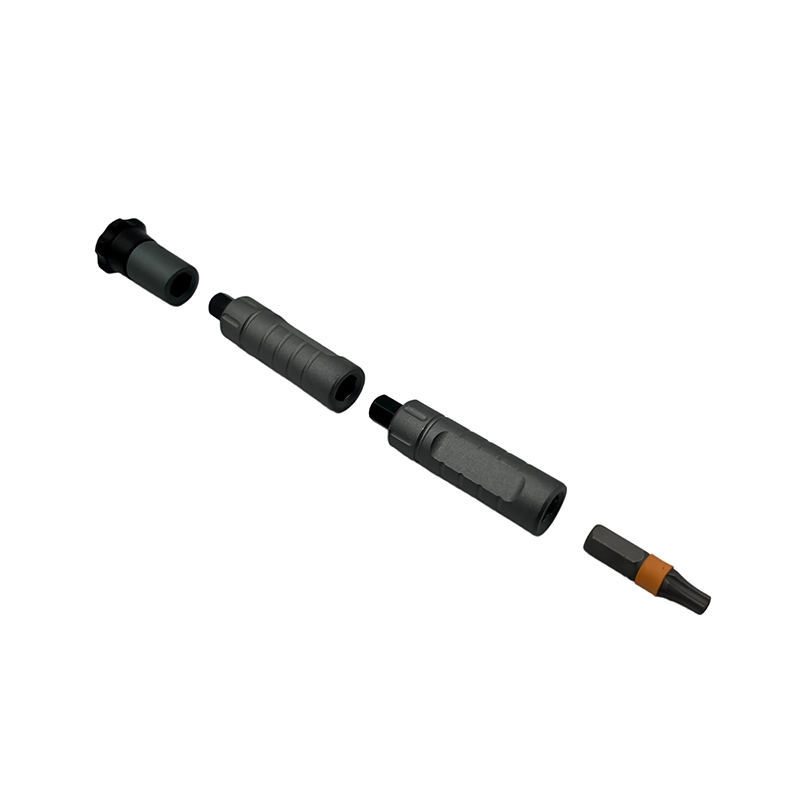
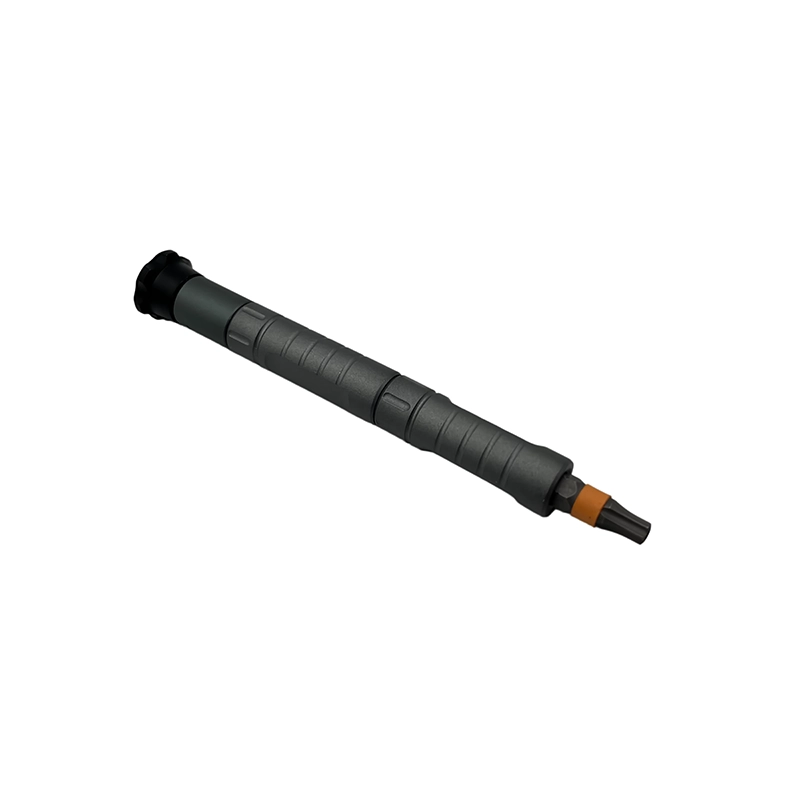
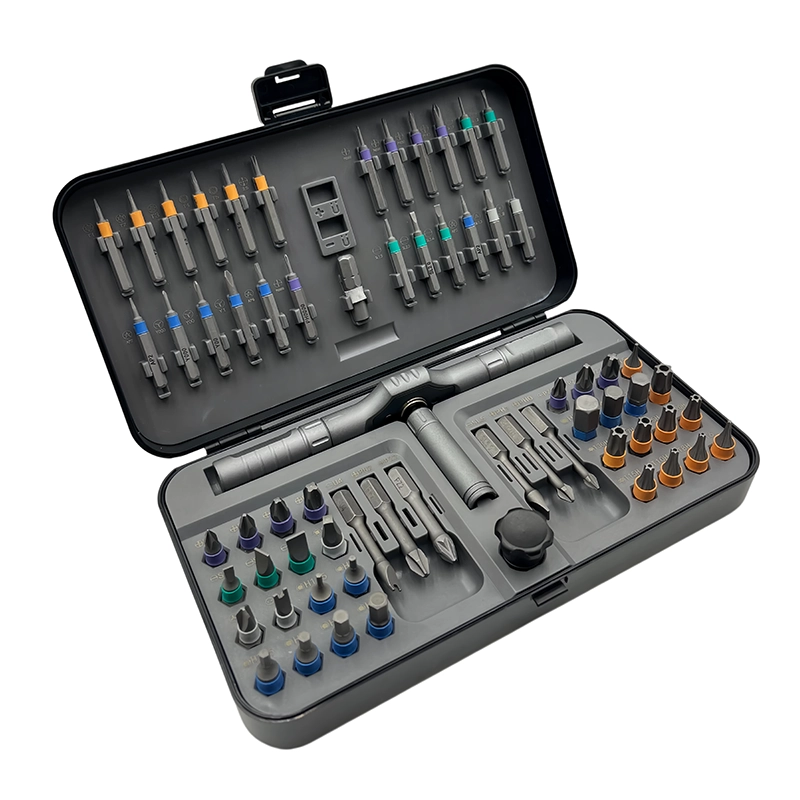
The current XOENAEN catalogue lists H6.35 and H4 bit interfaces, 32 mm and 40 mm long-bit formats, short precision bits, a magnetizer and a handle that can convert to a straight-driver format for the 66-in-1 platform. This is a first-party catalogue description, not a claim that the platform is universally compatible with stick-vacuum floor-head soleplate screws. Shortlisting still depends on the real screw profile, working depth, holder clearance and representative sample. Buyers should compare the physical bit map rather than the product name alone. They should also confirm selector labeling, case retention, replacement-bit identification and instructions for the target market. A useful sample review records what fit, what did not fit and which exclusion prevented the tool from being used on a particular part.
What evidence belongs in a Western-market OEM or wholesale brief?
For this application, request an actual contaminated floor head, screw-length map, deep-well dimensions, retention check and photographs showing the accepted seam and brush clearance. Add target countries, language set, sales channel, expected quantity, packaging format and the intended user group. Claims should remain tied to the approved sample and current artwork revision. Do not convert a successful fit check into an unsupported torque, durability, certification or repair-performance promise. The strongest inquiry gives XOENAEN a representative screw or product, photographs of the access envelope and a measurable acceptance condition. That evidence makes platform selection, quotation, packaging review and later quality control more efficient without pretending that every household product uses the same hardware.
What should a representative bench trial reproduce for stick-vacuum floor-head soleplate screws?
Build the trial around the awkward fact that deep wells beside wheels often need a long working tip, but the holder must not scrape the well or push the head sideways. Use the real several similar-looking screws positioned near wheels, brush bearings, belt covers, sensors and flexible plastic tabs, not a convenient substitute from a workshop drawer. Reproduce the supported starting condition by requiring the operator to clear hair and dust with the approved method, map screw length by location, secure the brush roll, and keep loose metal bits away from exposed electrical contacts. The trial record should name the product revision, fastener position, selected bit, working length and handle mode, then show whether the operator can release the soleplate in its documented order, keep bushings and end caps with the correct side, and hand-start every mapped screw before using short ratchet strokes. A useful photograph captures the tip axis and nearby clearance while a second image shows the completed joint. This evidence answers a practical sourcing question—whether the configuration is controllable at this access point—without stretching the result into an unmeasured strength or service-life claim.
How should this specific task be handed over to another operator?
Write a one-page handover for stick-vacuum floor-head soleplate screws in the order the next operator will use it. Begin with the boundary that limits the work to removing a maker-approved brush guard or soleplate after the cordless vacuum is switched off and its battery is handled exactly as the product instructions require; motor, battery-cell and live charging work are excluded. Follow with the hardware map and the warning that work ends at packed debris prevents full seating, a boss rotates, a tab remains captured, a wire enters the seam or a long screw approaches a shallow location. Include the approved alternative: a fixed precision driver is preferable for the final plastic-thread feel; belt, motor, sensor or battery faults follow the model-specific service route. The final line should state the observable release condition—the soleplate sits flush, wheels and brush parts move as specified, no cable is trapped, and the manufacturer-directed post-cleaning check is completed. Keep the dated sheet with an actual contaminated floor head, screw-length map, deep-well dimensions, retention check and photographs showing the accepted seam and brush clearance. This task-level handover is more useful than a generic safe-use paragraph because it identifies the actual decision, excluded work, physical evidence and escalation route that apply to this one repair, assembly or maintenance question.
What field observation is unique to stick-vacuum floor-head soleplate screws?
A floor head is a small mechanical map: wheel axles, brush end caps and soleplate screws may occupy the same visual field while serving unrelated functions. Lay the head on white paper before opening it; dark screws, clips and hair are easier to distinguish there. Note which wheel remains loaded and which brush end carries a keyed insert. If the plate releases on one side but not the other, look for a documented tab instead of twisting the free corner. When the work is complete, rotate each wheel and brush by hand before reconnecting the vacuum so a trapped strand or misplaced cap is found without motor power.
Method choice for stick-vacuum floor-head soleplate screws
| Method | Best-fit stage | Useful advantage | Mandatory check |
|---|---|---|---|
| Compact ratchet screwdriver | Restricted swing after a verified hand start | Repeated manual free travel | The bit remains square at stick-vacuum floor-head soleplate screws |
| Fixed or locked hand driver | Initial thread start and final seating | Direct feedback | The receiving material remains sound |
| Maker-specified or specialist method | Excluded, rated or measured work | Task-specific control | Follow the documented procedure and equipment |
- Map the real screw profiles and locations used at stick-vacuum floor-head soleplate screws.
- Measure working depth, holder clearance and the full ratchet return arc.
- Document safe state, work support, excluded systems and the maker instruction.
- Approve stop signals for recess, receiver, surface and alignment damage.
- Compare a representative application with the current XOENAEN 66-in-1 ratchet screwdriver set configuration.
- Keep the physical sample, bit map, case, artwork and inspection record on one revision.
- View the XOENAEN 66-in-1 ratchet screwdriver set →
- Previous guide: How to Check Air-Fryer Basket-Handle Screws with a Ratchet →
- Next guide: Should You Tighten Space-Heater Foot and Base Screws? →
- Plan an XOENAEN OEM / ODM ratchet set →
- Review manufacturing and quality support →
- Read the XOENAEN buyer FAQ →
- Read the related ratchet-screwdriver-lift-top-coffee-table-linkage-guards guide →
- How XOENAEN presents quality evidence →
Which ratchet setup helps remove a stick-vacuum floor-head soleplate without mixing its screws?
Use the ratchet only after the work is inside this stated boundary: removing a maker-approved brush guard or soleplate after the cordless vacuum is switched off and its battery is handled exactly as the product instructions require; motor, battery-cell and live charging work are excluded. The immediate acceptance check is that the soleplate sits flush, wheels and brush parts move as specified, no cable is trapped, and the manufacturer-directed post-cleaning check is completed. If either condition is uncertain, pause before applying leverage.
What should be photographed before working on stick-vacuum floor-head soleplate screws?
Photograph the complete assembly, every fastener location, the visible hardware stack and the initial alignment. For this job, preparation also means that you clear hair and dust with the approved method, map screw length by location, secure the brush roll, and keep loose metal bits away from exposed electrical contacts. Those records prevent similar-looking parts from being interchanged.
Which access problem matters most at stick-vacuum floor-head soleplate screws?
The distinct constraint is that deep wells beside wheels often need a long working tip, but the holder must not scrape the well or push the head sideways. Check the full return stroke with an unloaded tool, not just whether a bit reaches while stationary. Reject a setup that rubs, rocks or depends on several uncontrolled adapters.
When must a user stop ratcheting stick-vacuum floor-head soleplate screws?
Stop at packed debris prevents full seating, a boss rotates, a tab remains captured, a wire enters the seam or a long screw approaches a shallow location. Preserve the screw recess and surrounding material, document the condition and follow the approved repair or replacement route instead of adding hand force.
How is successful reassembly of stick-vacuum floor-head soleplate screws verified?
The narrow fastener result is acceptable when the soleplate sits flush, wheels and brush parts move as specified, no cable is trapped, and the manufacturer-directed post-cleaning check is completed. Complete any additional maker-required functional, stability or return-to-service procedure before normal use.
What should an OEM buyer send for a stick-vacuum floor-head soleplate screws tool inquiry?
Send an actual contaminated floor head, screw-length map, deep-well dimensions, retention check and photographs showing the accepted seam and brush clearance. Include destination markets, users, quantities, language and packaging needs so the sample and claim review stay tied to the real application.