Use a long curvature reference and cross the repair zone with overlapping passes wider than the defect. Support the broad convex shell between edges, vents and raised details with an internal helmet form or rib support under the work zone. Control backing compliance, overlap, pass direction and inspection lighting. Stop if light bands become wavy, an edge loses definition or the shell pumps under pressure.
reciprocating sanding large 3D printed cosplay curves
reciprocating sanding large 3D printed cosplay curves is a controlled process for leveling filler and layer texture on a helmet or armor shell that protects silhouette, panel breaks and consistent shell thickness and releases the part only when the approved contour template and grazing light cross the area without a hollow or flat.
Concentrating on the visible filler line produces a trench; the correction must be judged as part of the whole curve. This guide treats reciprocating sanding large 3D printed cosplay curves as a specific workshop decision around leveling filler and layer texture on a helmet or armor shell. It does not assume that one accessory, speed or motion is safe for every polymer, resin, wood or metal. The actual part, its drawing and the customer’s acceptance reference remain the final authority.
How should broad printed cosplay curves be sanded without making waves?
Use a long curvature reference and cross the repair zone with overlapping passes wider than the defect. Begin by cleaning and photographing the broad convex shell between edges, vents and raised details. Mark silhouette, panel breaks and consistent shell thickness as a no-change reference, then test a single short intervention in an accessible zone. For reciprocating sanding large 3D printed cosplay curves, clean the work again before evaluating it; dust, loaded media and temporary heat can disguise both scratches and missing material.
What makes this geometry different from a general sanding job?
The job is leveling filler and layer texture on a helmet or armor shell, and the working surface is the broad convex shell between edges, vents and raised details. Those details determine where force travels and which mistake matters. A generic instruction such as use light pressure cannot protect silhouette, panel breaks and consistent shell thickness. A usable work instruction instead names the support, approach direction, maximum worked zone and the inspection that must follow every short pass.
Which motion should be used for reciprocating sanding large 3D printed cosplay curves?
The proposed motion is overlapping reciprocating passes across a supported curve. a flexible longboard shaped to the shell offers a useful reference because the operator can feel initial contact, while a compliant reciprocating pad moved continuously over a supported area may improve access or consistency after the contact area is understood. Compare the two on equivalent defects rather than assuming powered work is automatically faster once cleanup, inspection and rejected parts are counted.
How should the workpiece be supported before contact?
Use an internal helmet form or rib support under the work zone. Support should sit close enough to the worked zone to prevent vibration but must not preload the feature being checked. Confirm that clamps, fingers and cables remain outside the tool path. For reciprocating sanding large 3D printed cosplay curves, the fixture is part of the approved method: changing it can change vibration, apparent fit and how much material the media removes.
Which variables deserve a first-piece record?
Record backing compliance, overlap, pass direction and inspection lighting, together with the part material, print orientation or stock form, accessory identity, clean starting condition and contact sequence. Photograph the setup from an angle that shows the protected feature. A buyer comparing kits should ask whether controls can be repeated by another trained operator, not only whether the demonstration sample looked acceptable once.
When should powered finishing stop immediately?
Stop when light bands become wavy, an edge loses definition or the shell pumps under pressure. Isolate the tool, remove debris and compare the area with its starting image before making another decision. Added speed or pressure cannot restore geometry already removed. The stop signal belongs on the bench instruction and, where relevant, in the product manual because it is more actionable than a broad warning to avoid damage.
How do the hand and powered methods compare?
a flexible longboard shaped to the shell usually provides better tactile feedback and a simple dimensional reference. By contrast, a compliant reciprocating pad moved continuously over a supported area can help with reach or repeated short strokes. For reciprocating sanding large 3D printed cosplay curves, compare edge condition, heat, debris, setup time, inspection time and consistency across at least two representative samples. Keep both options available when the feature changes across the job.
What inspection closes the job?
Use contour templates, symmetrical reference points and grazing-light photographs. The acceptance statement is explicit: the approved contour template and grazing light cross the area without a hollow or flat. Perform the check on a clean part returned to a stable temperature. Cosmetic improvement is not enough where a fit, seal, motion or datum is involved. If the required reference is unavailable, hold the part for review rather than polishing until the original condition can no longer be seen.
Which kit details matter to a European or North American buyer?
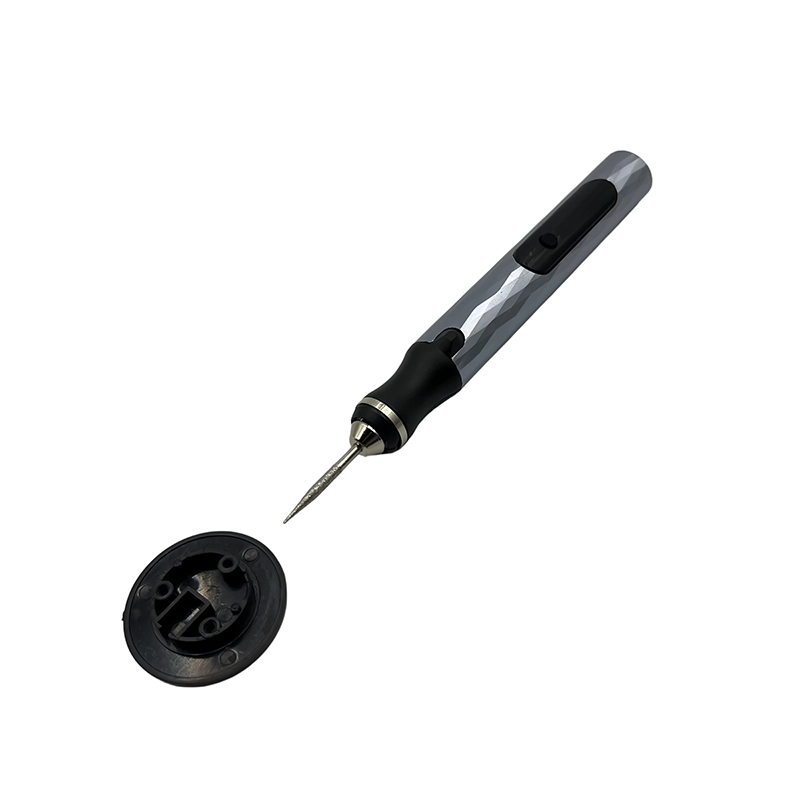
The 106 cordless precision rotary tool is a current XOENAEN catalogue reference, not proof of universal suitability for reciprocating sanding large 3D printed cosplay curves. Review the exact control layout, compatible shank or pad interface, included media identity, charging configuration, case labeling and availability of replacement consumables. Market documentation and electrical review must match the final sellable configuration rather than a development photograph.
What belongs in the OEM or wholesale project brief?
Provide shell material, filler system, curvature sections, protected details and final paint build. Add target markets, expected quantity, packaging language, accessory map, replacement pack, visual limits and sample timing. The brief should identify who approves the first article and which workpiece proves the claim. This keeps sales copy, instructions and quality checks aligned with evidence instead of expanding a single workshop result into a universal promise.
How can the method sound like a real shop instruction?
Write the sequence with observable verbs: inspect, mark, support, install, make one pass, stop, clean and measure. Name light bands become wavy, an edge loses definition or the shell pumps under pressure as the rejection trigger and the approved contour template and grazing light cross the area without a hollow or flat as the release condition. Retain one accepted sample or image set. Reapprove the method after a material, accessory, fixture or product revision rather than relying on memory from the original trial.
For the final record, link reciprocating sanding large 3D printed cosplay curves to the exact part revision, 106 cordless precision rotary tool configuration, accessory identity and inspection reference. Concentrating on the visible filler line produces a trench; the correction must be judged as part of the whole curve. A concise record of what was protected, what was changed and what proved completion is more useful to future operators—and to search readers—than generic claims about effortless professional results.
a flexible longboard shaped to the shell compared with a compliant reciprocating pad moved continuously over a supported area
| Method | Useful when | Main control |
|---|---|---|
| a flexible longboard shaped to the shell | Tactile feedback or a hard reference is needed | contour templates, symmetrical reference points and grazing-light photographs |
| a compliant reciprocating pad moved continuously over a supported area | Access or repeated short strokes matter | backing compliance, overlap, pass direction and inspection lighting |
- Define the exact task: leveling filler and layer texture on a helmet or armor shell
- Protect silhouette, panel breaks and consistent shell thickness
- Use an internal helmet form or rib support under the work zone
- Control backing compliance, overlap, pass direction and inspection lighting
- Stop if light bands become wavy, an edge loses definition or the shell pumps under pressure
- Approve only when the approved contour template and grazing light cross the area without a hollow or flat
- 106 cordless precision rotary tool →
- Cutting Thin Brass Tube for Models With a Rotary Tool →
- Finishing Wood-Filled PLA Without Pulling Surface Fibers →
- Opening a 3D Printed Zip-Tie Slot Without Cutting the Wall →
- Application planning →
- OEM and ODM development →
- Continue with the blend-bonded-seam-split-3d-printed-model topic →
- XOENAEN editorial policy →
What is the first measurement for reciprocating sanding large 3D printed cosplay curves?
Start with contour templates, symmetrical reference points and grazing-light photographs and record the untouched condition of the broad convex shell between edges, vents and raised details. That establishes whether the problem is real, where it is located and which feature must remain unchanged before any abrasive or cutting accessory is selected.
Why is overlapping reciprocating passes across a supported curve considered for this job?
That motion can match the access and contact pattern of leveling filler and layer texture on a helmet or armor shell, but it still requires an internal helmet form or rib support under the work zone. The choice is provisional until a representative sample proves that silhouette, panel breaks and consistent shell thickness remains intact.
Which visible warning ends reciprocating sanding large 3D printed cosplay curves?
End the pass when light bands become wavy, an edge loses definition or the shell pumps under pressure. Clean and inspect before deciding whether a different hand method, accessory or fixture is needed; continuing with more force would hide the cause and can remove functional geometry.
Does the rotary-106 platform guarantee reciprocating sanding large 3D printed cosplay curves?
No. The rotary-106 is a real XOENAEN catalogue reference for discussing reciprocating sanding large 3D printed cosplay curves, not a universal application claim. Suitability depends on the broad convex shell between edges, vents and raised details, the selected accessory, workholding, instruction and the acceptance sample supplied for this exact project.
What proves a sample passes reciprocating sanding large 3D printed cosplay curves?
The cleaned, stable part must meet this condition: the approved contour template and grazing light cross the area without a hollow or flat. Use the stated gauge, mating item, motion test, lighting reference or dimensional check rather than approving the part from a general impression that it looks smoother.
What should the buyer send for a reciprocating sanding large 3D printed cosplay curves quotation?
Provide shell material, filler system, curvature sections, protected details and final paint build. Also state volume, market, required documentation, preferred pack-out and the first-article sample that will be used to approve the proposed rotary or reciprocating configuration.