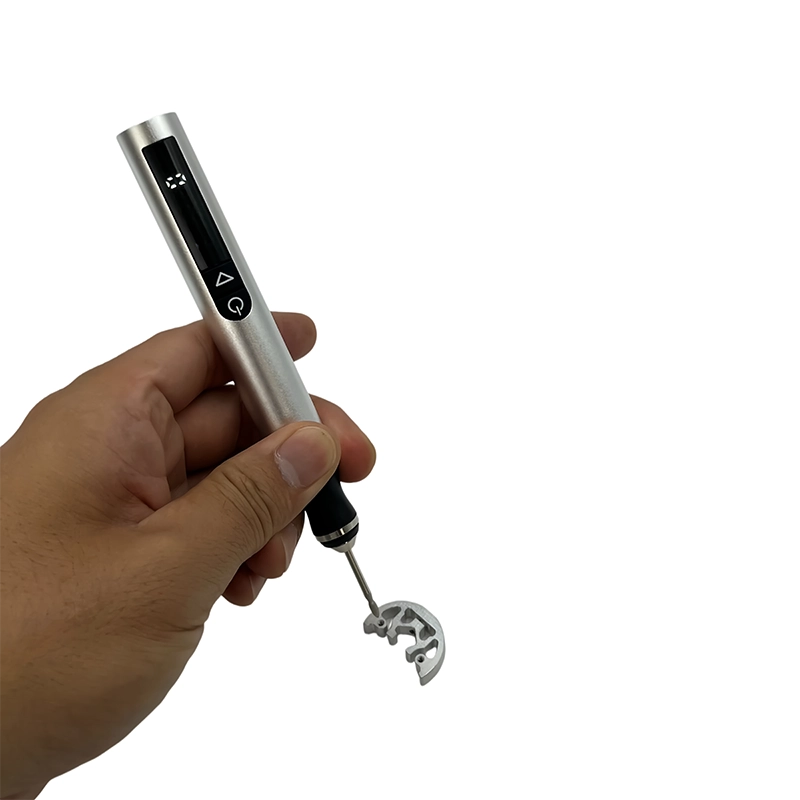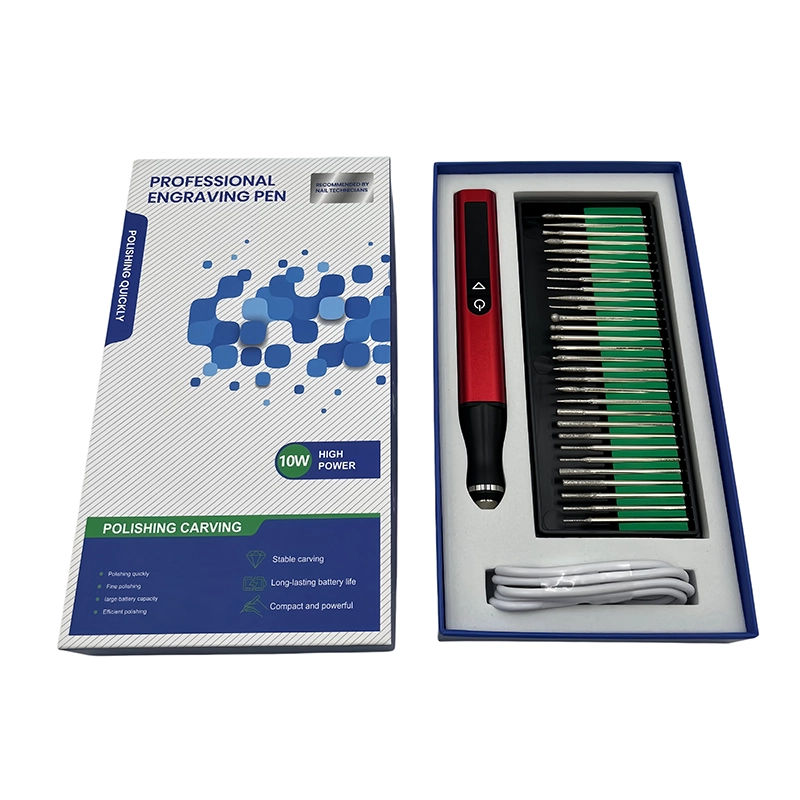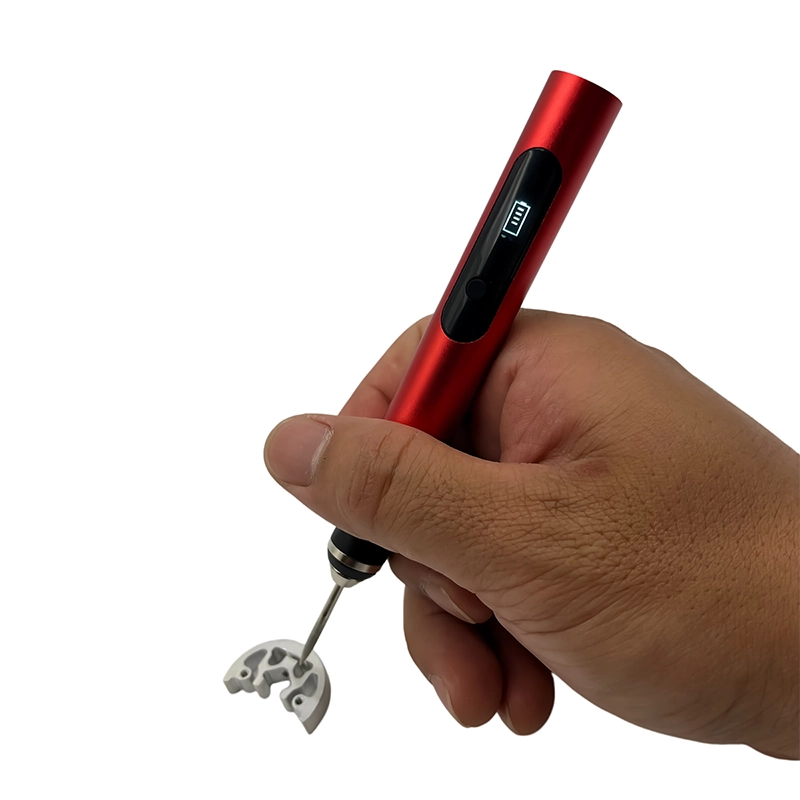
For blending support marks and seams beside visible or assembly-critical printed edges, choose a compact rotary and hand-sanding tool kit around edge protection, moving contact and measured stop points. Confirm fit, access, operator control and the complete bit or accessory map on a representative sample before approving a wholesale, OEM or DIY configuration.
sanding 3D print edges with rotary tool
sanding 3D print edges with rotary tool means selecting a tool set around the real fastener, surface, access and inspection requirement instead of choosing by piece count alone.
Sanding 3D Print Edges with a Rotary Tool Without Rounding Them starts with the work, not the headline piece count. For blending support marks and seams beside visible or assembly-critical printed edges, the useful question is whether a compact rotary and hand-sanding tool kit gives the operator the access, control and bit or accessory fit needed to complete the job without creating a second repair. The product should be easy to identify, easy to inspect and easy to return to its case when the work is done.
For sanding 3D print edges with rotary tool, the brief should translate edge protection, moving contact and measured stop points into an observable sample decision. Record the exact blending support marks and seams beside visible or assembly-critical printed edges, the surrounding material, access limit, expected repetition and pass condition before comparing features. add a no-sand boundary and edge gauge to the sample acceptance plan. That evidence gives a manufacturer, distributor or private-label buyer a configuration target instead of a generic request for more pieces.
How do you sand 3D print edges without rounding them?
Support the edge, approach the defect from the side and use a small moving contact instead of sweeping across the boundary. Start with the exact device, appliance, furniture part or printed feature whenever possible. A sample that looks close in a catalogue can behave differently when the screw is recessed, the housing is plastic, the panel is finished or the printed part has a thin wall. Confirm the fit before comparing colour, packaging or a larger accessory count.
Which bit, reach or accessory should be specified?
The selection should follow edge protection, moving contact and measured stop points. List the profiles, sizes, lengths or abrasive shapes that the user actually needs, then mark the pieces that are optional. For a product set, also record the interface, storage position, replacement plan and any speed or handling limits. This detail keeps a high piece count from hiding a gap in the real application.
What is the most common mistake in this workflow?
polishing a rounded edge until it looks smooth while the part no longer fits its mating component The remedy is usually a better start: clean the work area, seat the bit or accessory fully, keep the tool square, support the part and stop to inspect before the problem becomes irreversible. If a feature is safety-critical, load-bearing or outside the tool’s intended control, the correct decision may be a different tool, a controlled machining step or a reprint.
How should a repair or DIY user set up the work?
Set up blending support marks and seams beside visible or assembly-critical printed edges on a supported surface with direct light and a dedicated place for every removed fastener or used accessory. The operator should be able to observe edge protection, moving contact and measured stop points without changing grip or blocking the work. Because polishing a rounded edge until it looks smooth while the part no longer fits its mating component, begin with a reversible trial, inspect after the first controlled movement and keep the stopping point visible throughout the task.
How can a buyer validate the kit before ordering?
Validate sanding 3D print edges with rotary tool on a representative blending support marks and seams beside visible or assembly-critical printed edges. Record the profile or accessory identity, access, handling, condition before work and the result tied to support the edge, approach the defect from the side and use a small moving contact instead of sweeping across the boundary. Include the unsuccessful attempt or stop signal as evidence, because a sample that only records the successful pass cannot explain the limits another operator must follow.
The retained record for sanding 3D print edges with rotary tool should be short but specific: identify the workpiece, approved setup, acceptance view and any item that was replaced or rejected. For this task, add a no-sand boundary and edge gauge to the sample acceptance plan. A buyer can then compare samples on the same evidence and explain why the selected configuration fits this application without implying universal compatibility.
What should be included in an OEM or wholesale brief?
State the target market, user, application, order quantity and required launch timing. Add the product or platform reference, complete bit or accessory map, packaging format, label language, manual requirements, compliance documents and sample plan. add a no-sand boundary and edge gauge to the sample acceptance plan. Keep commercial and technical decisions together so the quotation reflects a real configuration rather than a generic photograph.
Final checklist
Before the next job, confirm the correct profile, clean contact surfaces, square alignment, protected no-touch areas, a visible stop condition and a final fit or appearance check. Record the model and replacement items when the kit is shared. These small habits make sanding 3D print edges with rotary tool useful for a service bench, a workshop or a DIY project instead of a tool case that looks complete but is hard to trust.
Choose the method by the real job
| Method | Best use | Main risk | Stop when |
|---|---|---|---|
| Hand sanding | Broad or edge-critical surface | Slow but tactile | The surface and fit pass inspection |
| Rotary | Local recess, hole or curve | Heat or excess removal | The local feature is corrected |
| Reciprocating | Accessible directional plane | Uneven stroke or edge drift | The scratch pattern is controlled |
- Confirm the actual blending support marks and seams beside visible or assembly-critical printed edges and the fastener, surface or feature involved.
- Check the complete bit or accessory map, interface, reach and storage position.
- Use representative samples and a repeatable inspection light, gauge or mating part.
- Write the stop condition that prevents polishing a rounded edge until it looks smooth while the part no longer fits its mating component.
- Include packaging, manual language, replacement items and target-market requirements in the brief.
- View the referenced 104 compact rotary tool →
- Related guide: Rotary Tool Finishing for PLA and PETG 3D Prints →
- Next application question: How to Polish Resin 3D Prints with a Small Rotary Tool →
- Review manufacturing and quality support →
- Explore OEM / ODM options →
- Read the related reciprocating-sanding-for-3d-printed-surfaces guide →
- Continue with the 3d-print-finishing-tool-kit-oem-buyers topic →
- XOENAEN editorial policy →
How do you sand 3D print edges without rounding them?
Support the edge, approach the defect from the side and use a small moving contact instead of sweeping across the boundary. Test the exact combination on a representative sample before treating it as a universal setting.
Which checks matter before buying sanding 3D print edges with rotary tool?
Check edge protection, moving contact and measured stop points, the complete bit or accessory map, storage, documentation and the sample acceptance method for blending support marks and seams beside visible or assembly-critical printed edges. Piece count matters only when the included items cover that verified workflow.
When should work stop during sanding 3D print edges with rotary tool?
Stop when the setup begins to reproduce this known failure: polishing a rounded edge until it looks smooth while the part no longer fits its mating component Preserve the fastener, surface or printed feature, then correct fit, support, alignment or method before continuing.
What evidence should an OEM buyer send for sanding 3D print edges with rotary tool?
Send the target market, quantity, representative photos or samples, the bit or accessory map, packaging language and the acceptance view. add a no-sand boundary and edge gauge to the sample acceptance plan. The supplier should be able to trace the proposed configuration back to those inputs.