Product knowledge

Useful decisions. Better tool projects.

Practical product, OEM/ODM and quality guidance grounded in the tools and project work shown across this site.

Precision screwdriver supplier evaluation scorecard reviewed beside product and quality recordsSeptember 1, 2026How Should Buyers Score Precision Screwdriver Suppliers?Read article
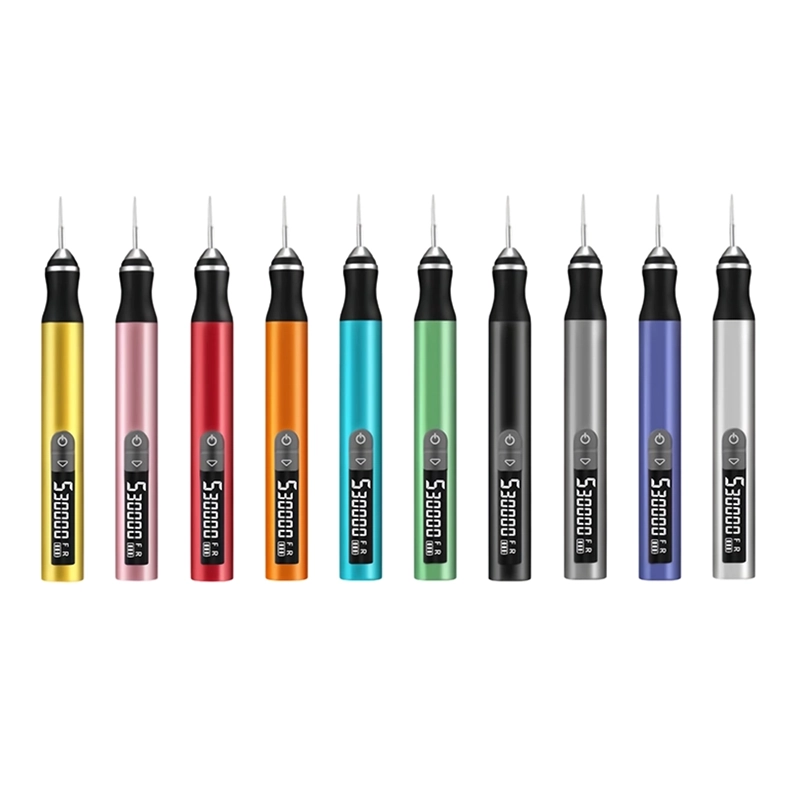
194Removing FDM Nozzle Blobs from a Z-Seam Without Flat Spots — H101 five-speed cordless engraving pen cover view for correcting isolated nozzle deposits on a curved enclosure or display part
August 20, 2026 · XOENAEN 3D Print & Rotary Application Team

Removing FDM Nozzle Blobs from a Z-Seam Without Flat Spots

Mark each blob and remove its crest individually before blending with a supported fine abrasive. For this job, control blob height, wall curvature, lighting, pressure and local temperature. Stop if the work band widens, the curve develops flats or softened debris smears. Accept the work only when raking light shows a continuous curve with no measurable wall loss.

Read article
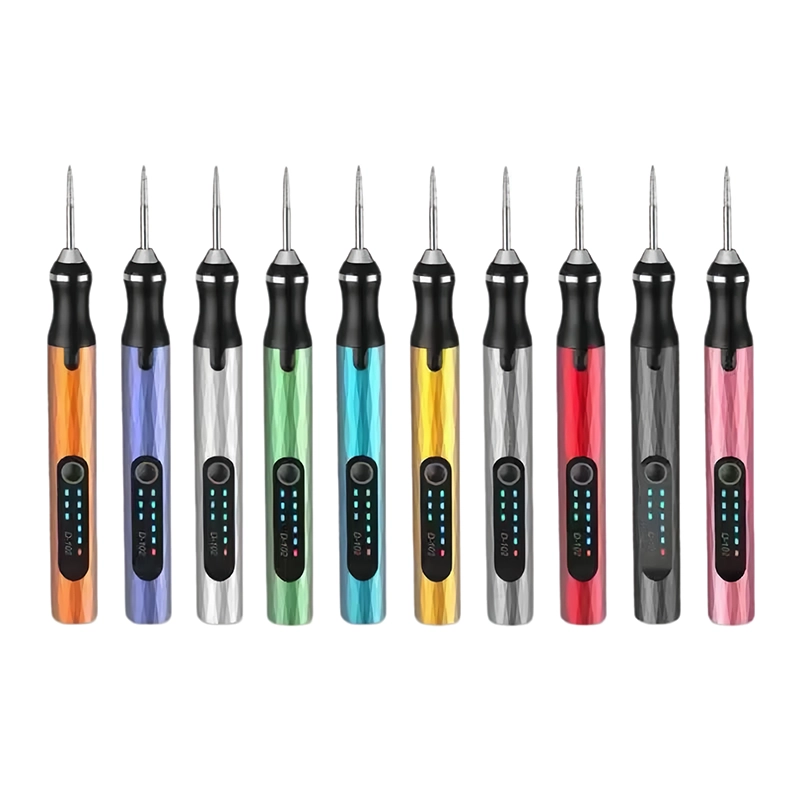
195Finishing a 3D Printed Vacuum-Forming Buck for Clean Release — H102 five-speed cordless engraving pen cover view for preparing a prototype buck used by a qualified thermoforming process
August 20, 2026 · XOENAEN 3D Print & Rotary Application Team

Finishing a 3D Printed Vacuum-Forming Buck for Clean Release

Preserve draft and vent paths while removing only defects that would print through or trap the sheet. For this job, control draft angle, edge radius, vent geometry, coating system and process temperature. Stop if a vent closes, a release edge rounds or heat limits are assumed rather than validated. Accept the work only when the buck matches its approved surface reference and downstream process checklist.

Read article
196Engraving Basswood Without Letting the Bit Follow the Grain — D-102 cordless electric engraving pen cover view for engraving names or small graphics in a basswood craft panel
August 20, 2026 · XOENAEN 3D Print & Rotary Application Team

Engraving Basswood Without Letting the Bit Follow the Grain

Use a shallow layout pass, stable two-hand control and progressive depth rather than one deep cut. For this job, control grain direction, point geometry, support, depth increments and dust removal. Stop if the point pulls into a soft band, tears an edge or obscures the layout line. Accept the work only when letter strokes remain centered, clean and consistent under direct light.

Read article
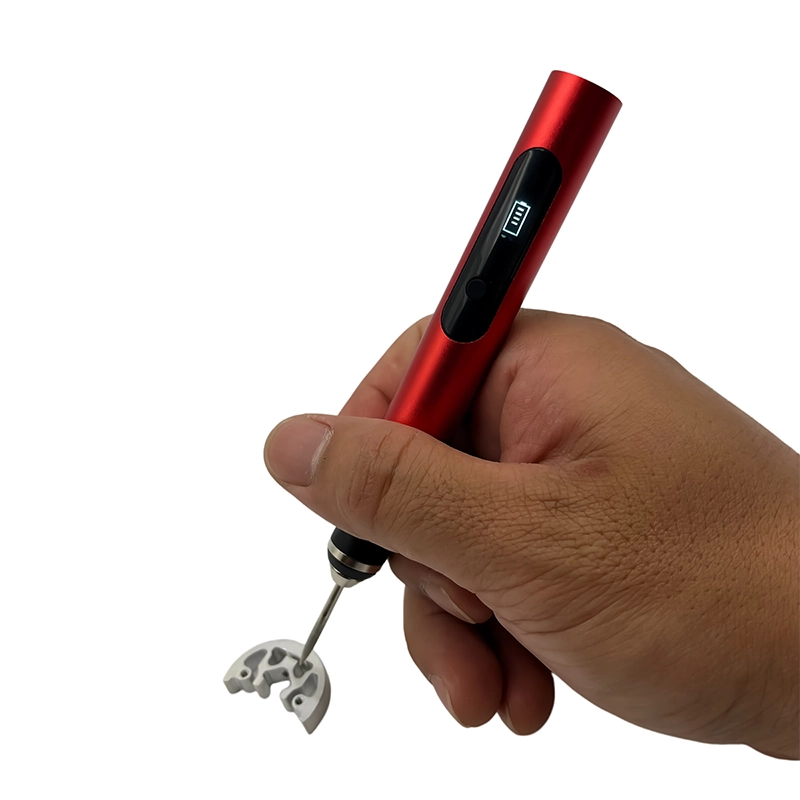
197Fine Lettering in Hardwood Without Burn Marks or Chipped Serifs — 104 mini rotary tool pen cover view for engraving a hardwood label, gift or workshop marker
August 20, 2026 · XOENAEN 3D Print & Rotary Application Team

Fine Lettering in Hardwood Without Burn Marks or Chipped Serifs

Use a sharp point, shallow passes and continuous motion with the work firmly supported. For this job, control wood species, grain, point condition, dwell and cut depth. Stop if dark burnishing, smoke, chatter or chipped serif corners appears. Accept the work only when the groove is clean, legible and ready for the approved finish without char.

Read article
198Polishing an Acrylic Edge with a Mini Rotary Tool Without Haze — 106 cordless precision rotary tool cover view for finishing a clear display panel, small sign or electronics window
August 20, 2026 · XOENAEN 3D Print & Rotary Application Team

Polishing an Acrylic Edge with a Mini Rotary Tool Without Haze

Flatten tool marks first, then progress through approved abrasives and polishing media with light contact. For this job, control edge flatness, media sequence, compound cleanliness, dwell and temperature. Stop if the edge waves, turns milky or shows fine stress cracks. Accept the work only when the edge is straight and reaches the agreed clarity under consistent lighting.

Read article
199Drilling Small Acrylic Project Holes Without Cracking the Panel — H101 five-speed cordless engraving pen cover view for adding a switch, indicator or mounting hole to a DIY acrylic panel
August 20, 2026 · XOENAEN 3D Print & Rotary Application Team

Drilling Small Acrylic Project Holes Without Cracking the Panel

Back the exit, mark the center and use a suitable sharp tool with controlled feed. For this job, control panel thickness, edge distance, backing, tool geometry and chip clearing. Stop if radial whitening, melting, grabbing or an exit chip develops. Accept the work only when the hole is round, on location and free of cracks under inspection.

Read article

Project inquiry

Bring us the brief.

Share your product, market, quantity and customization requirements. Our project team will reply with the right next step.