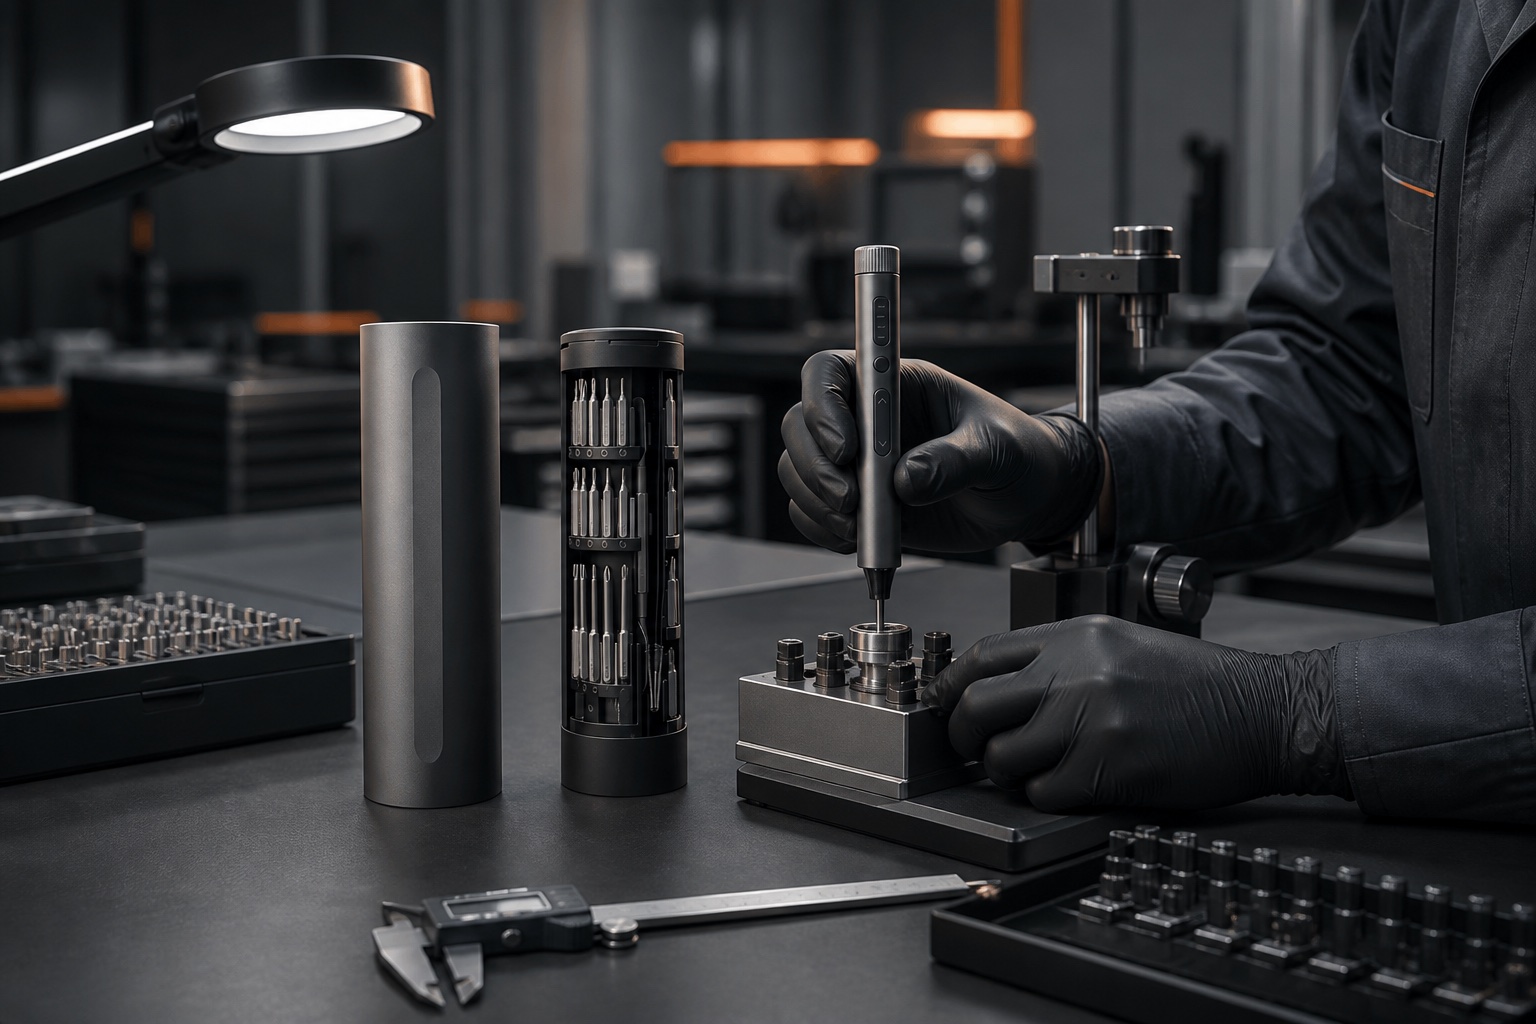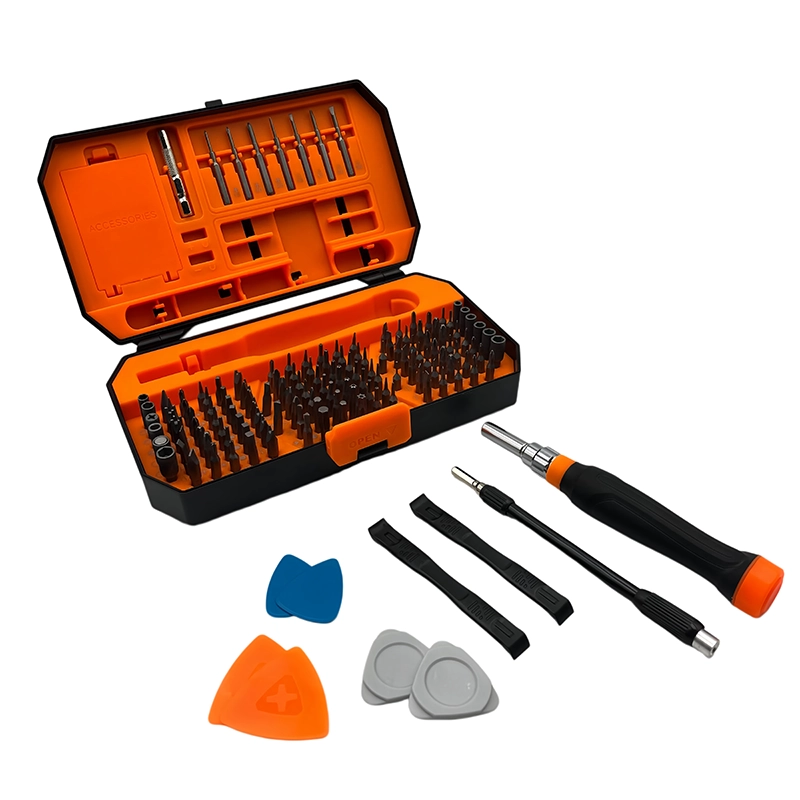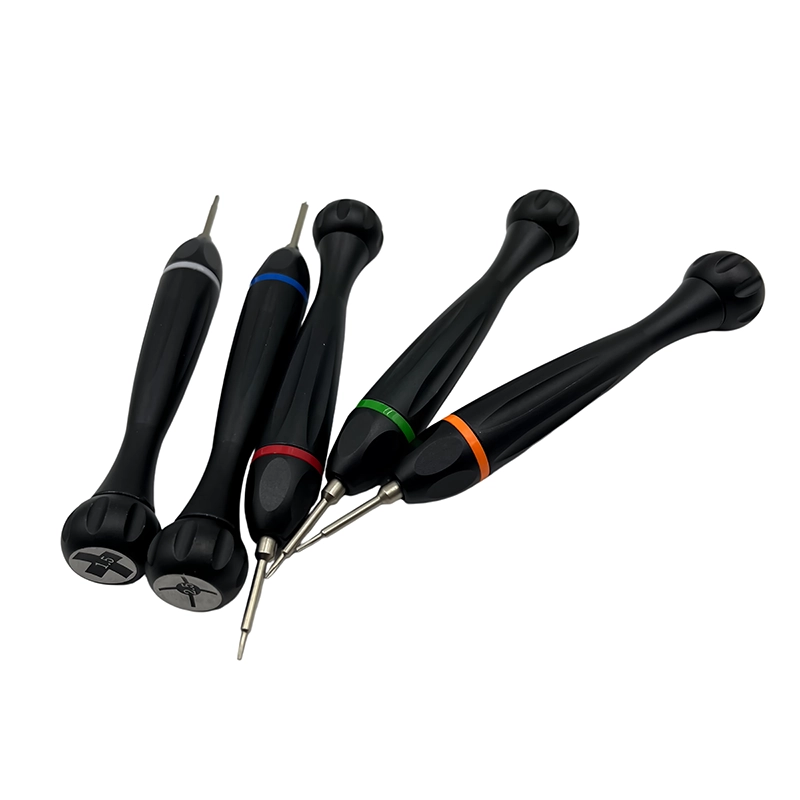
Inspect each shipment against the approved model, specification, sample, bit map, packaging, and agreed sampling plan. Verify quantity, identity, tip profiles, markings, holder engagement, installed-bit runout, handle and cap function, case retention, accessories, labels, and visible defects. Record lot and inspection results; do not replace application testing with a cosmetic check or an unverified material claim.
Incoming inspection for screwdriver sets
The documented acceptance process used by a buyer to compare delivered manual tool kits with approved specifications, samples, records, and agreed criteria.
What makes this manual screwdriver task different?
A screwdriver kit is a system of many small parts. The outer case can look correct while one bit map is wrong, a holder interface is loose, markings are duplicated, or packaging language belongs to another revision. Inspection must sample the complete configured SKU. The first decision is therefore not how much force the handle can deliver, but whether the service task, device condition, and operator authorization are clearly understood. Keep the manufacturer’s instructions, the actual fastener, and the surrounding parts in view before selecting a bit.
A manual driver gives useful tactile feedback only when the workpiece is supported and the tip remains fully engaged. For importers, distributors, quality teams, private-label brands, and procurement managers, that means treating access, visibility, screw identity, and reassembly records as part of the tool choice rather than as optional bench habits.
Which technical factors matter most?
Review purchase order, revision, lot, quantity, approved sample, drawings, bit map, profile gauges or references, material and hardness evidence where agreed, straightness, installed runout, magnetism where specified, handle cap, case retention, accessories, manuals, labels, and carton condition. Evaluate the complete installed system: handle, cap, holder, bit, fastener, access path, and work support. A premium material name or a high accessory count cannot compensate for partial recess contact or an unsafe service sequence.
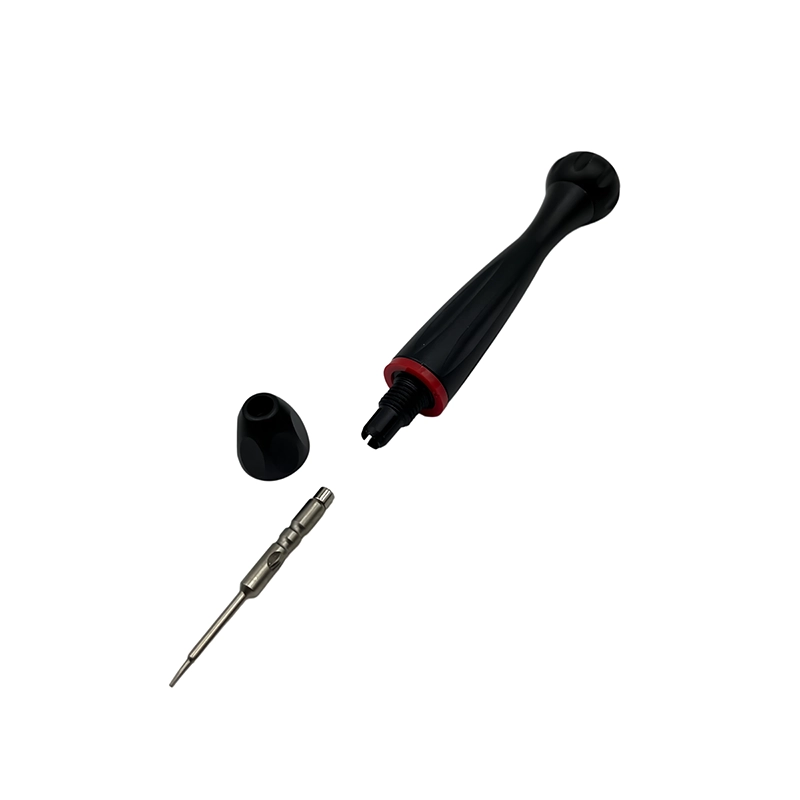
For manual screwdriver set incoming inspection, any drawing, service manual, torque specification or safety rule takes priority over general hand-tool guidance. Record the exact model, the condition described by a weak inspection counts the pieces and checks color but never seats the critical bits in an approved reference. the shipment passes even though duplicate markings, poor holder fit, or a wrong specialty profile will cause field failures. and the configuration used by importers, distributors, quality teams, private-label brands, and procurement managers. A revision can change fastener length, cable routing, sealing or authorized access, so the retained record must identify the actual article-specific task.
What workflow keeps the repair controlled?
1. Quarantine the received lot, verify documents and model identity, choose samples using the agreed plan, and photograph the unopened pack-out and lot marks. This preparation stage prevents the screwdriver from becoming the first tool used on an unidentified joint.
2. Count and map every component, inspect critical profiles and dimensions, check holder retention and cap function, compare runout and fit with approved references, and record nonconformities by severity. Place each removed fastener into a position-based map immediately rather than relying on memory or one mixed container.
3. Review packaging, manuals, labels, and cartons, decide acceptance under the agreed criteria, segregate rejects, and feed recurring issues into supplier corrective and change-control processes. Final inspection should confirm the joint, surrounding parts, and complete device function required by the manufacturer; a closed case alone is not proof of a successful repair.
How should buyers compare a manual screwdriver set?
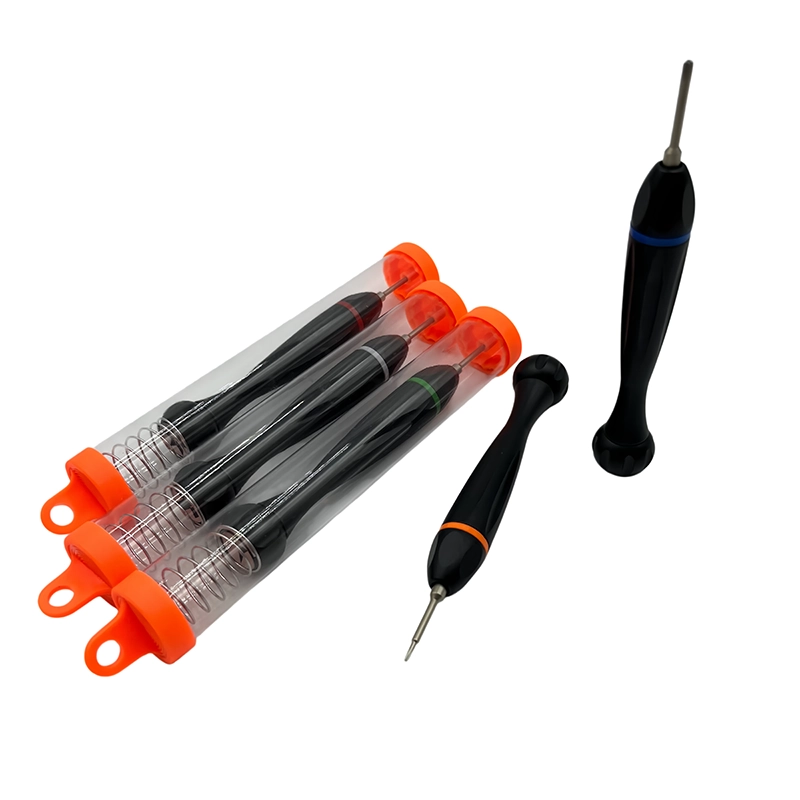
Compare candidates on verified profile fit, working reach, installed-bit stability, handle access, cap behavior, storage, labels, replacement support, and performance on representative fasteners. Buyers should agree inspection method, sampling, acceptance criteria, records, and change notification before production. XOENAEN catalogue evidence can identify the product platform, but order-specific approved documents govern the shipment.
For a wholesale or private-label manual screwdriver set incoming inspection project, freeze the bit map and case layout around this recommendation: Buyers should agree inspection method, sampling, acceptance criteria, records, and change notification before production. XOENAEN catalogue evidence can identify the product platform, but order-specific approved documents govern the shipment. Link the physical 206-in-1 manual screwdriver set sample, specification, product images, packaging text and the task-specific inspection criteria to one revision so the claim remains tied to the configuration that will ship.
What failure signs mean stop rather than push harder?
A weak inspection counts the pieces and checks color but never seats the critical bits in an approved reference. The shipment passes even though duplicate markings, poor holder fit, or a wrong specialty profile will cause field failures. The operator should preserve the remaining screw geometry and surrounding device instead of converting uncertainty into more force.
Hold the lot when identity or revision is uncertain, critical profiles fail fit, records do not match the order, parts are mixed, rejects cannot be segregated, or an unapproved change appears in product or packaging. Document the condition when the job is handed off. A clear stop rule protects the customer’s device and gives a qualified technician better options than a head damaged by repeated attempts.
How does this apply in a real repair?
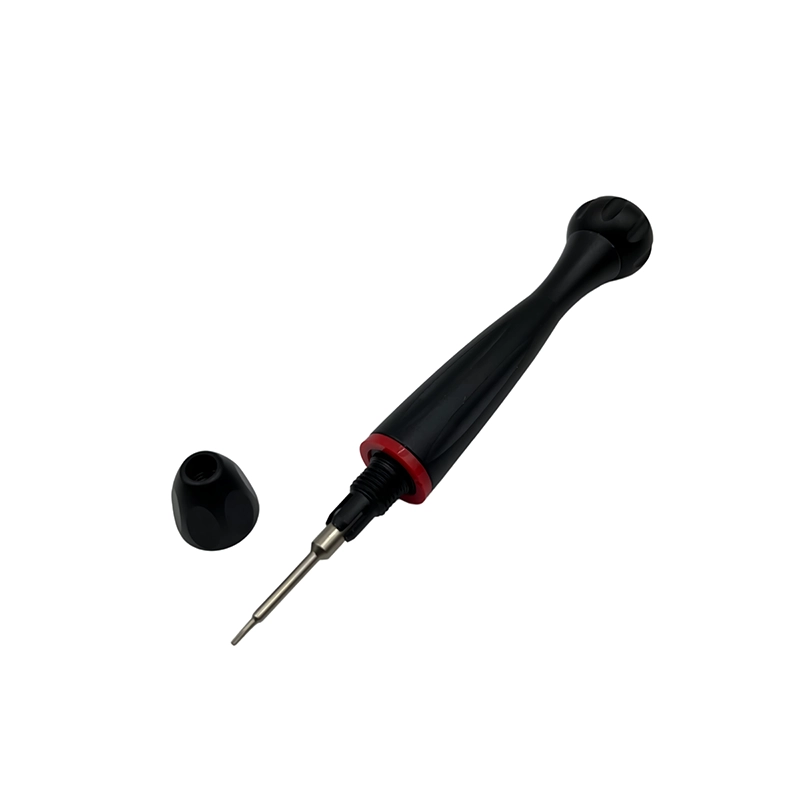
For a 206-in-1 configuration, inspection should use a controlled bit map and risk-based sample rather than treating every item as identical. High-use and specialty profiles deserve defined references, while the case is tested for retention after normal handling. Use the actual device instructions and representative hardware to confirm the method. Similar-looking screws can have different length, pitch, shoulder, coating, sealing, or grounding roles.
The buying decision for manual screwdriver set incoming inspection should cover review purchase order, revision, lot, quantity, approved sample, drawings, bit map, profile gauges or references, material and hardness evidence where agreed, straightness, installed runout, magnetism where specified, handle cap, case retention, accessories, manuals, labels, and carton condition. without encouraging force outside the defined task. Keep an exception path for the condition in hold the lot when identity or revision is uncertain, critical profiles fail fit, records do not match the order, parts are mixed, rejects cannot be segregated, or an unapproved change appears in product or packaging.; that path may require a different bit, opening tool, specified torque method, rated electrical tool, battery process or qualified specialist rather than a larger general-purpose set.
What does the XOENAEN catalogue add to the decision?
The current XOENAEN catalogue includes the 206-in-1 manual screwdriver set, the real product reference used for manual screwdriver set incoming inspection. Its photography and model record can anchor the buyer brief for for a 206-in-1 configuration, inspection should use a controlled bit map and risk-based sample rather than treating every item as identical. high-use and specialty profiles deserve defined references, while the case is tested for retention after normal handling. Catalogue evidence does not establish universal device compatibility; the actual fastener, access path, stop rule and order-specific sample still determine approval.
Incoming quality is a configuration-control problem. The accepted item is not an abstract screwdriver set; it is one model revision, bit map, accessory pack, label set, and packaging system tied to an order. Share target devices, fastener photos, required profiles, access constraints, market, quantity, packaging, and verification needs through the XOENAEN project enquiry so the product and evidence can be aligned before production.
Incoming inspection levels
| Option or condition | Best use | Main caution |
|---|---|---|
| Pack-out and visual check | Finds missing parts and visible defects | Cannot prove profile fit or function |
| Dimensional and functional sample | Tests critical interfaces and use | Requires methods and approved references |
| Application verification | Confirms selected real-task performance | Must be defined for the exact product and risk |
- Verify model, revision, and lot
- Compare the full bit map
- Inspect critical tip geometry
- Check holder, runout, and cap
- Review labels and manuals
- Record acceptance and segregate rejects
- 206-in-1 manual screwdriver set product page →
- Browse manual screwdriver products →
- Plan an OEM or private-label project →
- Review XOENAEN manufacturing and quality →
- Read XOENAEN tool FAQ answers →
- Related guide: tool-quality-verification →
- Related guide: manual-screwdriver-oem-private-label-kit →
- How XOENAEN presents quality evidence →
Is counting pieces enough for incoming inspection?
No. Count and identity matter, but fit, geometry, function, records, labels, and configuration also need agreed checks.
Should every bit be tested?
Use the agreed risk-based sampling and critical-characteristic plan; full checks may be required for specific risks or configurations.
What is an approved sample used for?
It provides a controlled physical comparison for features defined in the order, but it does not replace drawings and acceptance criteria.
Why check installed-bit runout?
The handle, holder, and bit interact; excessive installed wobble can reduce centering even when the loose bit looks straight.
What happens to rejected samples?
Segregate, identify, document, and disposition them under the buyer’s quality process so they cannot re-enter accepted stock.
How should supplier changes be handled?
Require documented notification, review, sample or evidence approval, and revision control before the changed configuration ships.