Choose rotary-tool bits for 3D print post-processing by the job they must perform. Cutting and abrasive accessories remove material differently; brushes clean differently from polishing media. Identify the polymer, defect, access and protected geometry, then trial the accessory on scrap at a conservative setting. Short contact and frequent inspection matter more than a large accessory count, because one wrong bit can quickly change fit.
Rotary-tool accessory selection
Rotary-tool accessory selection is the controlled matching of an accessory material, shape and working face to a defined removal or finishing task on a known printed material and geometry.
What should be decided before rotary-tool bit selection for 3D printed parts?
Name the defect first: attached support, proud seam, rough contour, blocked hole, residue or polishing haze. This first decision keeps matching cutters, abrasives, brushes and polishing accessories to specific printed-part defects tied to a real task rather than a generic tool claim. Record what is known, what is assumed and which part of the decision still needs a sample. The practical boundary is to select by task, material, geometry and removal rate rather than the visual similarity of accessory shapes. If the work cannot be described that clearly, pause before choosing an accessory or publishing a recommendation.
Which work details control rotary-tool bit selection for 3D printed parts?
Identify polymer, reinforcement, wall thickness and nearby edges before choosing an accessory family. Treat the check as part of one controlled workflow. The main failure to prevent is gouging, melting, fiber pull-out, enlarged openings and contaminated finishing surfaces. Use a representative part, fastener or sample whenever possible, and change one variable at a time so the observation remains useful. A catalogue image can identify the referenced platform, but it does not prove the result on an untested material, device or production lot.
How should the tool or method be selected for rotary-tool bit selection for 3D printed parts?
Match accessory shape to access so only the intended working face contacts the print. Selection should follow the working interface rather than accessory count or a broad marketing label. Note the contact geometry, available clearance, operator visibility and the point at which powered work should stop. Confirm the choice through a low-risk coupon trial followed by dimensional and visual inspection before touching the final part. Retain the rejected option as well as the chosen one so later changes can be traced to a reason.
What setup reduces risk during rotary-tool bit selection for 3D printed parts?
Start on a coupon with light pressure and short contact while watching heat and debris formation. Set up the work so movement, heat, debris and access can be observed. Support the item without loading a delicate feature, begin conservatively and inspect after a short interval. If the response differs from the sample or the expected condition, stop and reassess instead of compensating with more force, speed or time.
How should the first sample be checked?
Inspect dimensions and surface direction before moving from removal to refinement or polishing. A useful first pass answers a narrow question; it is not a demonstration of maximum removal or output. Compare the result with the baseline, clean the interface before inspection and write down the setting only with its material, accessory and geometry. This turns an isolated trial into evidence that can inform the next controlled step.
When should the operator stop and reassess?
Discard loaded, damaged or contaminated accessories instead of increasing pressure to compensate. The stop rule matters as much as the starting method. Stop when the tool loses alignment, the surface changes unexpectedly, heat or debris obscures the work, or the remaining geometry approaches its acceptance boundary. Escalate critical or uncertain conditions rather than converting a limited guide into an unsupported universal instruction.
What evidence belongs in the approval record?
Document the useful accessory sequence for the specific material and geometry, including its stop condition. For approval, keep the model or material identity, sample condition, method, observation, date and accountable decision together. The appropriate evidence is a low-risk coupon trial followed by dimensional and visual inspection before touching the final part. Separate a product-existence record from a measured performance record, and state openly when a result still needs buyer or laboratory confirmation.
Which XOENAEN product reference supports this guide?
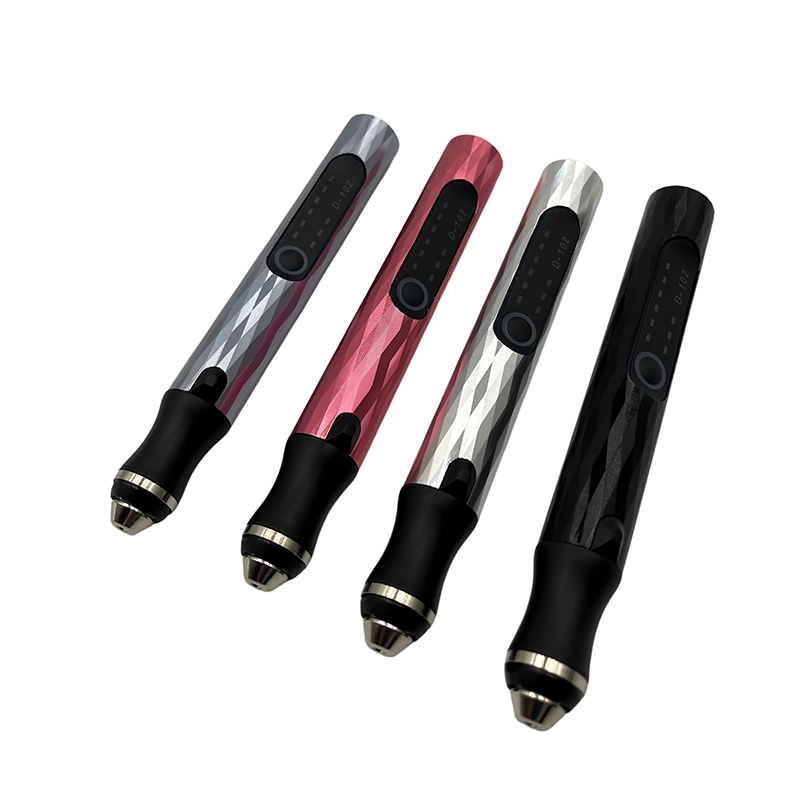
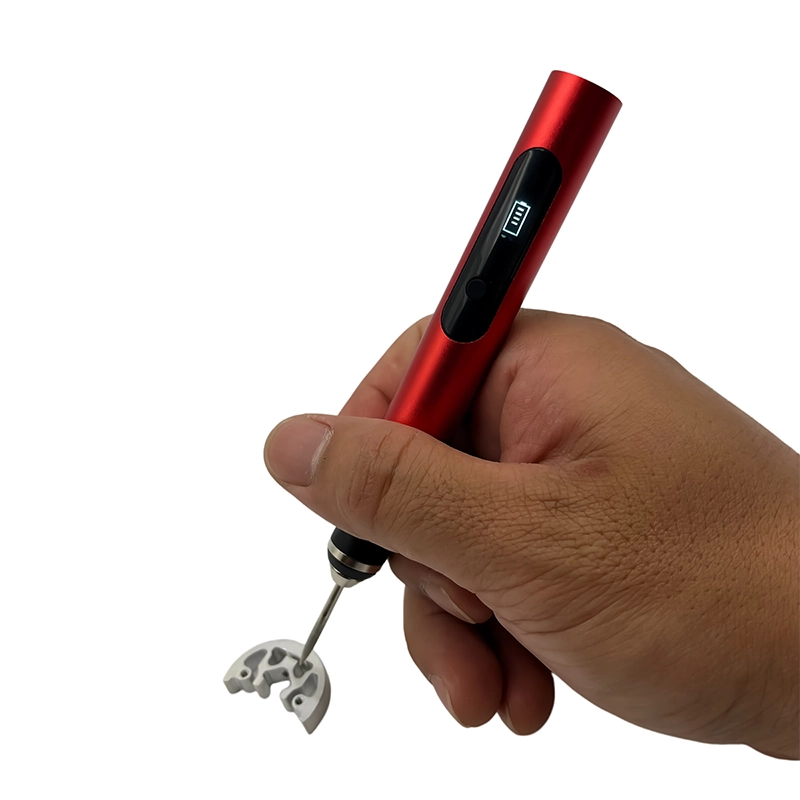
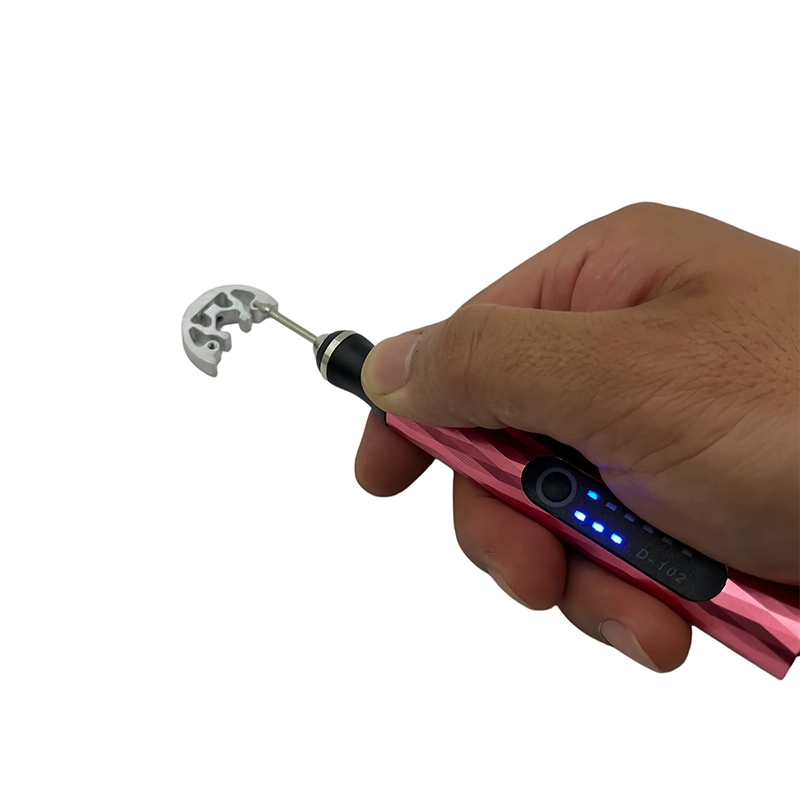
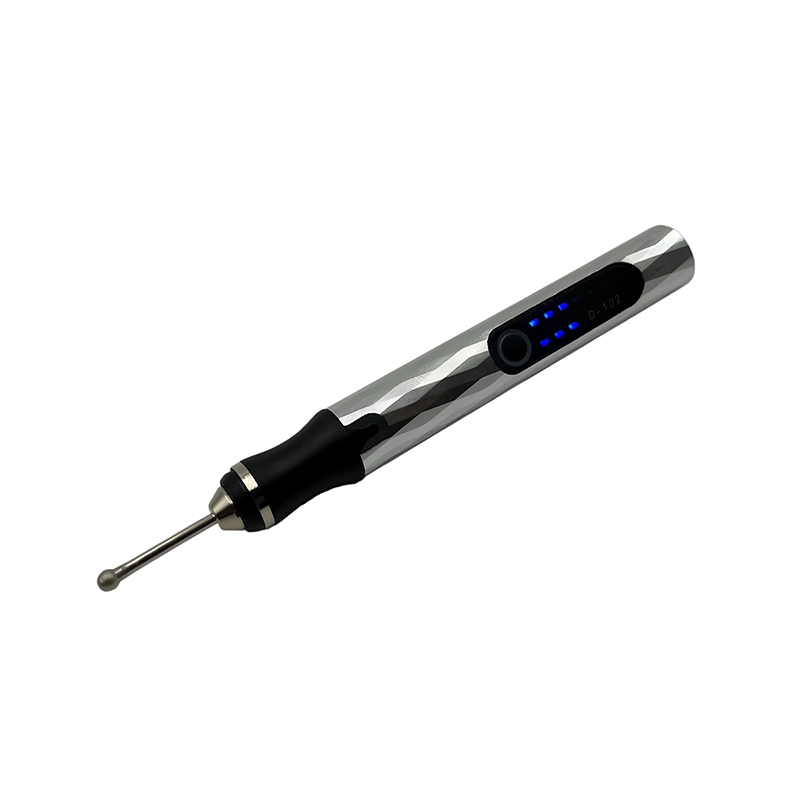
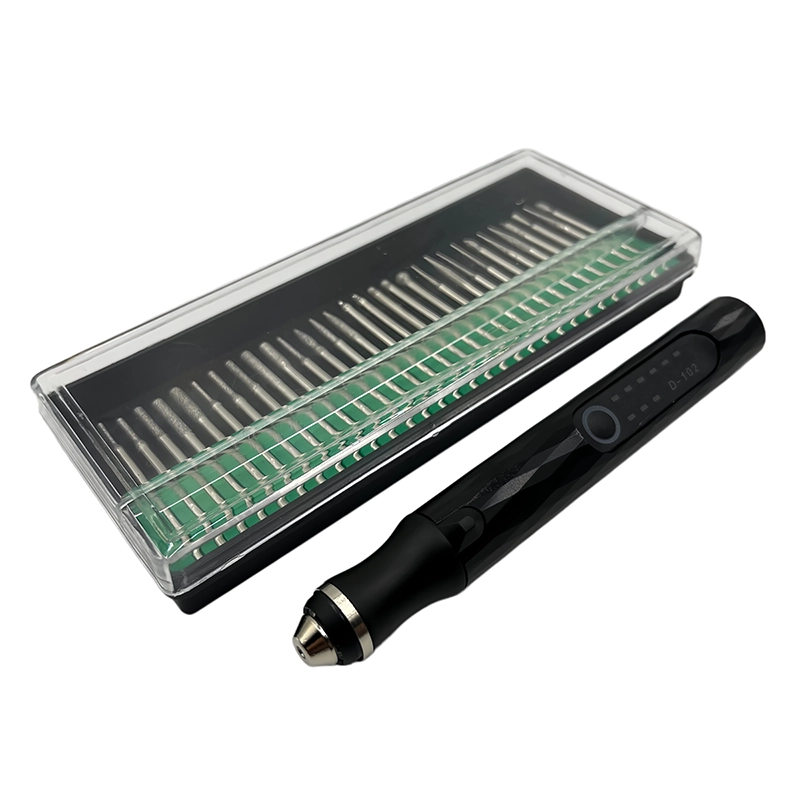
Use D-102 catalogue images to discuss interface and kit layout without asserting an unverified universal result. The relevant first-party reference is the XOENAEN D-102 cordless rotary pen. It shows a documented product configuration that can anchor a discussion about rotary-tool bit selection for 3D printed parts. Final suitability still depends on the exact task and sample because the catalogue does not establish compatibility with every device, polymer, fastener or finishing requirement.
Before closing the job, compare the result with the written requirement for rotary-tool bit selection for 3D printed parts, clean the work area and retain any measurement, fit observation or unresolved exception. This final pause prevents a visually acceptable result from being mistaken for verified functional approval and gives the next operator or buyer a clear starting record.
Decision paths for rotary-tool bit selection for 3D printed parts
| Path | Use when | Control |
|---|---|---|
| Proceed with a controlled sample | The application and boundary are documented for rotary-tool bit selection for 3D printed parts | a low-risk coupon trial followed by dimensional and visual inspection before touching the final part |
| Pause and clarify | Material, geometry, model or acceptance criteria remain uncertain | Prevent gouging, melting, fiber pull-out, enlarged openings and contaminated finishing surfaces |
| Escalate or replace | The task is critical, damaged or outside the verified boundary | Use an approved specialist, replacement or documented alternative |
- Write the actual customer question for rotary-tool bit selection for 3D printed parts
- Identify the exact product, material, fastener or geometry involved
- Define the acceptance boundary and the risk to prevent: gouging, melting, fiber pull-out, enlarged openings and contaminated finishing surfaces
- Approve the sample method: a low-risk coupon trial followed by dimensional and visual inspection before touching the final part
- Retain the model, accessory or bit map and the dated decision record
- Review the XOENAEN D-102 cordless rotary pen →
- Continue with the related rotary tool for 3d print support removal guide →
- Continue with the related rotary tool for 3d print holes and slots guide →
- Open the complete 3D print finishing pillar guide →
- How XOENAEN separates product facts from test evidence →
- XOENAEN editorial and technical review policy →
- Discuss the application and sample plan →
What is the first decision in rotary-tool bit selection for 3D printed parts?
Define the exact application and acceptance boundary first. For this guide, that means select by task, material, geometry and removal rate rather than the visual similarity of accessory shapes. Tool or accessory choice should follow that written requirement.
What is the main risk when rotary-tool bit selection for 3D printed parts?
The main risk is gouging, melting, fiber pull-out, enlarged openings and contaminated finishing surfaces. Use a representative sample, short controlled steps and frequent inspection instead of assuming one setting or configuration is universally safe.
How should a sample for rotary-tool bit selection for 3D printed parts be verified?
Use a low-risk coupon trial followed by dimensional and visual inspection before touching the final part. Record the applicable model or material, method, observations and decision so the result is not separated from the conditions that produced it.
Can one recommendation cover every case of rotary-tool bit selection for 3D printed parts?
No. In rotary-tool bit selection for 3D printed parts, device design, material, fastener, geometry, accessory and service condition can change the outcome. This guide provides a decision method; final suitability requires a representative check.
Which XOENAEN product is referenced for rotary-tool bit selection for 3D printed parts?
For rotary-tool bit selection for 3D printed parts, the first-party reference is the D-102 cordless rotary pen. Its catalogue page documents the platform and images used here, but it is not presented as proof of an untested application result.
What should a buyer record for rotary-tool bit selection for 3D printed parts?
For rotary-tool bit selection for 3D printed parts, record the requirement, chosen model or material, accessory or bit map, sample method, acceptance boundary, packaging or workflow revision, and the person responsible for the final approval.