Product knowledge

Useful decisions. Better tool projects.

Practical product, OEM/ODM and quality guidance grounded in the tools and project work shown across this site.

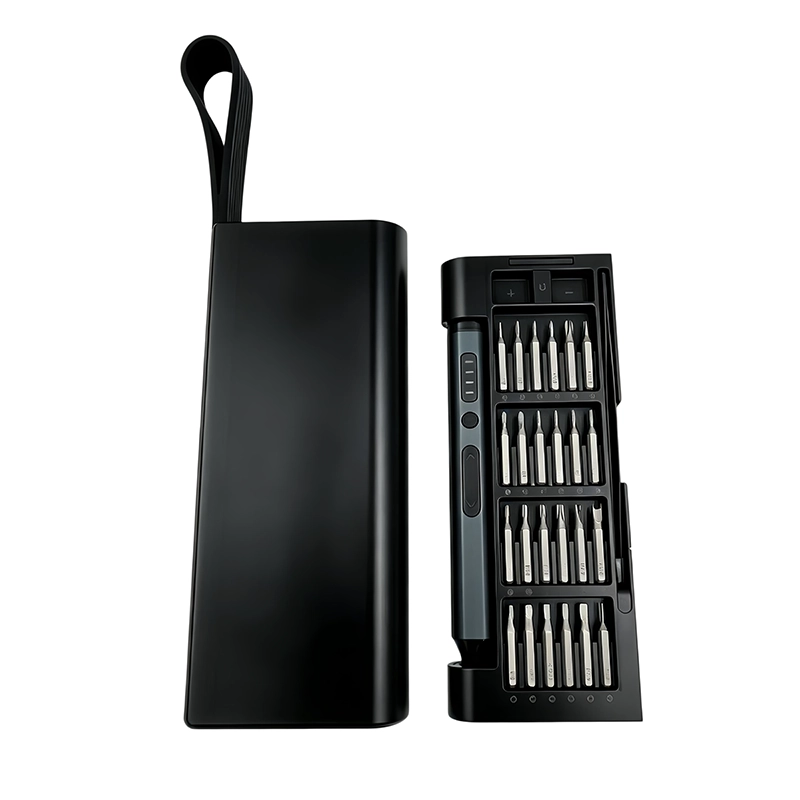
Electric Screwdriver Spare Parts Service Plan; XOENAEN 53-in-1 precision electric screwdriver set shown as a product configuration referenceOctober 30, 2026Electric Screwdriver Spare Parts Service PlanRead article →
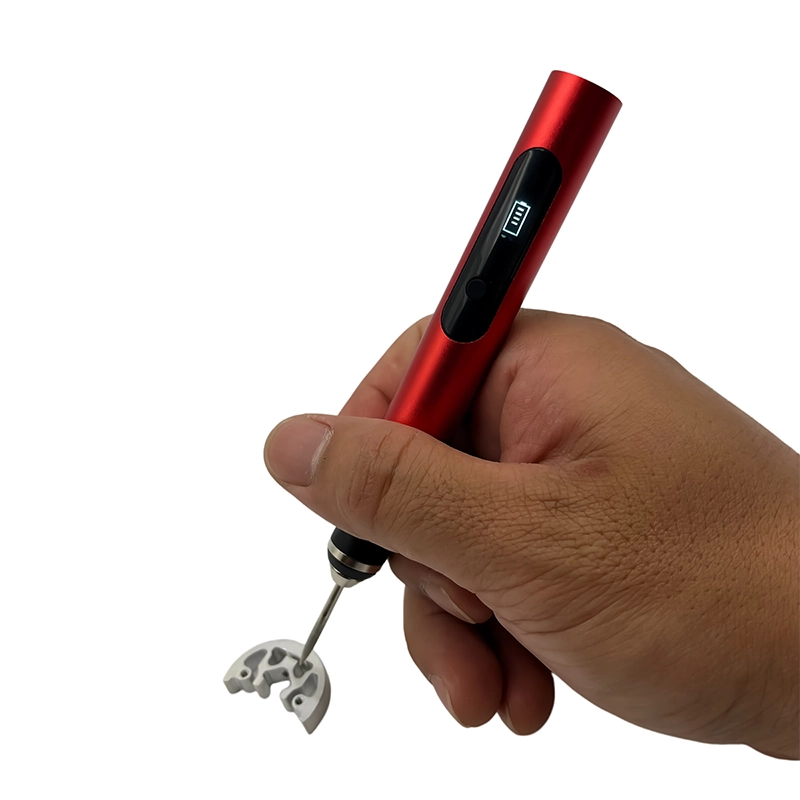
224How to Clean 3D Printed Lattice Vents Without Breaking Struts — H101 five-speed cordless engraving pen cover view for cleaning an architectural panel, speaker grille or lightweight cover
August 20, 2026 · XOENAEN 3D Print & Rotary Application Team

How to Clean 3D Printed Lattice Vents Without Breaking Struts

Stabilize a small zone and use cutting or hand methods before considering powered contact. For this job, control strut thickness, support location, tool direction and vibration. Stop if a strut chatters, turns white or develops a notch at a node. Accept the work only when all required openings are clear and every strut matches the retained reference pattern.

Read article →
225Finishing a Multi-Material 3D Print Seam Without Smearing Colors — H102 five-speed cordless engraving pen cover view for blending a decorative logo or soft-overmold transition on a printed part
August 20, 2026 · XOENAEN 3D Print & Rotary Application Team

Finishing a Multi-Material 3D Print Seam Without Smearing Colors

Test each material separately and approach the interface from the harder, better-supported side. For this job, control material hardness, color transfer, abrasive loading and interface adhesion. Stop if one material recedes faster, pigment transfers or the bond edge begins to lift. Accept the work only when the transition is even under raking light with no color smear or exposed gap.

Read article →
226Finishing an ASA Outdoor 3D Printed Part Without Weak Edges — D-102 cordless electric engraving pen cover view for deburring an outdoor sensor enclosure or functional bracket
August 20, 2026 · XOENAEN 3D Print & Rotary Application Team

Finishing an ASA Outdoor 3D Printed Part Without Weak Edges

Limit finishing to noncritical flash and preserve designed radii and protective surface sections. For this job, control load path, UV-exposed surface, temperature, edge geometry and coating plan. Stop if a structural corner becomes sharp, a wall thins or heat gloss masks a smear. Accept the work only when the part retains its drawing features and the approved coating or weathering preparation.

Read article →
227Finishing Polycarbonate 3D Prints Without Heat Gloss or Cracks — 104 mini rotary tool pen cover view for cleaning a functional polycarbonate prototype after support removal
August 20, 2026 · XOENAEN 3D Print & Rotary Application Team

Finishing Polycarbonate 3D Prints Without Heat Gloss or Cracks

Use sharp media, short contact and a scrap coupon before touching load-bearing geometry. For this job, control dwell, pressure, layer direction, residual stress and feature thickness. Stop if a glossy patch, whitening line or sharp notch appears beside the worked zone. Accept the work only when the edge is clean, cool and free of cracks under direct inspection.

Read article →
228Deburring Polypropylene 3D Prints Without Fuzz or Rolled Edges — 106 cordless precision rotary tool cover view for cleaning a clip, living container part or chemical-resistant prototype
August 20, 2026 · XOENAEN 3D Print & Rotary Application Team

Deburring Polypropylene 3D Prints Without Fuzz or Rolled Edges

Support the feature and favor a sharp shearing action over prolonged rubbing. For this job, control edge restraint, abrasive condition, contact direction and surface temperature. Stop if the edge rolls, feathers or stretches instead of producing a clean chip. Accept the work only when the corrected edge returns to shape and has no loose fuzz or notch.

Read article →
229Removing Support Nubs from Flexible Resin Prints Without Tears — H101 five-speed cordless engraving pen cover view for cleaning a wearable prototype, gasket sample or soft model after support removal
August 20, 2026 · XOENAEN 3D Print & Rotary Application Team

Removing Support Nubs from Flexible Resin Prints Without Tears

Cut the support close with the part supported and refine only the remaining proud spot. For this job, control cure state, feature support, cut direction and local heat. Stop if the nub stretches, a crescent tear starts or the surface becomes tacky or glossy. Accept the work only when the area flexes through its intended range without a growing cut.

Read article →

Project inquiry

Bring us the brief.

Share your product, market, quantity and customization requirements. Our project team will reply with the right next step.