Check the adhesive supplier’s preparation method and use a flat reference before any powered step. Support the work with a clean right-angle support keeping the panel vertical and the visible face protected. Control panel material, edge flatness, heat, abrasive residue and solvent compatibility. Stop when the edge turns convex, the panel crazes or a polished face develops a heat mark.
prepare acrylic edge for solvent bonding
prepare acrylic edge for solvent bonding is a controlled workshop process for a laser-cut or sawn acrylic panel for a display case or electronics enclosure that corrects small saw marks, laser ridge or isolated burr on the bonding edge while preserving edge squareness, panel length, polished visible face and full joint contact.
A highly polished edge may bond differently from the preparation specified for the chosen adhesive, so gloss is not the acceptance target. This article answers “How should a cut acrylic edge be prepared when it must form a straight bonded joint?” for a laser-cut or sawn acrylic panel for a display case or electronics enclosure. It is a workshop planning guide, not a universal compatibility promise. Material, geometry, accessory, workplace controls and the buyer’s acceptance sample determine whether a method is suitable.
How should a cut acrylic edge be prepared when it must form a straight bonded joint?
Check the adhesive supplier’s preparation method and use a flat reference before any powered step. The defect in scope is small saw marks, laser ridge or isolated burr on the bonding edge. Clean the part, photograph the starting condition and mark the smallest area that actually needs correction. For prepare acrylic edge for solvent bonding, the first pass should be short enough that the original condition remains easy to compare with the result.
What must remain unchanged during this finishing task?
Protect edge squareness, panel length, polished visible face and full joint contact. Those features define function or visible quality on a laser-cut or sawn acrylic panel for a display case or electronics enclosure. Write them on the job card before choosing media. A useful instruction states where contact is allowed, where it is forbidden and which gauge or mating part will reveal a mistake; a broad instruction such as use low speed is not enough.
How should the part be supported before any abrasive touches it?
Use a clean right-angle support keeping the panel vertical and the visible face protected. Place support near the worked zone without preloading a flexible wall, lug, edge or joint. Confirm that the work cannot rotate into the accessory, that the operator’s hands remain outside the path and that dust can be captured without hiding the contact point. Reapprove the setup if the fixture changes.
Which hand method provides the safest reference?
a long flat scraper or sanding block that references the whole edge gives the operator a tactile baseline for prepare acrylic edge for solvent bonding. Use it on a representative defect and record the number and direction of passes, cleanup method and resulting geometry. Hand work is not automatically harmless, but its slower feedback can expose a wrong contact map before a powered method repeats it across a valuable part.
When does a rotary or reciprocating method add value?
a rotary abrasive reserved for a local nonbonding obstruction, not the final joint plane may help when access, repeatability or local stock removal makes the hand reference impractical. It should enter the workflow only after the contact zone is understood. For this workpiece, control panel material, edge flatness, heat, abrasive residue and solvent compatibility. A tool feature or accessory name alone does not prove suitability for the customer’s material and part revision.
Which variables belong in the first-piece record?
Record panel material, edge flatness, heat, abrasive residue and solvent compatibility, plus the exact material, part revision, fixture identity, accessory code, clean starting image and environmental controls. For prepare acrylic edge for solvent bonding, also note whether the sample was printed, cured, bonded, coated or conditioned as production parts will be. That record lets another operator repeat the decision instead of imitating a demonstration.
What sequence keeps the correction local and reversible?
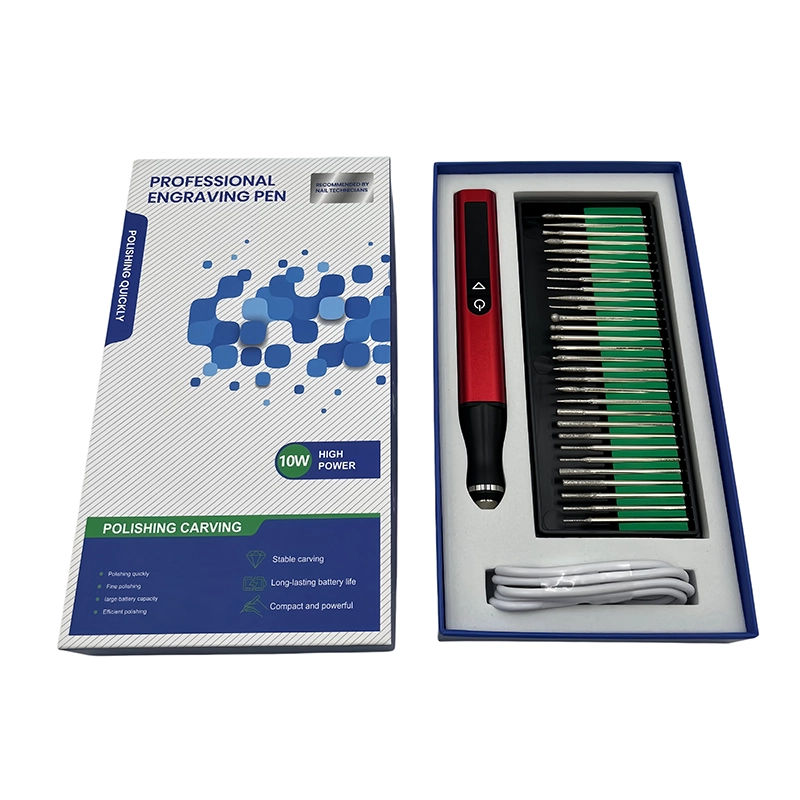
Inspect, mark, support, make one short pass, stop, clean and measure. Repeat only when the inspection still shows small saw marks, laser ridge or isolated burr on the bonding edge outside the approved boundary. Change one variable at a time and retain an untouched reference where practical. If the defect occurs on every part, investigate design, printing, cutting or upstream process control instead of normalizing unlimited rework.
Which warning means the powered pass must stop?
Stop immediately when the edge turns convex, the panel crazes or a polished face develops a heat mark. Isolate the tool, remove debris without spreading it and compare the area with the start image. More speed or pressure cannot restore removed geometry. A clear stop signal is particularly important for a small rotary or reciprocating kit because a light tool can still concentrate contact on a narrow edge.
How should the finished result be inspected?
Use a machinist square, backlight joint check, retained offcut and adhesive-process review. The release rule is specific: the mating panels meet along the specified joint with no rocking, trapped debris or changed angle. Inspect the cleaned part at a stable temperature, not while dust or polish masks the surface. Where fit, sealing, motion, alignment or airflow matters, a visual improvement cannot replace the agreed functional or dimensional check.
How do the hand and powered routes compare on a real sample?
Compare a long flat scraper or sanding block that references the whole edge with a rotary abrasive reserved for a local nonbonding obstruction, not the final joint plane on equivalent defects. Measure setup time, correction time, cleanup, retained geometry, inspection effort and rejects. For prepare acrylic edge for solvent bonding, the better route is the one that repeatedly protects edge squareness, panel length, polished visible face and full joint contact, not simply the one that removes material fastest in a short video.
Which product details should an EU or North American buyer review?
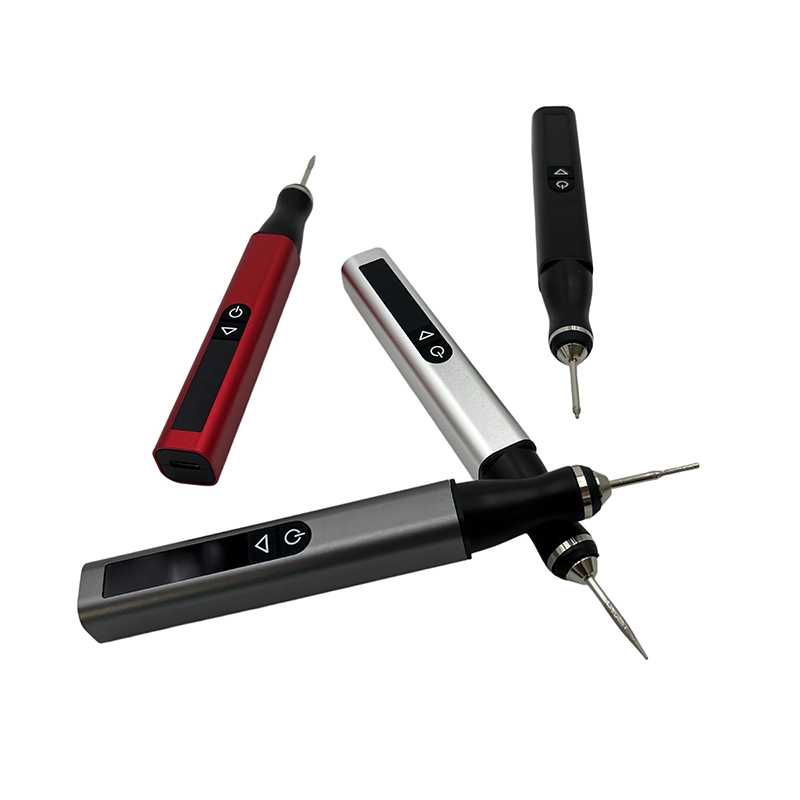
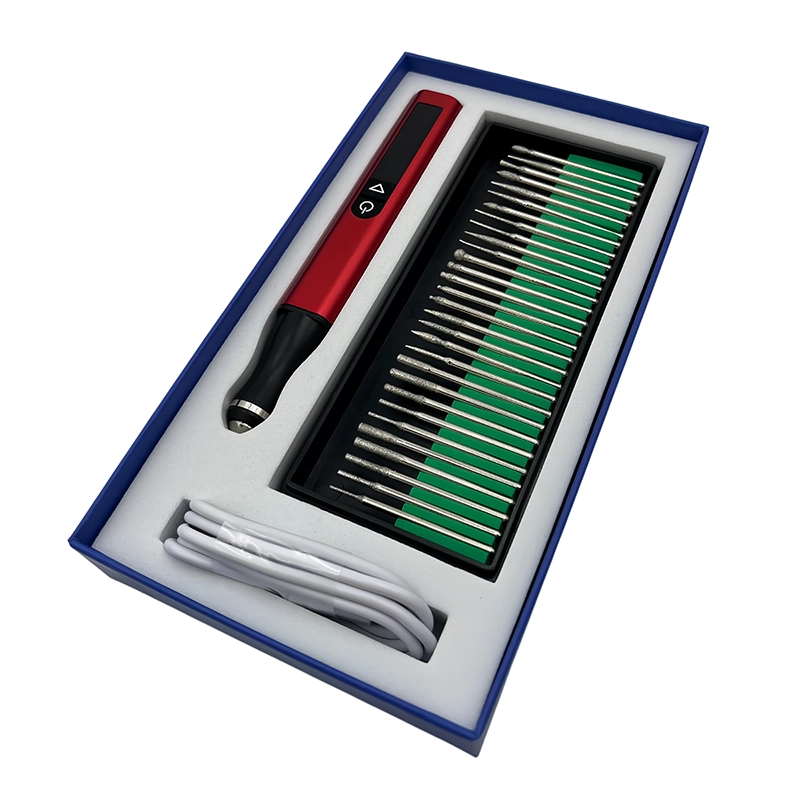
The XOENAEN H102 five-speed cordless engraving pen is a current XOENAEN catalogue reference for the discussion, not evidence that every accessory works on a laser-cut or sawn acrylic panel for a display case or electronics enclosure. Review the exact control interface, charging configuration, compatible accessory shank, supplied media identity, replacement-consumable plan, labels, instructions and target-market documentation on the final sample configuration.
What should be included in an OEM or wholesale brief?
Provide acrylic grade and thickness, cut method, adhesive system, joint drawing and visual acceptance sample. Add target sales markets, annual or order volume, packaging language, replacement accessories, sample quantity, change-control expectations and the person authorized to approve the first article. Claims in packaging and online listings should remain inside what the same configuration and documented sample method actually demonstrate.
Which evidence makes this answer useful to search and AI systems?
A reliable answer for prepare acrylic edge for solvent bonding names the customer question, exact workpiece, protected feature, method comparison, stop condition and acceptance evidence. Link the real product page, application guide and primary safety or process sources. Avoid invented rankings, unnamed customer outcomes or borrowed certification claims; those details may attract clicks briefly but weaken trust and purchasing decisions.
For shop use, keep the final record with the exact part revision, XOENAEN H102 five-speed cordless engraving pen configuration, accessory identity, fixture, accepted sample and inspection evidence. A highly polished edge may bond differently from the preparation specified for the chosen adhesive, so gloss is not the acceptance target. That concrete chain from question to decision to proof is more useful than repeating that a tool is professional, versatile or suitable for every material.
Before a production or retail release for prepare acrylic edge for solvent bonding, ask a second operator to follow the written sequence on another representative workpiece. Compare the resulting the mating panels meet along the specified joint with no rocking, trapped debris or changed angle against the retained first article, reconcile every accessory and revise the instruction whenever the workpiece, coating, fixture or supplied kit configuration changes.
Hand control compared with powered local finishing
| Method | Best use | Main risk to control |
|---|---|---|
| a long flat scraper or sanding block that references the whole edge | Establish tactile contact and a geometry reference | Slow access or inconsistent operator angle |
| a rotary abrasive reserved for a local nonbonding obstruction, not the final joint plane | Reach or repeated local correction after mapping | the edge turns convex, the panel crazes or a polished face develops a heat mark |
| Upstream process correction | A defect repeats across parts | Requires a new sample and validation cycle |
- Define the real workpiece: a laser-cut or sawn acrylic panel for a display case or electronics enclosure
- Map the defect: small saw marks, laser ridge or isolated burr on the bonding edge
- Protect edge squareness, panel length, polished visible face and full joint contact
- Support with a clean right-angle support keeping the panel vertical and the visible face protected
- Control panel material, edge flatness, heat, abrasive residue and solvent compatibility
- Stop when the edge turns convex, the panel crazes or a polished face develops a heat mark
- Approve only when the mating panels meet along the specified joint with no rocking, trapped debris or changed angle
- XOENAEN H102 five-speed cordless engraving pen →
- Rotary versus reciprocating finishing selection →
- Finishing a 3D Printed Hose Barb Without Flattening Seal Ribs →
- Polishing a Clear Resin Light Pipe Without Changing Its Optical Face →
- Shaping a Balsa Model Airfoil Leading Edge Without Flat Spots →
- OEM and ODM tool development →
- Continue with the deburr-drilled-petg-sheet-project-panel topic →
- XOENAEN editorial policy →
What should be measured first when you prepare acrylic edge for solvent bonding?
Begin with a machinist square, backlight joint check, retained offcut and adhesive-process review and preserve a clean starting image of a laser-cut or sawn acrylic panel for a display case or electronics enclosure. The first record must distinguish small saw marks, laser ridge or isolated burr on the bonding edge from an acceptable feature before any material is removed.
Why is workholding critical for prepare acrylic edge for solvent bonding?
The recommended support is a clean right-angle support keeping the panel vertical and the visible face protected. It keeps vibration and unintended movement away from edge squareness, panel length, polished visible face and full joint contact, while giving the operator a stable, visible contact zone and a repeatable setup for the next sample.
Which method should be tested before powered finishing for prepare acrylic edge for solvent bonding?
Use a long flat scraper or sanding block that references the whole edge as the tactile reference. Then compare it with a rotary abrasive reserved for a local nonbonding obstruction, not the final joint plane on equivalent defects, including setup, cleanup, geometry retention and the final inspection rather than speed alone.
What is the stop signal for prepare acrylic edge for solvent bonding?
Stop when the edge turns convex, the panel crazes or a polished face develops a heat mark. Clean and inspect before deciding whether a different accessory, fixture, hand method or upstream process change is needed; continuing can hide the cause and remove functional material.
Does the rotary-h102 guarantee prepare acrylic edge for solvent bonding?
No. The rotary-h102 is a real XOENAEN catalogue reference, but suitability depends on the material, geometry, accessory, controls and acceptance sample for a laser-cut or sawn acrylic panel for a display case or electronics enclosure. Validate the final configuration before making a market claim.
What should a buyer send for a prepare acrylic edge for solvent bonding quotation?
Provide acrylic grade and thickness, cut method, adhesive system, joint drawing and visual acceptance sample. Include market, volume, packaging, replacement-consumable needs and the exact sample and inspection method that will approve or reject the proposed tool configuration.