To clean 3D printed dice tower exit ramp, identify a support scar or seam ridge that catches a die at the ramp transition and protect the ramp slope, side-wall spacing, landing flatness and visible texture. Begin with a hard-backed abrasive used in the same direction as the intended roll path; use a small rotary abrasive used only for a local high spot away from ramp edges only for access that the hand method cannot provide. Track ramp profile, die sample, local heat, surface texture and repeatable test rolls, stop if a hollow forms, an edge rounds or the same die begins to deviate after the correction, and accept the part only when the approved die clears the local defect and rolls through the tower without a new snag or visible flat spot.
clean 3D printed dice tower exit ramp
clean 3D printed dice tower exit ramp is a controlled post-processing task that removes a support scar or seam ridge that catches a die at the ramp transition from a tabletop 3D printed dice tower with an open exit ramp and a visible lower landing area without changing the ramp slope, side-wall spacing, landing flatness and visible texture.
How can a printed dice-tower exit ramp be cleaned without making the roll path unpredictable? The example here is a tabletop 3D printed dice tower with an open exit ramp and a visible lower landing area. A rotary pen can offer local access after a print is cleaned and supported, but it is not a shortcut for uncertain geometry. The exact filament or resin, accessory instructions, fixture and representative sample govern any approved process.
What is the actual defect, and what must remain unchanged?
For clean 3D printed dice tower exit ramp, record a support scar or seam ridge that catches a die at the ramp transition before touching the part. On a tabletop 3D printed dice tower with an open exit ramp and a visible lower landing area, preserve the ramp slope, side-wall spacing, landing flatness and visible texture. Raking light, a close photo and a real mating item or gauge help separate an interference point from a cosmetic mark that should be left alone.
Establish the hand-finished reference first
a hard-backed abrasive used in the same direction as the intended roll path gives an operator immediate feedback at the defect. Make one small trial, clear residue and compare the result with an untouched area. That reference protects against turning an isolated problem on a tabletop 3D printed dice tower with an open exit ramp and a visible lower landing area into a larger dimensional or visual change.
When is a rotary pen useful in this application?
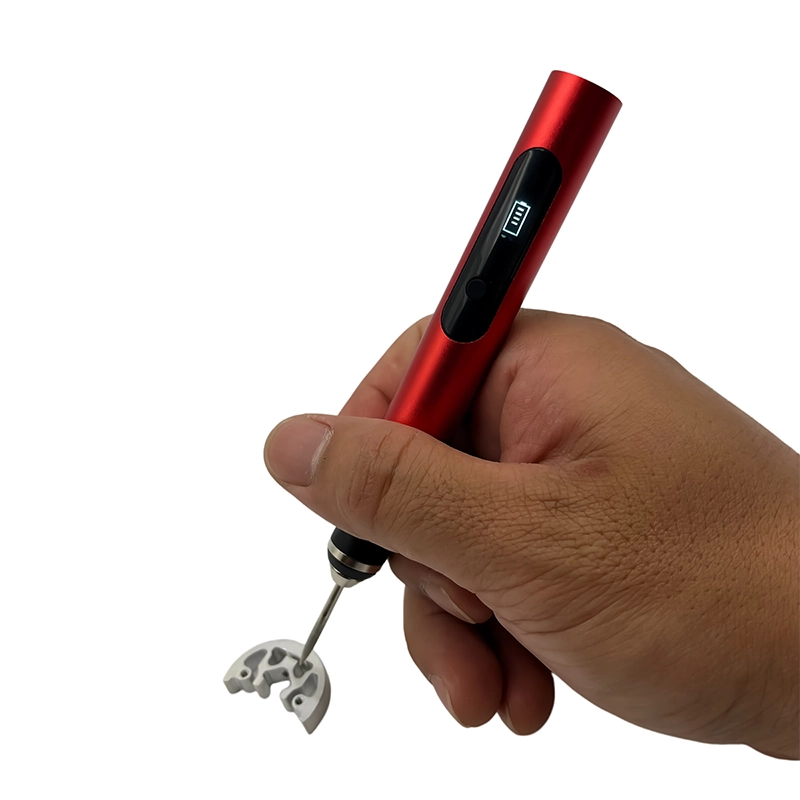
a small rotary abrasive used only for a local high spot away from ramp edges is appropriate only when the mapped contact is difficult to reach by hand. Use brief, inspectable contact rather than continuous abrasion, and do not treat a catalogued tool platform as a promised setting for every material or print profile. A rejected coupon is the safest place to learn the limit.
How should the printed part be held?
Use a broad padded base that holds the tower upright while leaving the lower ramp accessible. The fixture must resist vibration while keeping the contact zone visible, and it should not crush or preload delicate printed walls. Before rotating any accessory, confirm a clear tool path, a clear debris path and a safe stop path away from the operator and protected features.
Which first-article checks make the method repeatable?
For this use case, document ramp profile, die sample, local heat, surface texture and repeatable test rolls, along with material, print orientation, part revision, accessory identity, fixture and before-and-after images. The record should state the no-touch zones and name the gauge, sample or visual standard that decides whether this correction is accepted.
What is the practical pass sequence?
Inspect, mark, support, make one controlled contact, remove residue and inspect again. For clean 3D printed dice tower exit ramp, recheck the functional reference after every pass instead of waiting until the end. If the same high spot recurs across pieces, correct the print setup, orientation or model rather than normalizing open-ended manual rework.
What is the stop signal?
Stop work when a hollow forms, an edge rounds or the same die begins to deviate after the correction. Clean the part, compare it with the starting condition and choose the responsible next action: a gentler hand method, a changed fixture, a reprint or an upstream design and print correction. More pressure or speed cannot recover material that has already been removed.
How should this 3D printed part be released?
Release the part only when the approved die clears the local defect and rolls through the tower without a new snag or visible flat spot. Inspect under repeatable light and use the actual mating item or documented gauge where applicable. A surface can look cleaner while still failing its fit, alignment or visual-role requirement, so the acceptance step must be chosen before finishing begins.
What should an OEM buyer include in a rotary-pen brief?
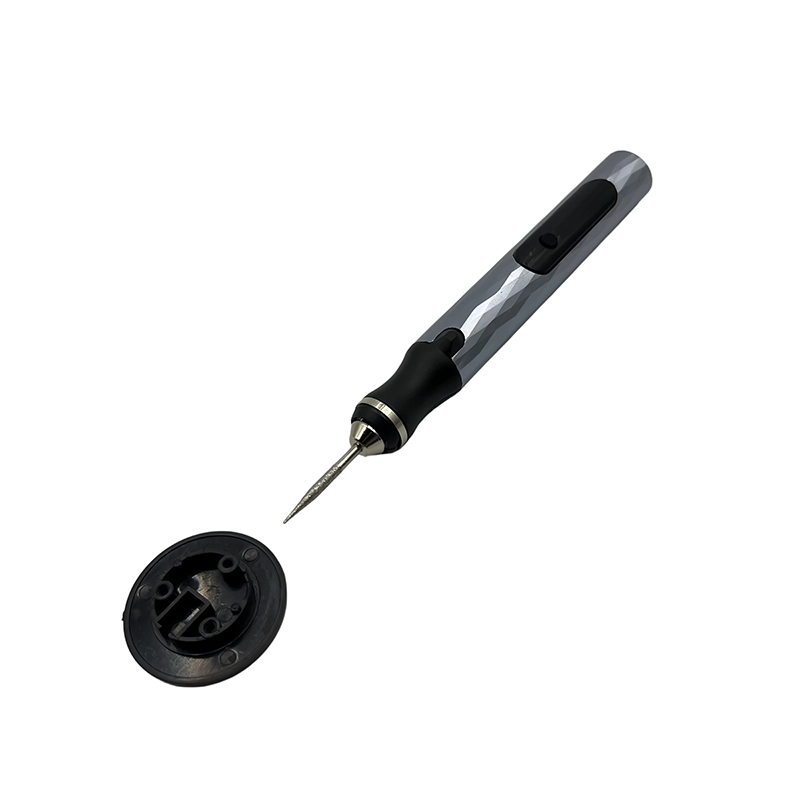
A buyer considering clean 3D printed dice tower exit ramp should provide the print material, defect photographs, protected features, fixture idea, accessory interface, target market, sample quantity and acceptance evidence. XOENAEN D-104 cordless engraving pen is a first-party XOENAEN catalogue reference, not a universal compatibility or performance claim. Evaluate the proposed configuration on the buyer's representative printed sample before release.
Use the least aggressive method that proves the result
| Method | Appropriate role | Control point |
|---|---|---|
| a hard-backed abrasive used in the same direction as the intended roll path | Identify and correct a local interference | Protect the marked boundary |
| a small rotary abrasive used only for a local high spot away from ramp edges | Reach a mapped inaccessible spot | a hollow forms, an edge rounds or the same die begins to deviate after the correction |
| Reprint or upstream correction | Recurring or geometry-critical artifact | Approve a new representative sample |
- Photograph a support scar or seam ridge that catches a die at the ramp transition before choosing an accessory.
- Protect the ramp slope, side-wall spacing, landing flatness and visible texture.
- Fixture the part with a broad padded base that holds the tower upright while leaving the lower ramp accessible.
- Record ramp profile, die sample, local heat, surface texture and repeatable test rolls.
- Stop if a hollow forms, an edge rounds or the same die begins to deviate after the correction.
- Approve only when the approved die clears the local defect and rolls through the tower without a new snag or visible flat spot.
- XOENAEN D-104 cordless engraving pen →
- 3D print finishing tools guide →
- Rotary tools and 3D print finishing hub →
- Related guide: refine 3d printed board game token trays →
- Related guide: smooth 3d printed tabletop miniature bases →
- Plan an OEM or ODM tool project →
- Continue with the clean-3d-printed-headphone-stand-cable-notches topic →
- XOENAEN editorial policy →
What should be checked before you clean 3D printed dice tower exit ramp?
Confirm that a support scar or seam ridge that catches a die at the ramp transition is the real interference, then protect the ramp slope, side-wall spacing, landing flatness and visible texture. Capture the starting condition and select the gauge or actual mating item before material is removed.
Why does workholding matter for clean 3D printed dice tower exit ramp?
a broad padded base that holds the tower upright while leaving the lower ramp accessible keeps the part stable and the contact point visible. That limits vibration and helps prevent accidental contact with the ramp slope, side-wall spacing, landing flatness and visible texture.
When can a rotary pen help with clean 3D printed dice tower exit ramp?
a small rotary abrasive used only for a local high spot away from ramp edges can help only after the contact zone is mapped and a hand reference is understood. Verify the material, accessory and geometry on a representative coupon first.
What tells an operator to stop clean 3D printed dice tower exit ramp?
Stop when a hollow forms, an edge rounds or the same die begins to deviate after the correction. Clean and inspect rather than increasing pressure or speed, because later polishing cannot replace removed geometry.
What should an OEM buyer supply for clean 3D printed dice tower exit ramp?
Provide the revision, material, defect photo, protected features, fixture constraints, sample quantity and acceptance evidence for clean 3D printed dice tower exit ramp. These inputs make the tool and accessory discussion specific to the real work.