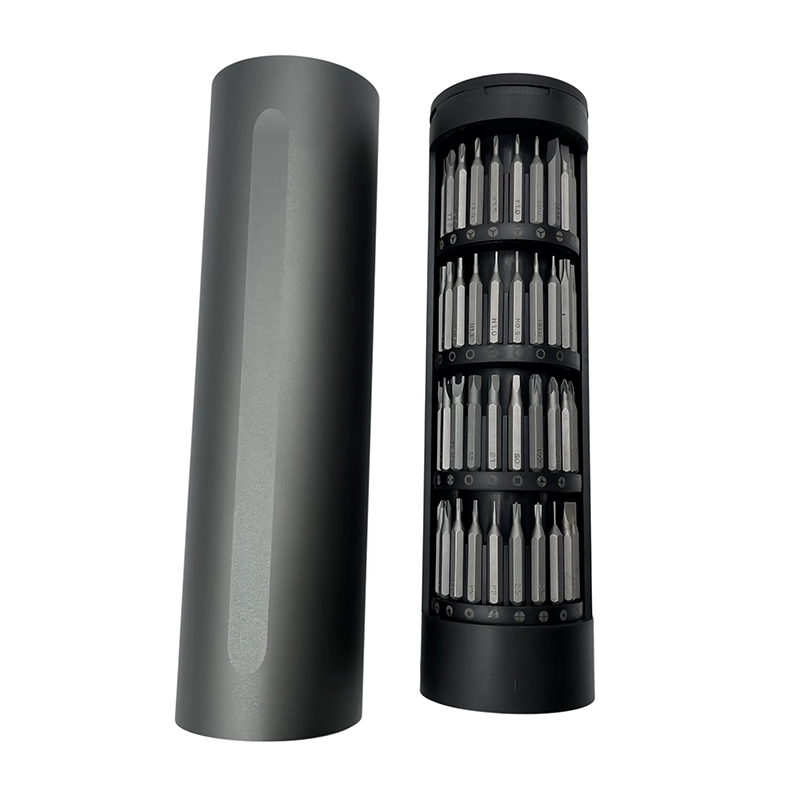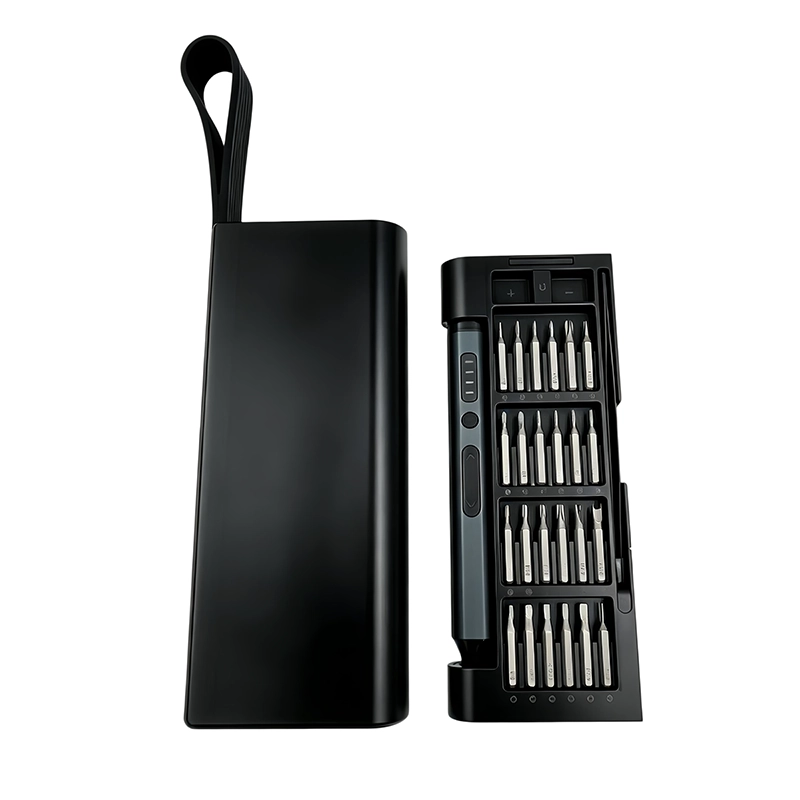
Verify electric screwdriver RPM with a documented mode, battery condition, bit or fixture, measurement instrument and sampling plan. Keep no-load and controlled-load results separate because they answer different questions. Record individual readings, instrument status and product revision, then compare them with limits approved for that exact motor, battery and control configuration rather than an unrelated nominal claim.
Production RPM verification
a traceable measurement of rotational speed under named no-load or controlled-load conditions for identified production samples and revisions.
The practical setting for production electric screwdriver RPM verification is a production team checks whether assembled drivers match an approved speed behavior before pack-out. This article treats the powered driver as one controlled element in a larger repair, assembly or approval system. The goal is not maximum trigger time. The goal is to preserve thread condition, device evidence and a repeatable handoff from preparation through final verification.
How should a factory define loaded and no-load RPM checks, sample size, instrument and acceptance limits?
How should a factory define loaded and no-load RPM checks, sample size, instrument and acceptance limits? For production electric screwdriver RPM verification, the useful answer begins with the service or assembly boundary, not with motor speed. Production RPM verification means a traceable measurement of rotational speed under named no-load or controlled-load conditions for identified production samples and revisions. The operator must distinguish verified fastener travel from diagnosis, prying, drilling, calibration and electrical work that belongs to a different procedure. This boundary keeps the powered driver in the part of the task where repetitive rotation is useful and observable.
A sound production electric screwdriver RPM verification decision also separates removal, free travel, thread engagement and final seating. Those phases do not carry the same risk. Removal may begin only after bit fit and support are proven. Free travel can often use controlled power. Thread engagement needs clear feedback, and final seating follows the product-specific instruction. Treating the entire joint as one trigger pull removes the inspection points that reveal a wrong screw, damaged thread or trapped component.
How should a bench be prepared for production electric screwdriver RPM verification?
Preparation for production electric screwdriver RPM verification starts with this action: Write the speed method, fixture and instrument fields Then Condition and identify the selected production samples Place the powered driver in a defined parking location and give removed hardware a separate, labeled area. A clean boundary prevents the tool, loose bit or customer screw from migrating into an exposed assembly. When batteries, boards, optics, seals or calibrated mechanisms are present, record exactly when the powered tool must leave the immediate work zone.
The fixture for production electric screwdriver RPM verification should support the structure close to the fastener without blocking visibility. Photograph original routing and screw locations before anything moves. Clean the recess with a method approved for the product, inspect the candidate bit and quarantine damaged hardware. These steps take less time than recovering a stripped recess or investigating a mystery screw after reassembly.
Why can production electric screwdriver RPM verification fail even when the bit appears to fit?
The central failure path in production electric screwdriver RPM verification is that mixing modes, charge states or load conditions can create misleading results and allow a changed motor or control to pass against the wrong reference. A tip can enter a recess and still be the wrong size, worn, too short or poorly aligned. Before powered travel, verify that the bit reaches its designed depth, does not rock and clears adjacent parts. Observe the screw from a second angle whenever the housing, fixture or operator's hand can hide side load.
For production electric screwdriver RPM verification, the four application controls are specific: separate no-load and controlled-load methods; define battery conditioning and operating mode; use an instrument with documented status and suitable fixture; and tie acceptance limits to the approved product revision. Each control blocks a different error path. No single claim about torque, runtime, steel grade or accessory count replaces them. If one control cannot be demonstrated on representative hardware, the task remains unapproved even when the driver runs normally on an unloaded bench.
What operating sequence works for production electric screwdriver RPM verification?
The controlled sequence for production electric screwdriver RPM verification is staged. First, Write the speed method, fixture and instrument fields Second, Condition and identify the selected production samples Third, Measure no-load speed only under its named method The first powered movement should be brief enough to stop while the original condition is still visible. Keep the driver aligned with the screw axis, avoid using the bit as a lever and release the control before repositioning the work.
Continue production electric screwdriver RPM verification by following these closing steps: Run any controlled-load check as a separate dataset Finally, Review results against revision-specific limits and retain traceability Account for every bit, screw, spacer and temporary fixture before power or function is restored. If the receiving thread does not accept the screw naturally, back out and investigate. Repeated trigger pulses are not a substitute for identifying contamination, wrong pitch, cross-threading or a shifted joint stack.
What stop rule protects production electric screwdriver RPM verification?
The explicit stop signal for production electric screwdriver RPM verification is: instrument status is uncertain, battery conditioning varies, the fixture slips or product revision cannot be confirmed. At that point, release the trigger, keep the original condition visible and decide whether the bit, screw, thread, fixture or procedure needs correction. Do not add downward force or speed simply because the expected movement did not occur. A stop rule is useful only when every operator can recognize it before damage becomes the new condition.
Acceptance for production electric screwdriver RPM verification is equally concrete: identified samples meet the separate approved speed limits under the documented no-load and controlled-load methods Check the surrounding assembly, not only the screw head. Enclosures should settle without forced gaps, moving parts should retain clearance, cables and seals should remain in their documented positions, and any required functional or calibration check should follow the accountable maker's procedure. Record exceptions rather than hiding them under final assembly.
Which two approaches should be compared for production electric screwdriver RPM verification?
For production electric screwdriver RPM verification, No-load RPM check is best understood this way: screens basic motor and control behavior without joint load. By comparison, Controlled-load RPM check is best understood this way: adds defined resistance and evaluates a different operating condition. Neither label is automatically safer or faster. Choose from access, screw condition, receiving material, cycle count, operator visibility and the cost of a mistake. Record why the selected approach fits this exact application instead of copying a setting from an unrelated device.
State the test condition every time RPM is reported, because an isolated number without load, mode and battery context is not comparable evidence. That recommendation for production electric screwdriver RPM verification turns a broad tool feature into a documented decision. During sample review, evaluate the installed bit, actual hardware, workholding and operator sequence together. A free-spinning demonstration can show that the motor works, but it cannot prove control at a shallow recess, plastic boss, threaded insert, gasketed joint or crowded electronic assembly.
How should production electric screwdriver RPM verification influence maintenance and training?
Training for production electric screwdriver RPM verification should show the real fixture, screw groups, parking location, hand-to-power transition and stop signal. “Use carefully” is not an instruction. A repeatable instruction names the profile, working length, support point, rotation phase and condition that requires escalation. Supervisors can then observe the process and separate a tool problem from a mapping, material, training or product-design problem.
Maintenance records for production electric screwdriver RPM verification should distinguish worn bits, holder contamination, control faults, charging issues, abnormal sound, dropped tools and application damage. Trend the categories rather than combining them as “driver problems.” A recurring pattern may call for a replacement interval, clearer label, different accessory, revised fixture or supplier corrective action. Evidence from the workbench is more valuable than adding unverified claims to the package.
What should a buyer specify for production electric screwdriver RPM verification?
For production electric screwdriver RPM verification, specify instrument, fixture, mode, battery conditioning, sample plan, loaded and no-load datasets, limits and change-control trigger. The RFQ should name target devices or joints, screw profiles and sizes, working lengths, expected daily cycles, charging pack-out, case layout, manual languages and sample quantity. Compatibility claims need a model list and an approval method. Numerical claims need the test condition, sample count, acceptance limit and record owner.
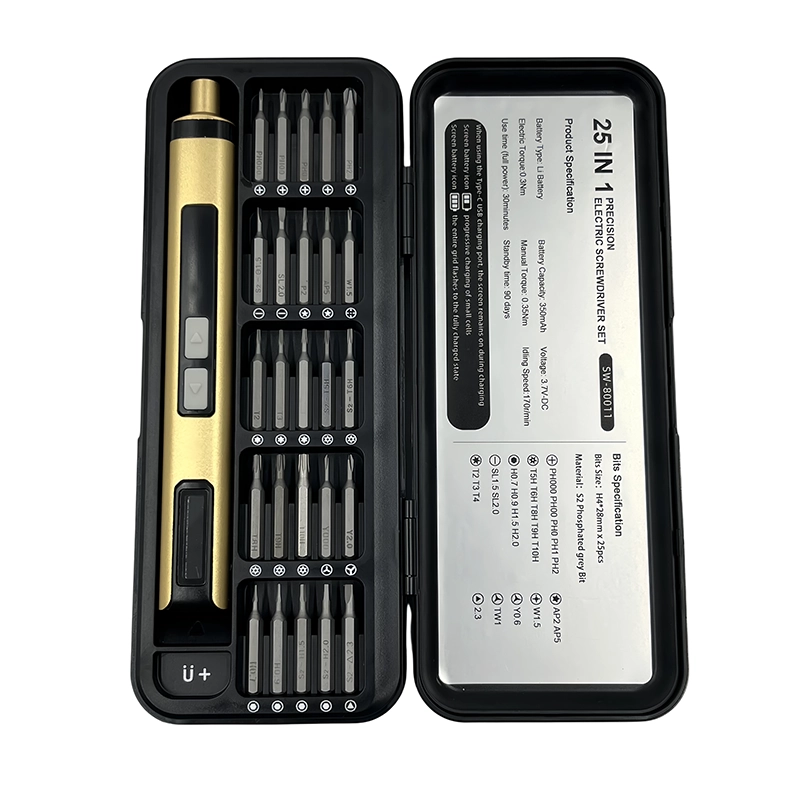
The sample plan for production electric screwdriver RPM verification should inspect appearance, controls, bit fit, installed-bit behavior, charging, indicator states, case organization, labels, instructions and representative screw work. Retain the approved sample and its bit map. If the motor, battery, control board, cable, bit source, case insert or instruction changes, assess the effect before the revised item enters production or replaces field stock.
What evidence supports guidance for production electric screwdriver RPM verification?
This production electric screwdriver RPM verification guide uses the stated customer question, a task-level failure analysis, the linked official guidance and the current XOENAEN catalogue record for the selected product platform. It does not infer universal device compatibility, certification, a customer result or a torque value that is absent from the model record. Representative hardware and the accountable product procedure remain the basis for approval.
The methodology for production electric screwdriver RPM verification connects each recommendation to an observable condition: bit engagement, alignment, receiving material, workholding, powered response, stop signal and post-work acceptance. Keep photographs, sample identifiers, revisions and deviations with the decision. This creates an answer that another technician or buyer can audit instead of relying on a generic “best tool” statement that changes meaning from one joint to another.
No-load RPM check compared with Controlled-load RPM check for production electric screwdriver RPM verification
| Approach | Best use | Primary control |
|---|---|---|
| No-load RPM check | screens basic motor and control behavior without joint load | separate no-load and controlled-load methods |
| Controlled-load RPM check | adds defined resistance and evaluates a different operating condition | define battery conditioning and operating mode |
- Define the customer question for production electric screwdriver RPM verification: How should a factory define loaded and no-load RPM checks, sample size, instrument and acceptance limits?
- Document the real application boundary: a production team checks whether assembled drivers match an approved speed behavior before pack-out
- Verify the first powered control: separate no-load and controlled-load methods
- Verify the second powered control: define battery conditioning and operating mode
- Approve representative hardware against XOENAEN 25-in-1 electric precision screwdriver set
- Retain the bit map, charging pack-out, stop rule and revision owner for production electric screwdriver RPM verification
- XOENAEN 25-in-1 electric precision screwdriver set →
- Choose a precision electric screwdriver →
- Electric screwdriver torque guide →
- XOENAEN OEM and ODM process →
- Manufacturing and quality control →
- Read the related electric-screwdriver-torque-repeatability-study guide →
- Read the related electronic-torque-control-vs-mechanical-clutch guide →
- How XOENAEN presents quality evidence →
Should electric screwdriver RPM be checked loaded and unloaded?
Before production electric screwdriver RPM verification, confirm the exact product boundary, fastener map and this first control: separate no-load and controlled-load methods. A physically fitting bit alone does not authorize the work.
What tachometer traceability is required for production RPM checks?
The specific powered-rotation concern during production electric screwdriver RPM verification is that mixing modes, charge states or load conditions can create misleading results and allow a changed motor or control to pass against the wrong reference. Short runs and deliberate inspection points preserve time to detect that change.
How are speed limits tied to the approved motor and battery?
Release the trigger during production electric screwdriver RPM verification as soon as instrument status is uncertain, battery conditioning varies, the fixture slips or product revision cannot be confirmed. Do not compensate with more speed, pressure or repeated cycling.
Can a no-load RPM result prove fastening performance?
For production electric screwdriver RPM verification, No-load RPM check screens basic motor and control behavior without joint load, while Controlled-load RPM check adds defined resistance and evaluates a different operating condition. Select the method from the joint condition and consequence of error.
Which sample records should a buyer retain for production electric screwdriver RPM verification?
A buyer approving production electric screwdriver RPM verification should document specify instrument, fixture, mode, battery conditioning, sample plan, loaded and no-load datasets, limits and change-control trigger. The approved sample, bit map and revision record should remain linked to the purchase specification.
Which observable result closes the work on production electric screwdriver RPM verification?
Completion of production electric screwdriver RPM verification requires this observable result: identified samples meet the separate approved speed limits under the documented no-load and controlled-load methods Installed screws alone are not evidence that the surrounding product is correctly restored.