For finish 3D printed LED diffuser edges, first identify a support mark or seam ridge on an edge that enters a retaining channel and protect edge thickness, light-blocking overlap, visible face and locating tabs. Start with a flat-backed micro abrasive used only on the marked edge; use a clean fine rotary pad used for a small local ridge after a coupon check only when access requires it. Control material clarity, heat, edge squareness, abrasive cleanliness and light-path inspection. Stop when the edge turns cloudy, a tab rounds or light becomes visible outside the intended aperture. Release the part only when the diffuser seats evenly, its visible face remains consistent and the assembled light pattern meets the approved comparison.
finish 3D printed LED diffuser edges
finish 3D printed LED diffuser edges is a controlled post-processing workflow that removes a support mark or seam ridge on an edge that enters a retaining channel from a printed translucent diffuser insert for a small enclosure, sign or prototype indicator while preserving edge thickness, light-blocking overlap, visible face and locating tabs.
How should an LED diffuser edge be cleaned without changing its fit or creating visible light leaks? This guide uses a printed translucent diffuser insert for a small enclosure, sign or prototype indicator as a practical post-processing case. It does not assume that a rotary pen is the first answer for every polymer or geometry: the material supplier, approved accessory limit, workholding and representative sample control the final process.
What should be mapped before material is removed?
Start by photographing the condition and identifying a support mark or seam ridge on an edge that enters a retaining channel. Mark the smallest area that actually interferes with the next operation. On a printed translucent diffuser insert for a small enclosure, sign or prototype indicator, the protected features are edge thickness, light-blocking overlap, visible face and locating tabs. A smoother looking part can still be a reject when its fit, load path or visible geometry has changed.
Which finishing method should be the reference?
a flat-backed micro abrasive used only on the marked edge is the reference method because it gives immediate tactile feedback. Make a short trial on an equivalent defect, clean the area and compare it with an untouched reference. The aim is to confirm the contact map before a powered accessory repeats the correction more quickly.
When does a rotary pen add practical value?
a clean fine rotary pad used for a small local ridge after a coupon check can be useful when the defect is inside a recess or an awkward corner. It is a local-access method, not a substitute for controlled machining or a reason to abrade an entire feature. Use a representative coupon first and keep the accessory moving through short, inspectable contacts.
How should the workpiece be supported?
Use a clean padded edge fixture that holds the diffuser without touching the visible face. This limits vibration and keeps the operator able to see the contact zone. Check that the part cannot rotate into the accessory, that dust does not hide the defect and that the fixture does not preload thin printed features. Recheck the setup after every material or part-revision change.
Which variables should be recorded on the first article?
Record material clarity, heat, edge squareness, abrasive cleanliness and light-path inspection, together with print material, orientation, part revision, accessory identity, fixture and start/end photographs. A written record should tell the next operator where contact is allowed, which area is no-touch and which gauge or mating item proves the correction has not changed the design.
What is the controlled pass sequence?
For finish 3D printed LED diffuser edges, inspect, mark, support, make one light pass, stop, remove debris and inspect again. Repeat only if the marked defect remains. If the same artifact appears across multiple prints, investigate the print process, part orientation or design rather than converting unlimited hand rework into the normal production method.
Which sign means the operation must stop?
Stop immediately when the edge turns cloudy, a tab rounds or light becomes visible outside the intended aperture. Do not compensate with higher speed or pressure. Clean the part and compare it with the starting image, then decide whether a different hand method, a new fixture, a reprint or an upstream correction is the responsible next step.
How should the result be accepted?
The release condition is that the diffuser seats evenly, its visible face remains consistent and the assembled light pattern meets the approved comparison. Inspect under repeatable light and, where function matters, use the actual mating component or a documented gauge. Cosmetic improvement alone is not proof that a printed functional feature still works as designed.
What should a buyer specify in a finishing-tool brief?
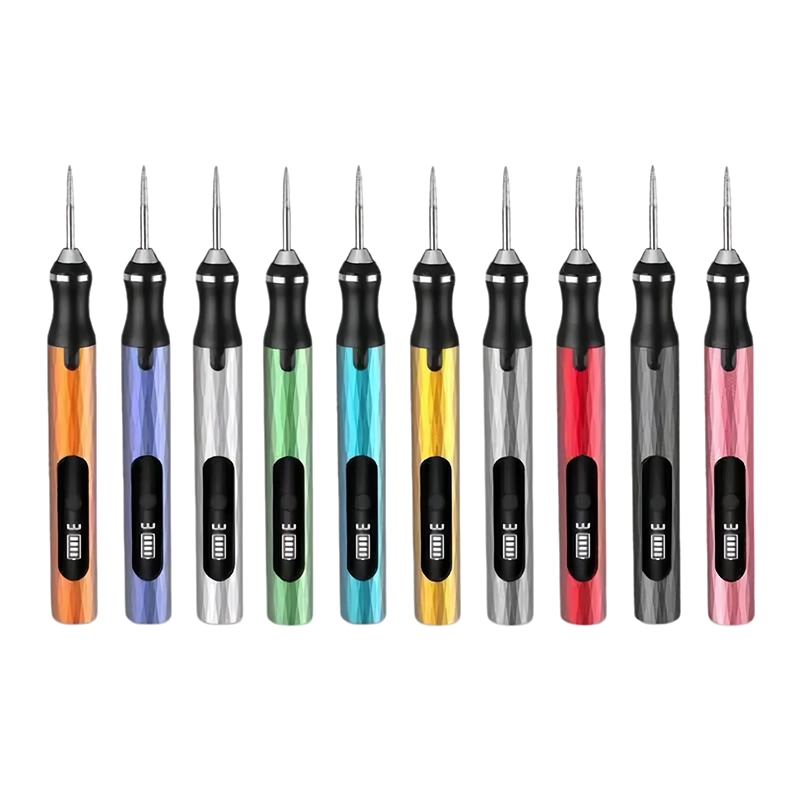
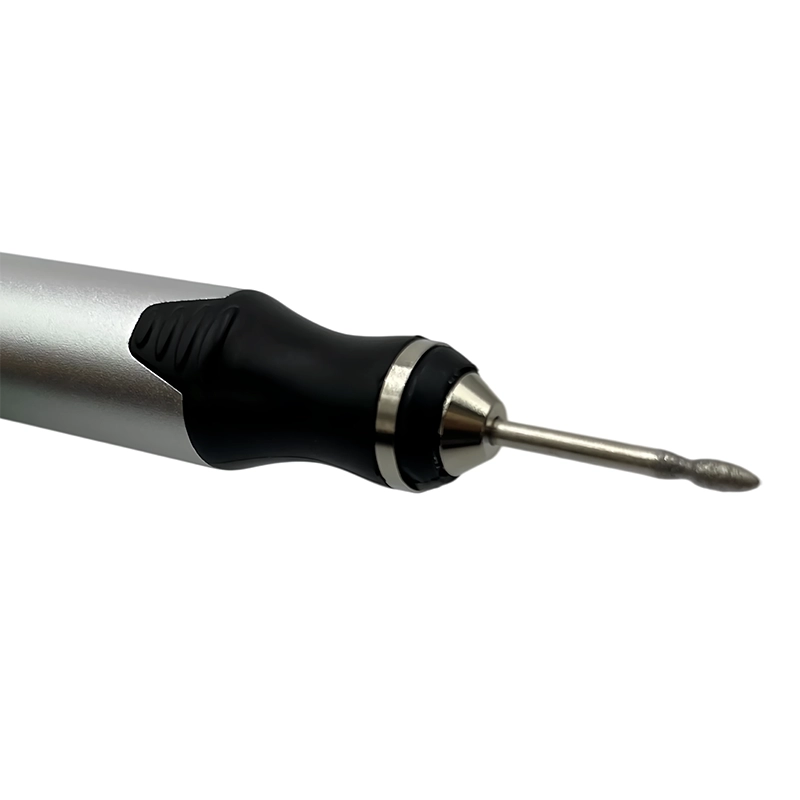
For finish 3D printed LED diffuser edges, specify the printed material, real defect, protected dimensions, fixture, accessory interface, desired pack-out, target market, sample quantity and acceptance check. The XOENAEN H101 five-speed cordless engraving pen is a first-party XOENAEN catalogue reference; it does not establish a universal setting or outcome for every printed part. Qualify the proposed configuration on the buyer's own representative sample before making customer-facing claims.
Choose the least aggressive controlled method
| Method | Best use | Risk to manage |
|---|---|---|
| a flat-backed micro abrasive used only on the marked edge | Map the defect and establish a tactile reference | Slow access or unintended edge contact |
| a clean fine rotary pad used for a small local ridge after a coupon check | Reach a mapped local obstruction | the edge turns cloudy, a tab rounds or light becomes visible outside the intended aperture |
| Reprint or upstream correction | A defect repeats or critical geometry is affected | Requires a documented new sample |
- Map a support mark or seam ridge on an edge that enters a retaining channel before choosing an accessory.
- Protect edge thickness, light-blocking overlap, visible face and locating tabs.
- Support with a clean padded edge fixture that holds the diffuser without touching the visible face.
- Control material clarity, heat, edge squareness, abrasive cleanliness and light-path inspection.
- Stop when the edge turns cloudy, a tab rounds or light becomes visible outside the intended aperture.
- Approve only when the diffuser seats evenly, its visible face remains consistent and the assembled light pattern meets the approved comparison.
- XOENAEN H101 five-speed cordless engraving pen →
- 3D print finishing tools guide →
- Rotary tools and 3D print finishing hub →
- Related guide: polish clear fdm prints without clouding →
- Related guide: polish clear resin light pipe printed surface →
- Plan an OEM or ODM tool project →
- Continue with the finish-3d-printed-paint-rack-hook-slots topic →
- XOENAEN editorial policy →
What should be checked before you finish 3D printed LED diffuser edges?
Confirm a support mark or seam ridge on an edge that enters a retaining channel is outside the approved geometry, then protect edge thickness, light-blocking overlap, visible face and locating tabs. Photograph the starting condition and choose the inspection or mating reference before any material is removed.
Why is workholding important for finish 3D printed LED diffuser edges?
Use a clean padded edge fixture that holds the diffuser without touching the visible face. Stable support limits vibration and helps prevent unplanned contact with edge thickness, light-blocking overlap, visible face and locating tabs. It also makes the first-article method reproducible.
When should a rotary pen be used for finish 3D printed LED diffuser edges?
a clean fine rotary pad used for a small local ridge after a coupon check is useful only after the contact is mapped and a hand reference is understood. Test the material, accessory and part geometry on a representative coupon before approving it for repeated work.
What is the stop signal for finish 3D printed LED diffuser edges?
Stop when the edge turns cloudy, a tab rounds or light becomes visible outside the intended aperture. Clean and inspect instead of increasing speed or pressure; removed geometry cannot be restored by later polishing.
What should an OEM buyer provide for finish 3D printed LED diffuser edges?
For finish 3D printed LED diffuser edges, provide the part revision, material, defect photo, protected features, acceptance gauge or mating part, target market, pack-out and required sample evidence. This allows the tool and accessory proposal to be evaluated against the real work.