For finish 3D printed table lamp shade seam, map a vertical seam ridge on a visible outer face before removing material and protect wall thickness, diffuser contour, join geometry and heat-clearance features. Start with a flexible abrasive strip supported by a shaped block; use a clean fine rotary pad for a short local transition away from the rim only for mapped local access. Support the part, inspect after each short pass and stop when the wall turns thin, a bright spot appears under light or the rim loses roundness. Approve it only when the shade sits true and the seam is no longer visually dominant when illuminated.
finish 3D printed table lamp shade seam
finish 3D printed table lamp shade seam is a controlled local finishing process for a printed table-lamp shade or decorative lighting cover that addresses a vertical seam ridge on a visible outer face while protecting wall thickness, diffuser contour, join geometry and heat-clearance features.
a printed table-lamp shade or decorative lighting cover can need post-processing, but a rotary pen is not the first answer for every material or geometry. The practical issue is a vertical seam ridge on a visible outer face; the features that must remain unchanged are wall thickness, diffuser contour, join geometry and heat-clearance features. Treat the work as local correction, not general polishing.
What should be checked before the first pass?
Photograph the condition, identify the part revision and mark the smallest area that interferes with fit or appearance. Compare the marked area with an untouched reference. A surface can look smoother while becoming unusable if wall thickness, diffuser contour, join geometry and heat-clearance features changes. Confirm the material supplier's guidance and use a representative sample when the material, print orientation or accessory changes.
When is a rotary pen useful after 3D printing?
a flexible abrasive strip supported by a shaped block provides the reference because the operator can feel the contact. a clean fine rotary pad for a short local transition away from the rim is useful only when the defect is inaccessible by hand and the permitted contact area is clear. Use light, brief contact; remove debris; inspect; then decide whether another pass is necessary. Do not use speed or pressure to compensate for a poorly supported part.
How should the printed part be supported?
Use a padded cylindrical mandrel that supports the shade from inside. The fixture should prevent vibration without loading thin printed features. Keep the actual contact zone visible, control loose particles and check that the part cannot rotate into the accessory. If the same defect recurs, investigate print settings, orientation or design instead of normalizing additional rework.
What makes the correction acceptable?
Stop when the wall turns thin, a bright spot appears under light or the rim loses roundness. The release check is that the shade sits true and the seam is no longer visually dominant when illuminated. Inspect under repeatable light and use the actual mating part or documented gauge when function matters. Record the material, part revision, fixture, accessory and before/after photographs for the first article so the method can be reviewed rather than copied as an assumed universal setting.
What should a buyer include in a tool brief?
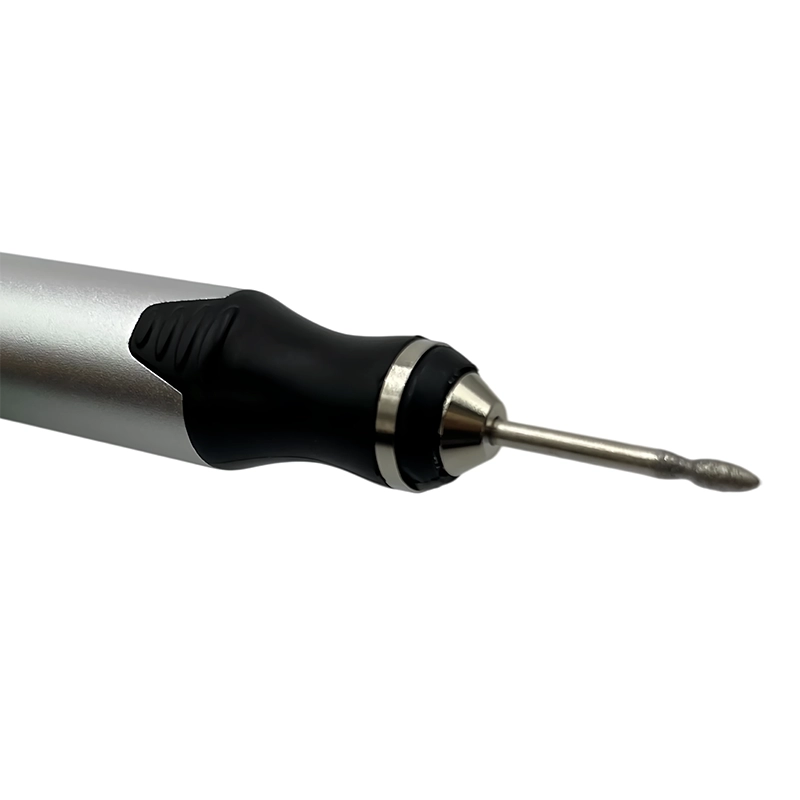
Provide the printed material, part revision, defect photo, protected features, expected throughput, fixture constraint, target pack-out and acceptance check. XOENAEN D-102 cordless engraving pen is a current XOENAEN product reference, not a claim that one configuration suits every polymer or geometry. Qualification must use the buyer's representative part and their approved process.
Choose the least aggressive controlled method
| Method | Use it when | Control point |
|---|---|---|
| a flexible abrasive strip supported by a shaped block | The defect is accessible and a tactile reference is needed | wall thickness, diffuser contour, join geometry and heat-clearance features |
| a clean fine rotary pad for a short local transition away from the rim | A mapped obstruction needs local access | the wall turns thin, a bright spot appears under light or the rim loses roundness |
| Reprint or upstream correction | The defect is repeated or a critical feature is affected | Approve a new sample |
- Map a vertical seam ridge on a visible outer face.
- Protect wall thickness, diffuser contour, join geometry and heat-clearance features.
- Use a padded cylindrical mandrel that supports the shade from inside.
- Inspect after every short pass.
- Release only when the shade sits true and the seam is no longer visually dominant when illuminated.
- XOENAEN D-102 cordless engraving pen →
- 3D print finishing tools guide →
- Rotary tools for 3D print finishing →
- Related guide: finish 3d printed led diffuser edges →
- Related guide: polish clear resin light pipe printed surface →
- OEM and ODM capabilities →
- Continue with the prep-3d-printed-casting-pattern-gate-edges topic →
- XOENAEN editorial policy →
Should a rotary pen be the first choice for finish 3D printed table lamp shade seam?
No. Start with a flexible abrasive strip supported by a shaped block; use powered local access only after the contact area and protected features are mapped.
What is the key release check?
the shade sits true and the seam is no longer visually dominant when illuminated